
- Posts: 9
- Thank you received: 1

Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
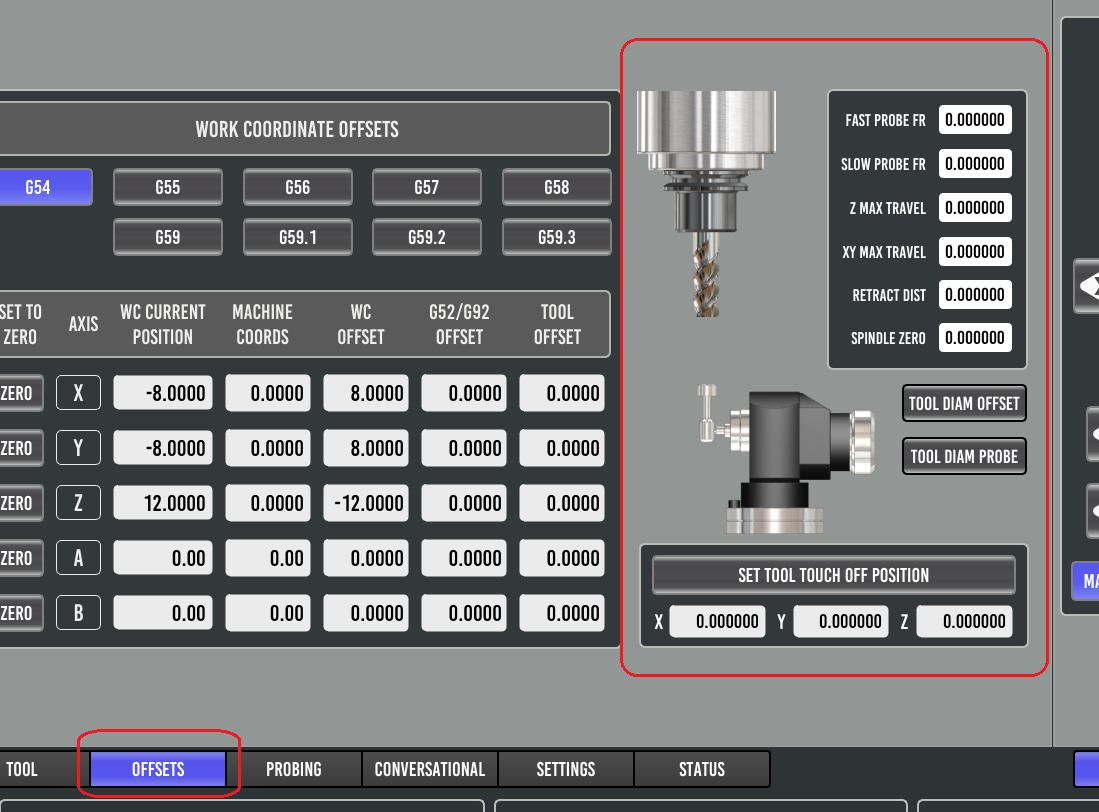
those parameters are set from the offsets page in probe basic.Hi,
I would like to call tool_touch_off.ngc subroutine from my remapped M6 subroutine, but I am missing parameters:
#<fast_probe_fr> = #1 (set from probe screen fast probe feed rate)
#<slow_probe_fr> = #2 (set from probe screen slow probe feedrate)
#<z_max_travel> = #3 (max z distance the tool travels before erroring out if not contact is made)
#<xy_max_travel> = #4 (max xy distance the tool travels before erroring out if not contact is made)
#<retract_distance> = #6 (distance the tool retracts after making contact during fast feed mode)
#<spindle_zero_height> = #5 (G53 distance from home to spindle nose triggering point on touch plate)
#<tool_diameter_probe_mode> = #8 (activates the tool diameter probe subroutine section)
#<tool_diameter_offset_mode> = #9 (activates the tool diameter offset position for probe subroutine section)
#<tool_diameter> = #10 (current tool's diameter used for offseting probe position in x axis)
Where those parameters are stored? Is there any chance I could access them from subroutine and and use them when I call tool_touch_off.ngc?
Best regards,
Guntars
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
I have done it like this,
Code:#<fast_probe_fr> = 50 (1: set from probe screen fast probe feed rate) #<slow_probe_fr> = 10 (2: set from probe screen slow probe feedrate) #<z_max_travel> = 28 (3: max z distance the tool travels before erroring out if not contact is made) #<xy_max_travel> = 0 (4: max xy distance the tool travels before erroring out if not contact is made) #<spindle_zero_height> = 87.1121 (5: G53 distance from home to spindle nose triggering point on touch plate) #<retract_distance> = 0.5 (6: distance the tool retracts after making contact during fast feed mode) #7= 0 (7: n/a) #<tool_diameter_probe_mode> = 0 (8: activates the tool diameter probe subroutine section) #<tool_diameter_offset_mode> = 0 (9: activates the tool diameter offset position for probe subroutine section) #<tool_diameter> = 0 (10: current tool's diameter used for offseting probe position in x axis) o<tool_touch_off> call [#<fast_probe_fr>] [#<slow_probe_fr>] [#<z_max_travel>] [#<xy_max_travel>] [#<spindle_zero_height>] [#<retract_distance>] [#<go_back_to_start_pos>] [#<tool_diameter_probe_mode>] [#<tool_diameter_offset_mode>] [#<tool_diameter>]
Please Log in or Create an account to join the conversation.
[/quote]those parameters are set from the offsets page in probe basic.
Please Log in or Create an account to join the conversation.

