Sherline Lathe Conversion ?

More
10 years 9 months ago #68816 by currinh
Replied by currinh on topic Sherline Lathe Conversion ?

andypugh wrote: I have wondered if a speedometer drive would work:
www.beedspeed.com/images/Speedo_drive_kit_metal.gif
The problem would be to find one that was exactly 1:1, but the dissimilar sizes of driver and driven might be useful.


Hmm. For a spindle, the P/R of standard encoders seems in the ball park. How would slowing, or speeding, the sensor shaft help? I always think of gears as introducing backlash, but for a spindle only rotating one direction it wouldn't matter. One could put a hall effect or optical sensor directly on the spindle for a Z pulse. You'd want a constant pulse stream so consider this when picking a gear ratio. As an extreme example consider a speed ratio of 1.111 (20:18 gears) and a 4 P/R encoder. This gives 4.444 P/R at the spindle which gives one uneven pulse using a Z on the spindle. A 1.25 radio (20:16) would give 5 P/R for an even pulse spacing. I don't know enough about LinucCNC to know if this is a potential problem or not.

Thanks.

Hugh

Please Log in or Create an account to join the conversation.
More
10 years 9 months ago #68817 by andypugh

currinh wrote: Hmm. For a spindle, the P/R of standard encoders seems in the ball park. How would slowing, or speeding, the sensor shaft help?


It would rarely help. Running at half-speed would be OK, as the index would still happen at a consistent angle, you might just have to wait longer for one. Anything non-integer would require a separate index from a sensor on the spindle.

This gives 4.444 P/R at the spindle which gives one uneven pulse using a Z on the spindle. A 1.25 radio (20:16) would give 5 P/R for an even pulse spacing. I don't know enough about LinucCNC to know if this is a potential problem or not


In practice it wouldn't matter except, possibly for gear hobbing.
For threading the encoder is zeroed at the start of each pass. The calculations are done in double-precision floating-point, with at least 15 digits of precision. For any plausible length of thread you would not see the rounding errors. But the HA/INI file should probably have at least 8 digits for non-integer scales.

Please Log in or Create an account to join the conversation.
More
10 years 9 months ago - 9 years 4 months ago #69008 by currinh
Replied by currinh on topic Sherline Lathe Conversion ?
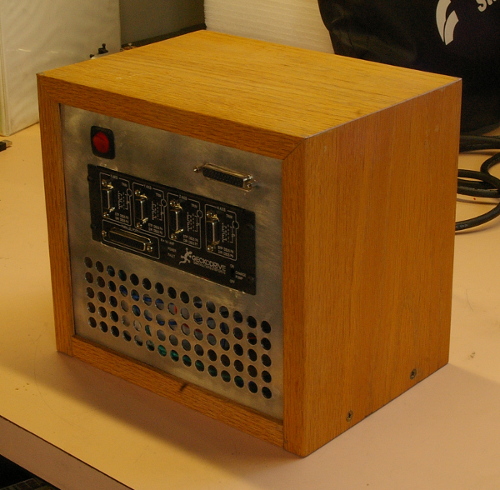
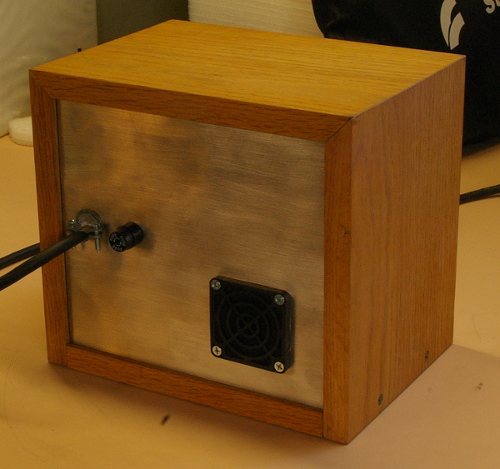
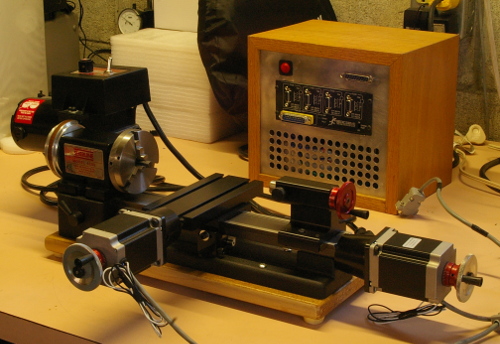
I've made some progress on the Sherline Lathe. I put together a driver box for the electronics. It has a toroidal transformer, 50V rectifier module, Gecko G540, 5v power supply, 60mm fan, switch and fuse holder. An old wooden stereo box had been sitting around for 15-20 years thatI re-purposed it for the driver box.


The separate DB25 plug at the upper right brings out the G540 terminal block and 5v supply.

The Lathe is so far a plain vanilla Sherline CNC conversion.


I'll likely build a stand and then decide how far I have to extend the stepper leads. Also decide lengths for the encoder and limit switch leads.

I ordered some slotted optical switches before ordering the encoder. These arrived from Newark a day or two ago. I hooked up the LED side to the 5V supply with a 250 ohm resistor (20mA). Then connected the open collector output directly to one of the G540 inputs and its ground. Using HALmeter I was able to monitor the parallel port line and see that it was switching. There was joy. Sounds simple, but with dumb wiring errors and other trial & error it took me some time.

I'm sure I'll have LinuxCNC questions once the encoder is mounted. I'm also starting to believe running a CNC lathe isn't trivial either, so I'll likely have some questions there also.

Thanks.

Hugh
Klamath Falls, OR, USA
Last edit: 9 years 4 months ago by currinh. Reason: Fixed pictures, which weren't displaying.

Please Log in or Create an account to join the conversation.
More
10 years 9 months ago #69010 by BigJohnT
Very nice work!

JT

Please Log in or Create an account to join the conversation.
More
10 years 8 months ago #69816 by currinh
Replied by currinh on topic Sherline Lathe Conversion ?
Thanks JT. It did come out looking good.

I've made some progress, mostly in learning how to run a CNC lathe. Seems a different ball game than a mill. It's only two axes, instead of three, so how could it be difficult? I set off learning the new turning portion of CamBam. It's not nearly as polished as the milling portion but eventually seemed workable. I couldn't get the roughing lead in moves to work, but that's a topic for the CamBam Forum. CamBam came with a LinuxCNC-turn post processor which I used without modification.

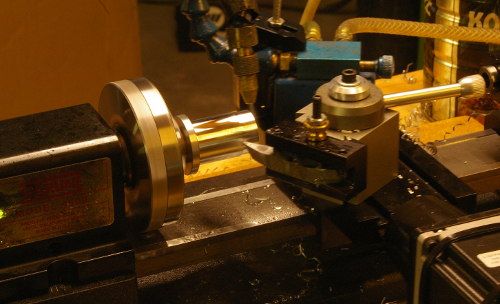
I had some learning difficulties, such as grabbing a scrap round of AL 1.5" diam saying that'll be large enough. The CAM was developed assuming a 1.25" stock. It didn't take too long to remember I had to cut the stock to 1.25". Then I had to come to grips with the Sherline. I have a 14" Goodway manual lathe and it took some experimenting to discover just how much less the Sherline can take off. After that it worked well. Here's a shot of the lathe during first cut.

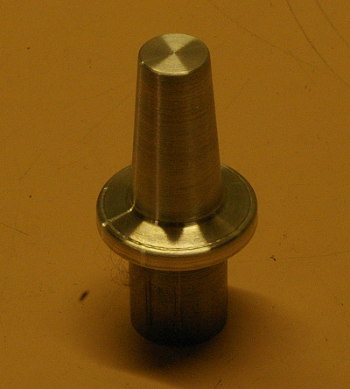
The resulting part is one post of a towel rack for our trailer. There's a bobble around the flange, but I'm declaring it a good part.

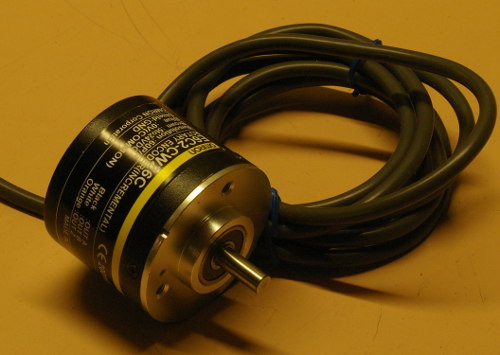
The slow boat from China did show up on our shores delivering a new encoder.

It is the same one mentioned above. It'll take some time to design and build the mounting, too many things getting in the way. But that is the plan. Then wire in the Sherline spindle speed control and maybe homing switches, although I may be OK without the switches. One step at a time.


I need to write this up if it isn't a know issue. I loaded LinuxCNC in simulation mode trying to track down some CamBam/G-Code questions. It seemed that LinuxCNC was rounding corners during rapid moves. I didn't notice it while machining but it was disconcerting to notice in simulation. The arcs are much bigger than a tool compensation would account for and the G Code had only sharp corners. If this seems unusual let me know and I'll start a thread on it.

Thanks.

Hugh
Klamath Falls, OR, USA

Please Log in or Create an account to join the conversation.
More
10 years 8 months ago #69828 by andypugh
For your next trick, convert the Goodway to CNC :-)

currinh wrote: I need to write this up if it isn't a know issue. I loaded LinuxCNC in simulation mode trying to track down some CamBam/G-Code questions. It seemed that LinuxCNC was rounding corners during rapid moves


It does that. The degree to which it does it is partly governed by the acceleration settings of the machine, and perhaps those are low in the simulator config you were looking at. I think that the G64 (etc) settings can also have a bearing on this, even in rapid moves.

Please Log in or Create an account to join the conversation.
Time to create page: 1.550 seconds
Powered by Kunena Forum
