Help Controller for a Lathe ?

More
3 months 4 days ago #348139 by MikkelRS
I converted a manual KBC GRIP-1340 lathe to CNC, kept the handwheels connected via encoders. I can manually machine or NC with it, It is more like a 'teaching' lathe, or tool room cnc lathe. Gives you the ability to quickly face or turn a diameter without having to write code or install a gui/cam thing to do it for you.

When i spin the handwheels, then stop, the machine stops. Encoder over-run is something you can disable. Sure you dont get feedback like a manual crank, but for the odd time doing something it doesnt matter. I put microswitches in the feed sticks and spindle fwd/rev lever, right now im using on screen dials to set the pitches and speeds, but its very similar to a manual lathe when you want it to be, and exactly a CNC lathe when it has to be.

I ended up using a 7i76E and 360ppr encoders connected with a small timing belt to 3d printed gears secured to the hand wheels inside an apron box i made from some rectangle tubing. My X ballscrew isnt in the apron it is beside the cross slide. I still have the cross slide on the lathe incase a quick taper job is required. Ill probably end up ditching it eventually for a more solid mount as its a weak point.

Anyways, the machine has made its money back and then a small fountain of cash to fund the other toys. It might not be everyones cup of tea, but it works very well.
 

Please Log in or Create an account to join the conversation.

More
3 months 3 days ago - 3 months 3 days ago #348159 by timo
Replied by timo on topic Help Controller for a Lathe ?
@tuxcnc: Are you a nay sayer? image missing /media/kunena/emoticons/cool.png 

Being pointed to weak aspects of something is not a bad thing. Many of my ideas where stupid and one work colleague used to call me out on it. And every time I learned something, sometimes he did as well (i think). 

"You can turn the handle faster than the axis is moving" I think that is plain wrong. I would like to see you hand crank any commercial lathe at rapid speed; plus they stop as soon as you let go of the wheel.
To make it "feel like a direct coupling" is "worth doing" regardless, if you only use it for positioning. Admittedly a stupid idea being happy with untuned overshooting hand wheel. (I am guilty of it as well, and it did end up in tears once or twice)
I prefer not to crash the machine into the chuck, or hitting E-stop buttons when I was hand cranking too fast, so I suggest to tune that. 

"People" can crash an engine lathe using the hand wheel quite reliable. (ask any trade school teacher :-) )
If that makes a lot of sense is another question, I agree to "doesn't mean it's worth doing".

Examples:
Fine adjust for the z-axis of the surface grinder works a treat with an encoder wheel and stepper motor, because the motor does not care and over powers the stick slip without overshooting. (I klick once, it moves 0.005 mm) 
If turn an M2.5 screw on my engine lathe there is not much "feedback signal" in the sense of force feedback as well.
All sorts of machinery is using encoders to cause movement. 

Pretty much I agree, that some things might not be worth the effort.
If something is worth doing for someone else is not for me to decide.
Last edit: 3 months 3 days ago by timo.

Please Log in or Create an account to join the conversation.

More
3 months 3 days ago #348161 by rodw
Replied by rodw on topic Help Controller for a Lathe ?

There are many reasons why you should not use MPG for turning, but I will give you just one - you can turn the handle faster than the axis is moving, in other words, when you are done turning, the axis will continue to move until it reaches the commanded position.
 
Thats not correct. The user can choose how he wants his MPG to operate when he sets it up. Now I am the old crank!

Please Log in or Create an account to join the conversation.
More
3 months 1 day ago #348296 by Holzwurm56
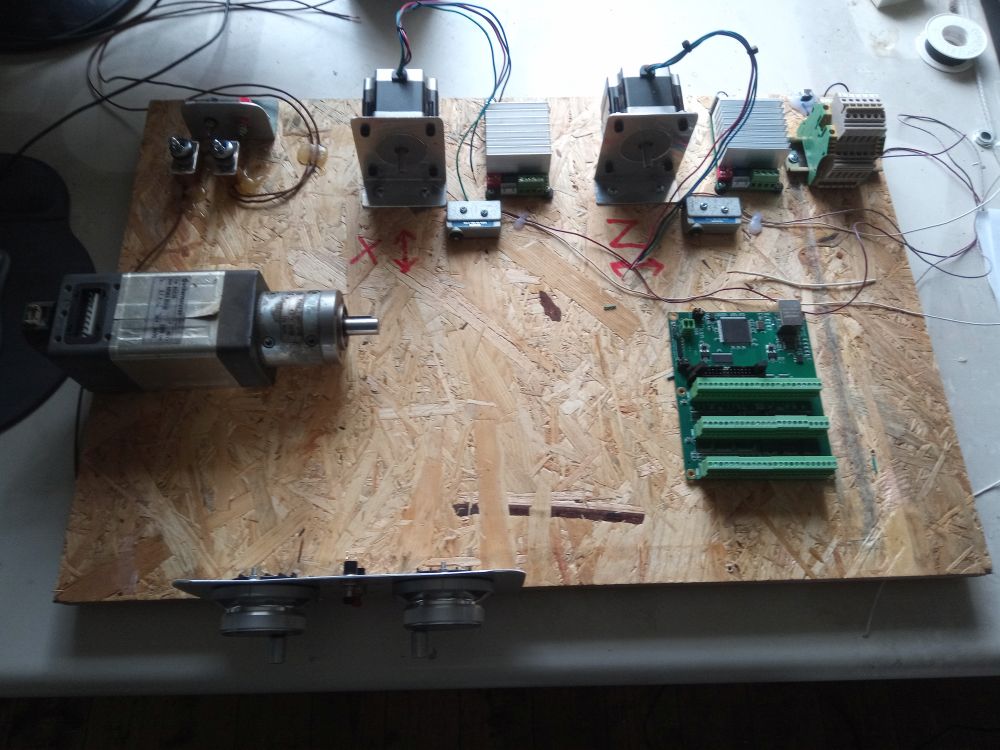
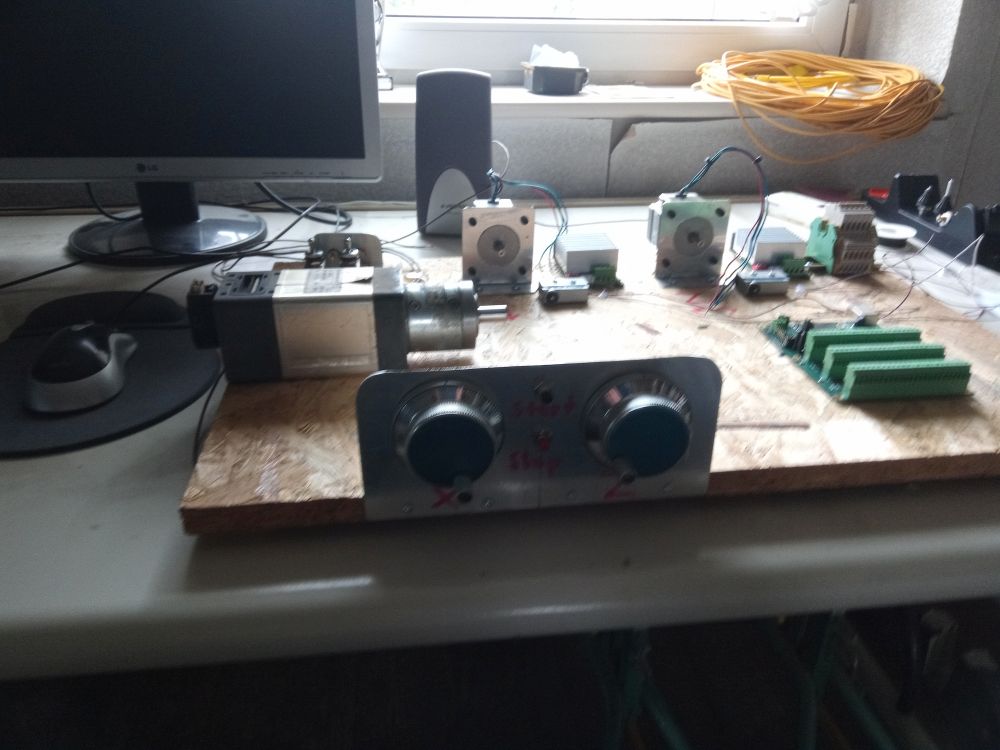
Thanks for any replies. I managed to repair my machine for the time being, but I still want to upgrade the control system. I’m currently building a makeshift lathe so I can experiment and find the best control system. I’m planning to try LinuxCNC with the 7I96—since it’s constantly being developed—though I’m not sure if I’m capable of setting it up. Mach3 is no longer being developed, but it would be my second choice, paired with an Ethernet breakout board like the PoKeys57E.
Best regards,
Hans
 
The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.
More
2 months 4 weeks ago #348429 by andypugh

There are many reasons why you should not use MPG for turning, but I will give you just one - you can turn the handle faster than the axis is moving, in other words, when you are done turning, the axis will continue to move until it reaches the commanded position.

LinuxCNC MPG inputs can be configured to stop moving as soon as the MPG stops. (Because this is such an obvious problem)

joint.N.jog-vel-mode

at

linuxcnc.org/docs/stable/html/man/man9/motion.9.html

Please Log in or Create an account to join the conversation.

More
2 months 4 weeks ago #348430 by Holzwurm56
I use UHU DC servo controllers. They compare the actual position with the target position. If the deviation is too large—for example, if I crank faster than the axis moves—the controller goes into a fault state and stop the axismoving.

Please Log in or Create an account to join the conversation.

Time to create page: 0.488 seconds
Powered by Kunena Forum
