
Plasma build basic questions


So what voltage are you running your dives at?
Please Log in or Create an account to join the conversation.

I just want to try to not make the same mistakes building my own.
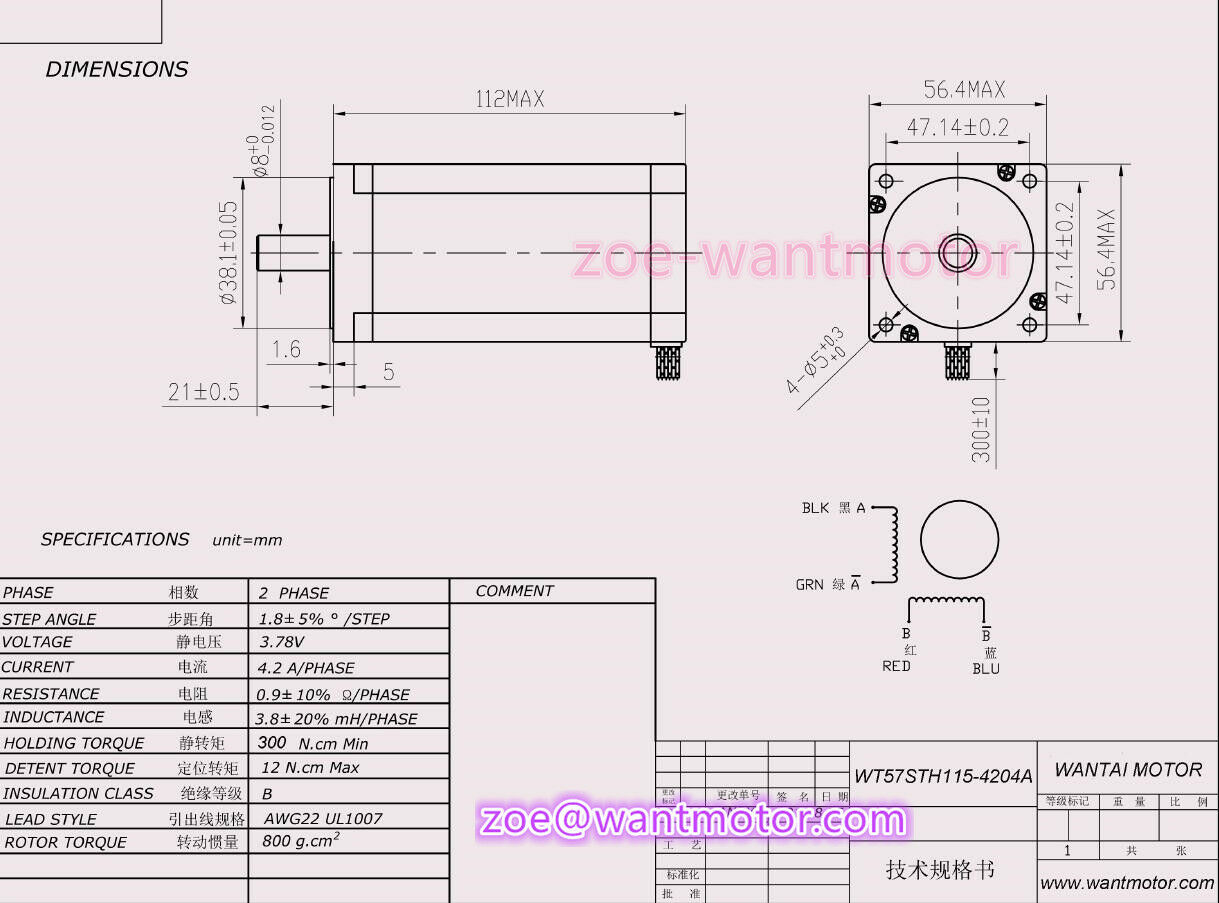
The motors on the table I'm using are Wantai WT57STH115-4204A. 4.2A 1.8 deg
The drives are Me 2H Microstep Driver DQ856MA
They are set to 4A RMS / 6.6A peak and 3200 pulse.
The power supplies are 48 volts.
I've attached the info I found on the motors. I assume they're nothing great,
There's two on the Y axis and one for Z and one for X. All but Z are setup as a rack and pinion. Don't know the ratio right now.
Please Log in or Create an account to join the conversation.
I think What Tommy said about grounding might be required. Bolt a seperate wire to a mounting bolt on each motor and run it back to a star ground point.
I would also seperate the motors from the racks so you can push the gantry around. I can push mine with my little finger like this. If there is any binding, work out what it is and fix it. Then remove the motors so avoid any back emf and do the same thing with the rack and pinion engaged. Perhaps this is the first step. I have a little bit of binding on my X axis rack and pinion when engaged. I think becasue of crappy rack and pinion.
Please Log in or Create an account to join the conversation.
rodw wrote: They look like they should work depending on gantry weight.
I think What Tommy said about grounding might be required. Bolt a seperate wire to a mounting bolt on each motor and run it back to a star ground point.
I would also seperate the motors from the racks so you can push the gantry around. I can push mine with my little finger like this. If there is any binding, work out what it is and fix it. Then remove the motors so avoid any back emf and do the same thing with the rack and pinion engaged. Perhaps this is the first step. I have a little bit of binding on my X axis rack and pinion when engaged. I think becasue of crappy rack and pinion.
Removing the motors so I can feel things move on their own is a good idea, I didn't think of that.
Something I can't wrap my head around is cutting 1/4" 304 SS I had issues with round holes not even being close to round and I thought it was because the plate was warped. Yet, I just tried burning a bunch of test holes in some 1/4" steel and they came out perfect. I then put the plate on a pretty steep angle and they still came out good. So, I don't know if it's an issue with SS, or that specific SS, or what's going on.
I'm running a Hypertherm Powermax 125 and was using 45A at those times. I usually get a pretty good cut, but, there's sometimes where not so much.
Please Log in or Create an account to join the conversation.
I vaguely remember from my cut charts that you need a "hotter" torch for stainless vs mild steel.
One commercial guy I knew who cut all day every day had a rule of thumb he had which was 10 amps per mm of steel. So by his benchmark, 45 amps is too low, I'd try 60-80 amps depending on available consumables..
Please Log in or Create an account to join the conversation.
rodw wrote: I've not cut much stainless, only thin stuff.
I vaguely remember from my cut charts that you need a "hotter" torch for stainless vs mild steel.
One commercial guy I knew who cut all day every day had a rule of thumb he had which was 10 amps per mm of steel. So by his benchmark, 45 amps is too low, I'd try 60-80 amps depending on available consumables..
I go by Hypertherm's charts and use the lowest current I can.
Perhaps that's a mistake, but they say 45A will cut 1/4" stainless so I assume that'll give me the best cut vs more current and higher speeds.
I'm certainly open to suggestions tho.
Please Log in or Create an account to join the conversation.