Can't run first job with qtdragon_hd

More
4 years 10 months ago #229756 by ucancallmebob89
That was super helpful, thank you! I didn't realize qtdragon_hd.ui had the color and off-color both defined as green by default. That really should be changed to avoid this confusion.

Please Log in or Create an account to join the conversation.

More
4 years 10 months ago #229758 by ucancallmebob89
Ok so after cleaning up my .hal files this is what I have right now in my PrintNC config folder. I'm still seeing the behavior where the job hangs at line 16.

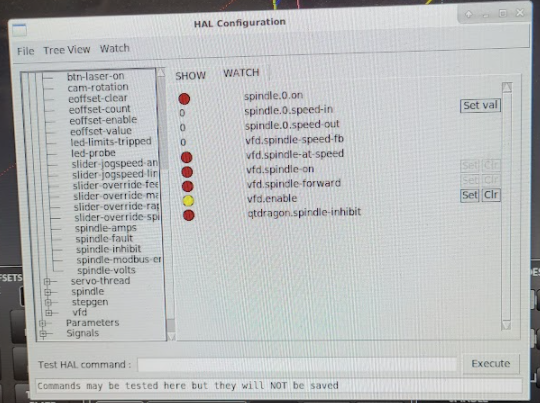
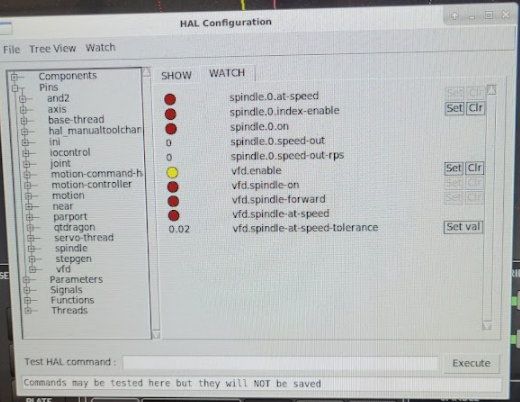
I did a HAL show on several relevant pins.
 

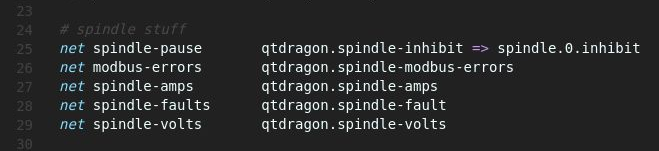
In my custom_postgui.hal I have these spindle settings:
 

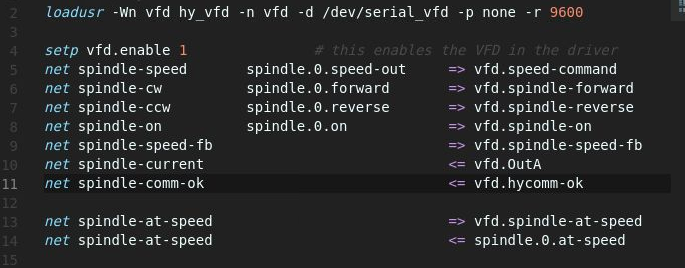
And in vfd.hal I have these spindle settings:
 

Do I need a line that does "setp spindle-at-speed true"? Because I thought the point of having the serial connection to the VFD is that it can tell me when it is at speed instead of manually setting it.

Please Log in or Create an account to join the conversation.

More
4 years 10 months ago #229788 by ucancallmebob89
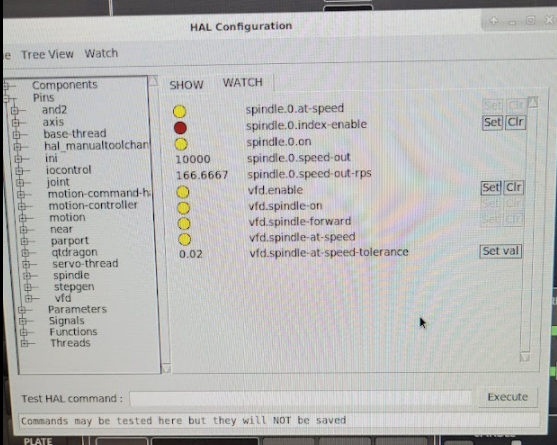
So I'm thinking now that this is not a spindle-at-speed problem. I just did hal show on a bunch of spindle and vfd related pins while running the spindle manually and then while attempting to run my gcode file.

Manually turning spindle on:
 

Running my gcode file:
 

Everything seems to be working fine when I turn on the spindle in manual mode. Is there something weird going on in my gcode file?

Please Log in or Create an account to join the conversation.

More
4 years 10 months ago #229794 by cmorley
your program runs fine on a sim config.

Please Log in or Create an account to join the conversation.

More
4 years 10 months ago - 4 years 10 months ago #229814 by ucancallmebob89
Progress! It has to do with my toolchange operation. I started commenting out one line at a time in my gcode file and it was able to run after I commented out "T3 M6".

Now I just have to figure out why that's causing a problem.

Here are my toolchange related config settings. I'm using a manual toolchange operation. I want the machine to go to G53 X100 Y100 Z0. I have TOOL_CHANGE_QUILL_UP = 1 because I want it to raise Z all the way up before moving to the toolchange position.

In my INI, here's my EMCIO section:
Code:
[EMCIO] EMCIO = io CYCLE_TIME = 0.100 TOOL_TABLE = tool.tbl TOOL_CHANGE_WITH_SPINDLE_ON = 0 TOOL_CHANGE_QUILL_UP = 1 TOOL_CHANGE_POSITION = 200 100 0

In my postgui file, here's my tool change info. I've tried it with the unlinkp lines commented and uncommented, and it hasn't changed the behavior.
Code:
# the unlink pin commands are only used, because they are connected # in core_sim.hal and we use this file to simulate # unlinkp iocontrol.0.tool-change # unlinkp iocontrol.0.tool-changed # unlinkp iocontrol.0.tool-prep-number     net tool-change         hal_manualtoolchange.change   <=  iocontrol.0.tool-change net tool-changed        hal_manualtoolchange.changed  <=  iocontrol.0.tool-changed net tool-prep-number    hal_manualtoolchange.number   <=  iocontrol.0.tool-prep-number

According to this , I expected a little message box to appear showing to facilitate the manual toolchange, but that never happened.

Last edit: 4 years 10 months ago by ucancallmebob89.

Please Log in or Create an account to join the conversation.

More
4 years 10 months ago #229820 by hottabich
Try replacing the Tool.tbl file to the attached and everything will work.

Please Log in or Create an account to join the conversation.

Moderators: cmorley
Time to create page: 0.273 seconds
Powered by Kunena Forum