New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
- retrofitcenter
- Offline
- New Member
-

Less
More
- Posts: 5
- Thank you received: 10
01 Oct 2026 20:10 #350051
by retrofitcenter
New LinuxCNC Multi-Channel System – Looking for Testers & Feedback was created by retrofitcenter
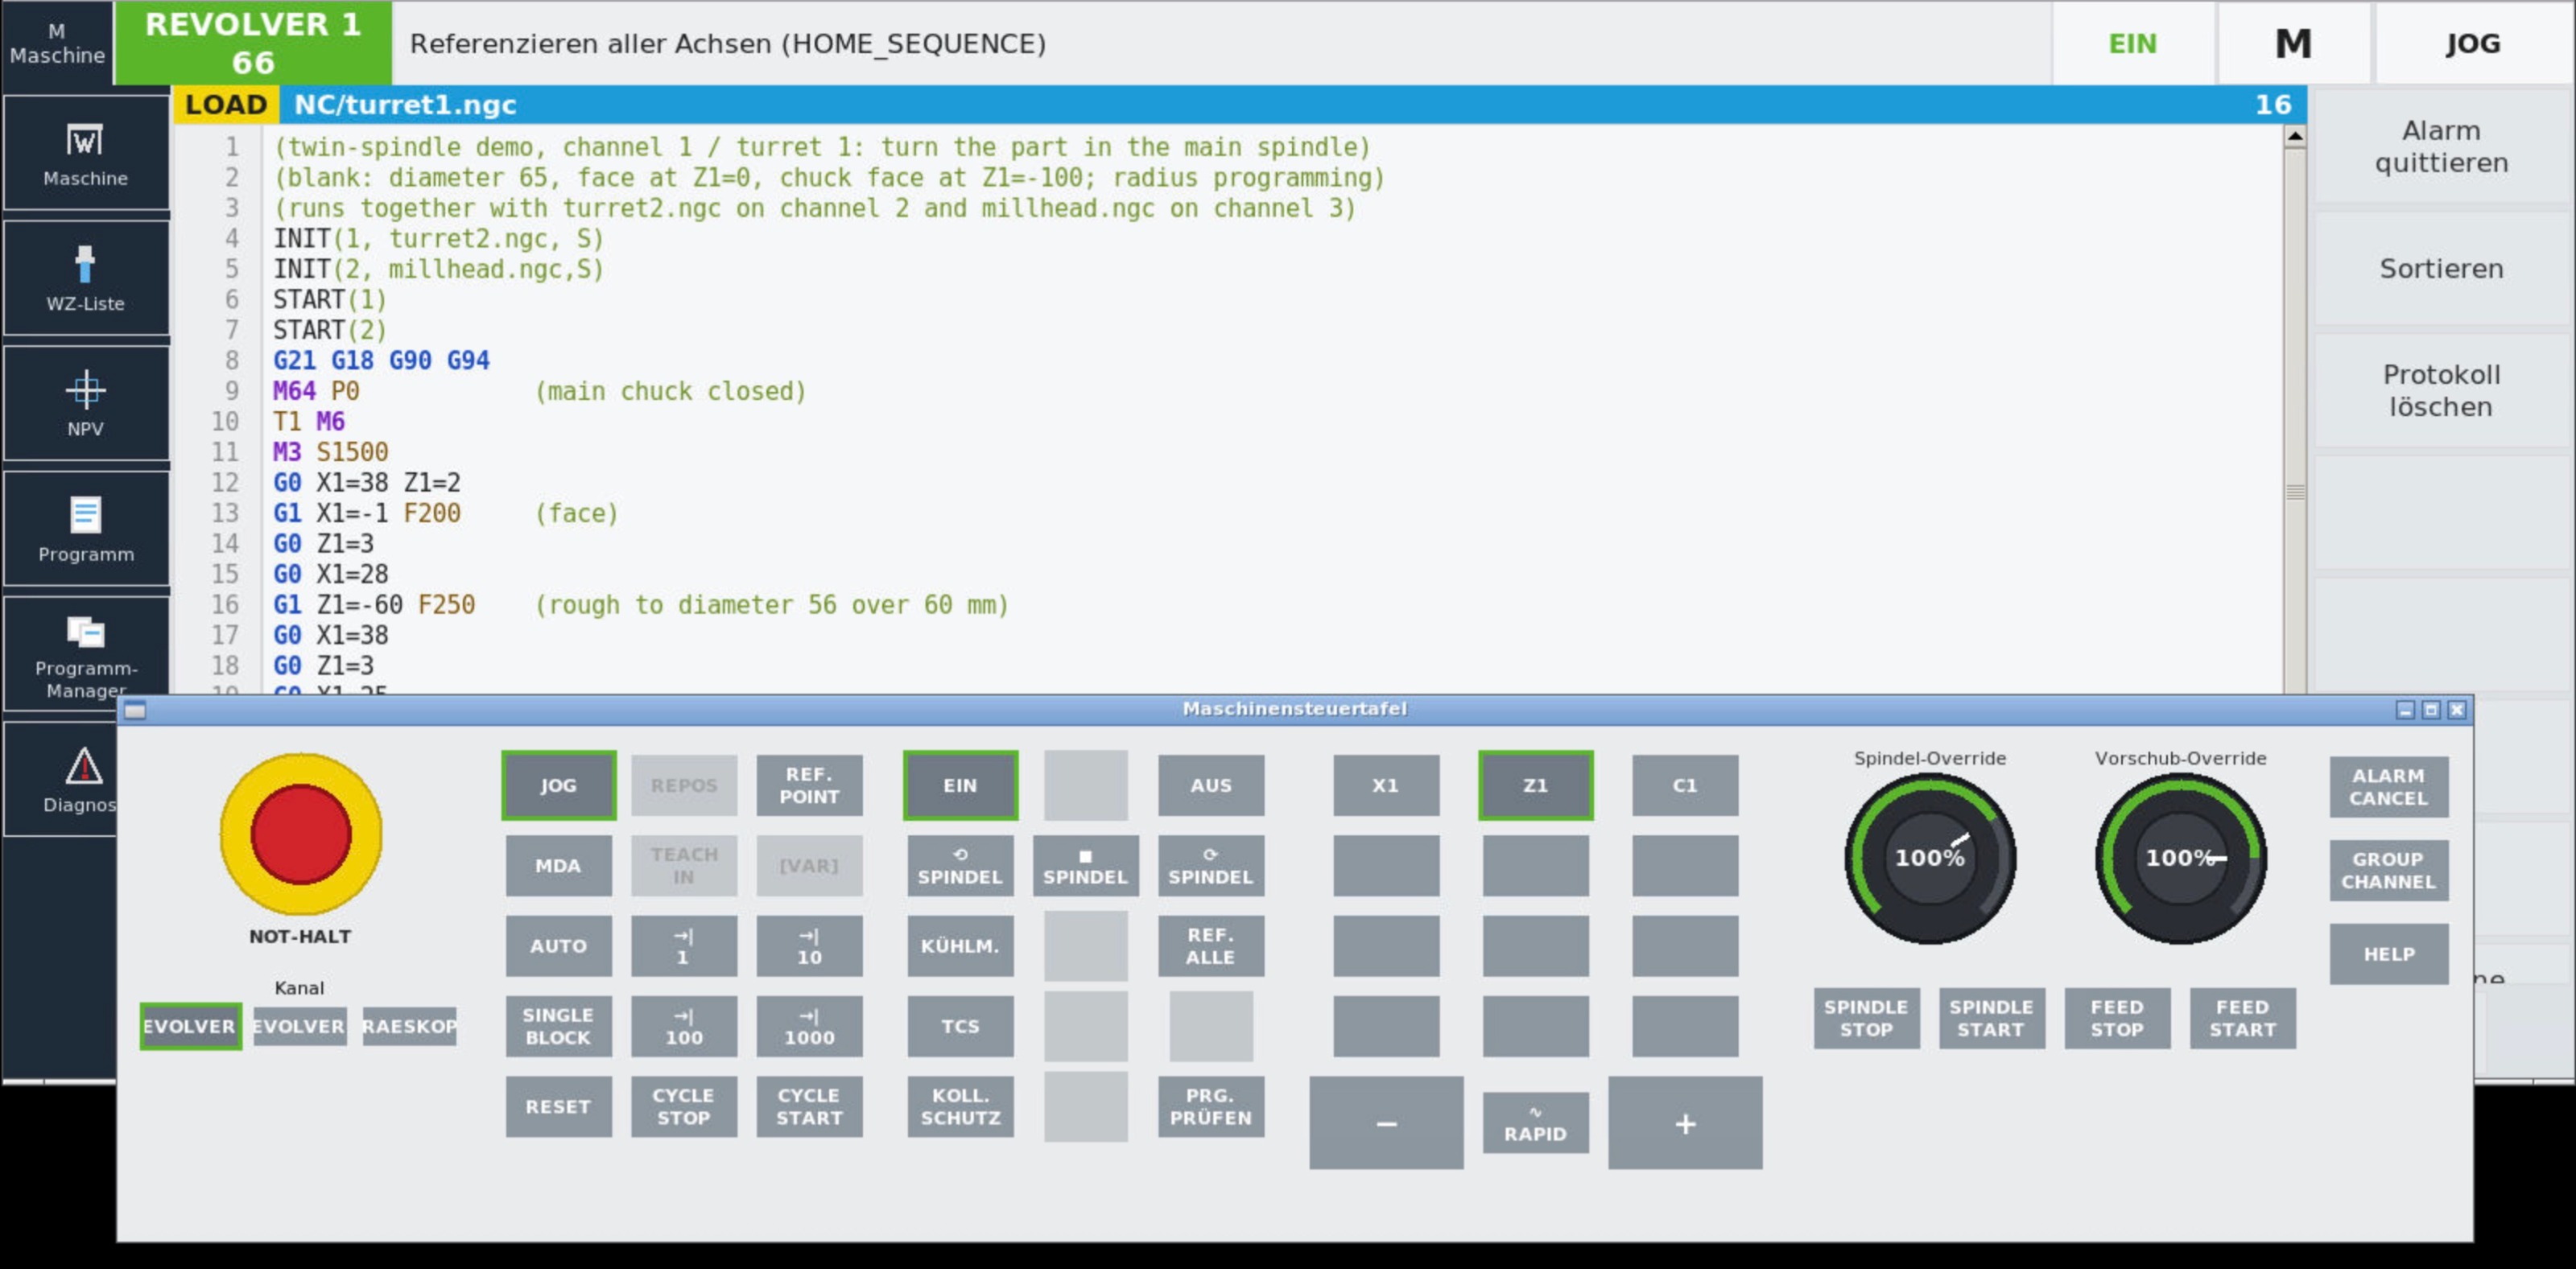
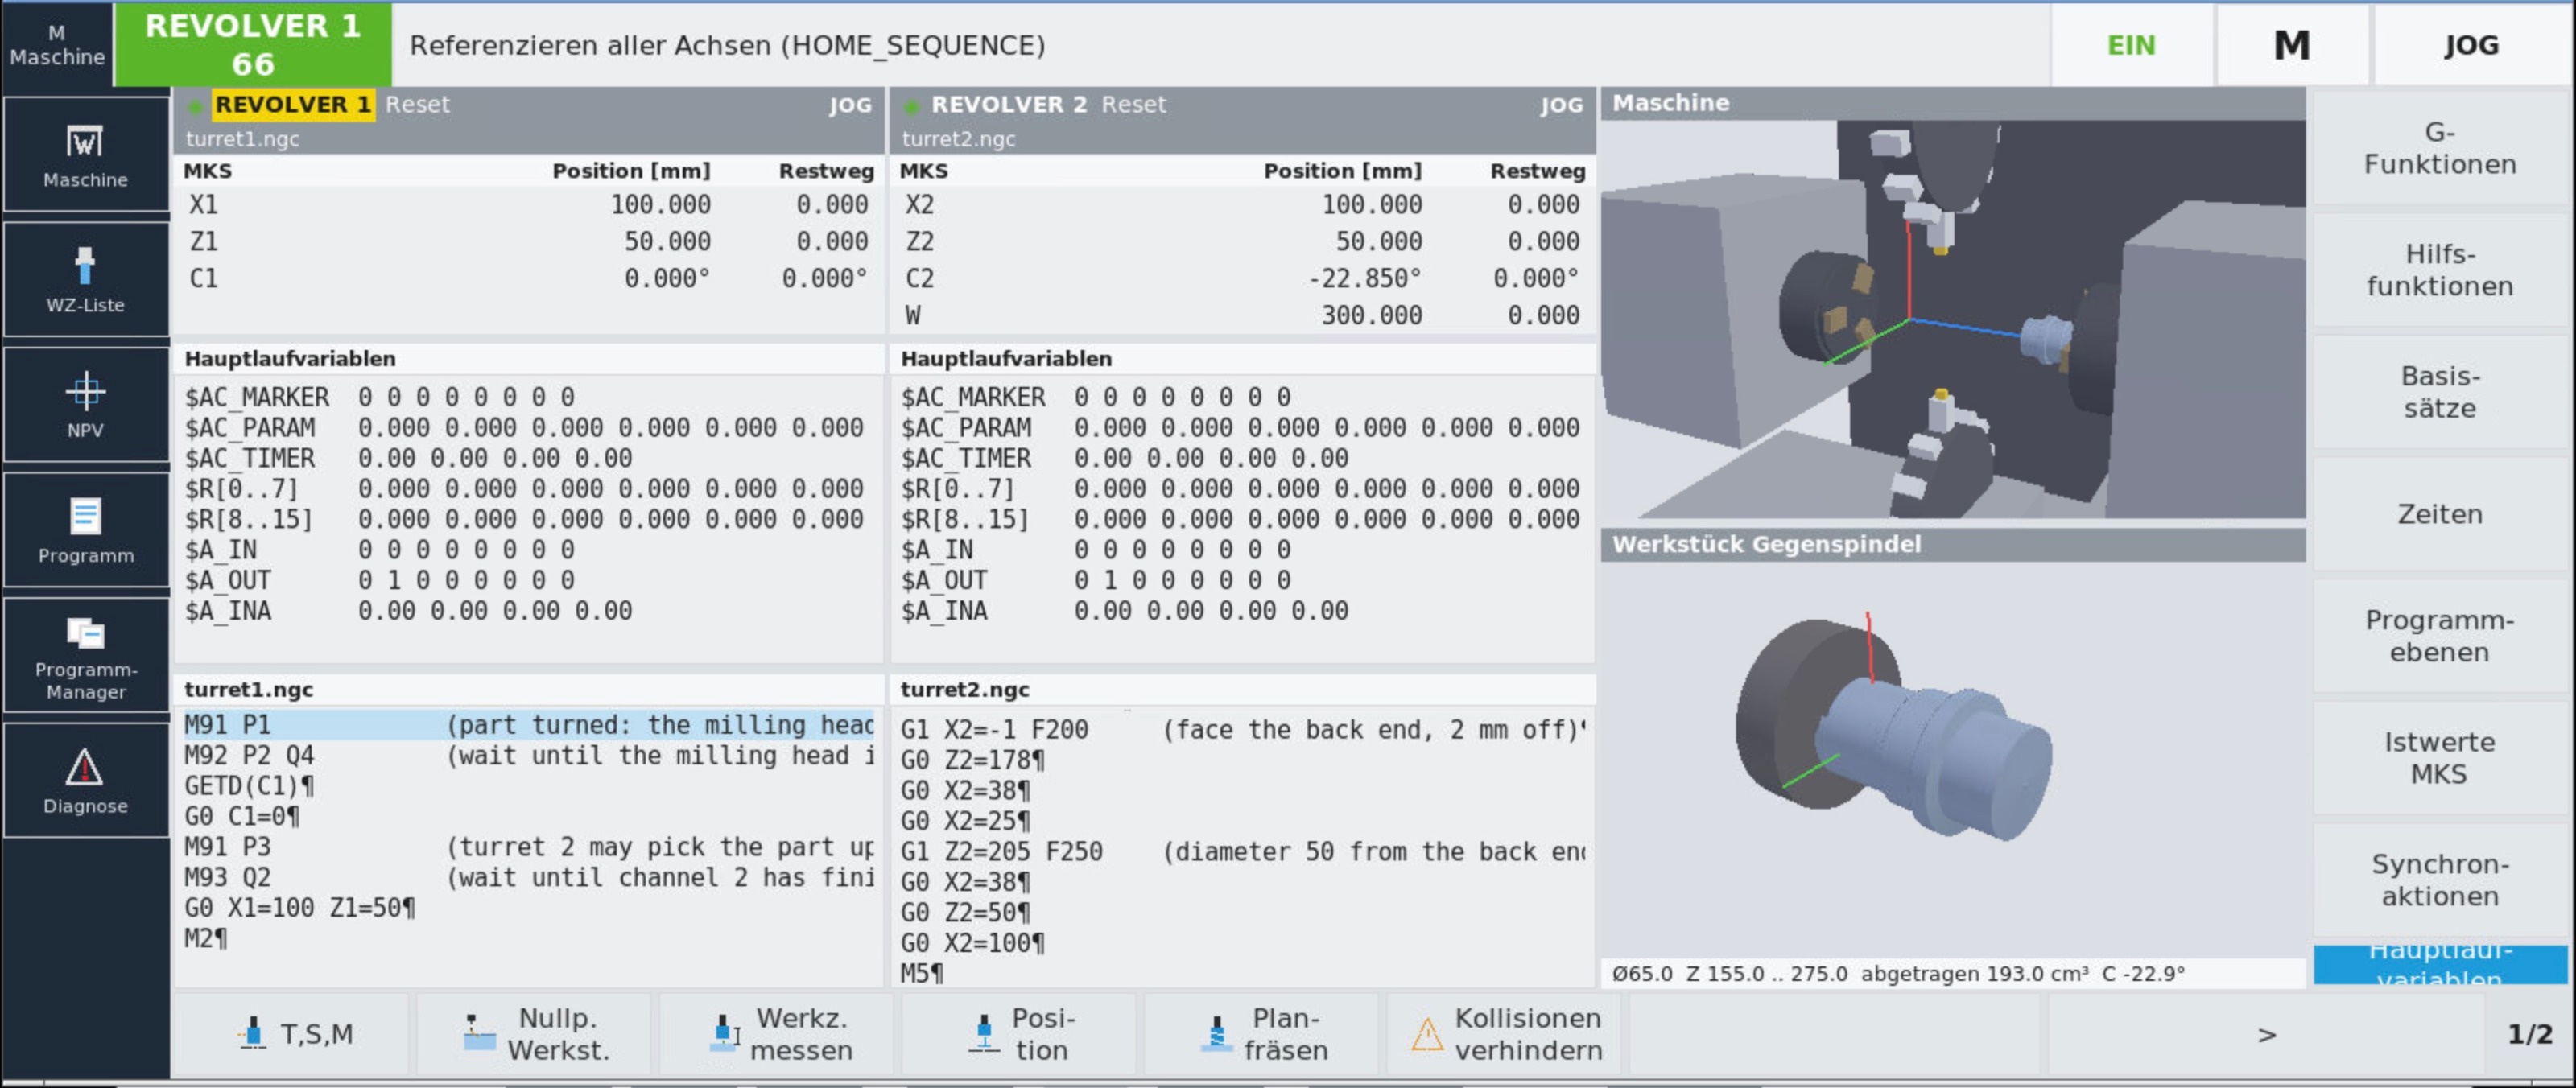
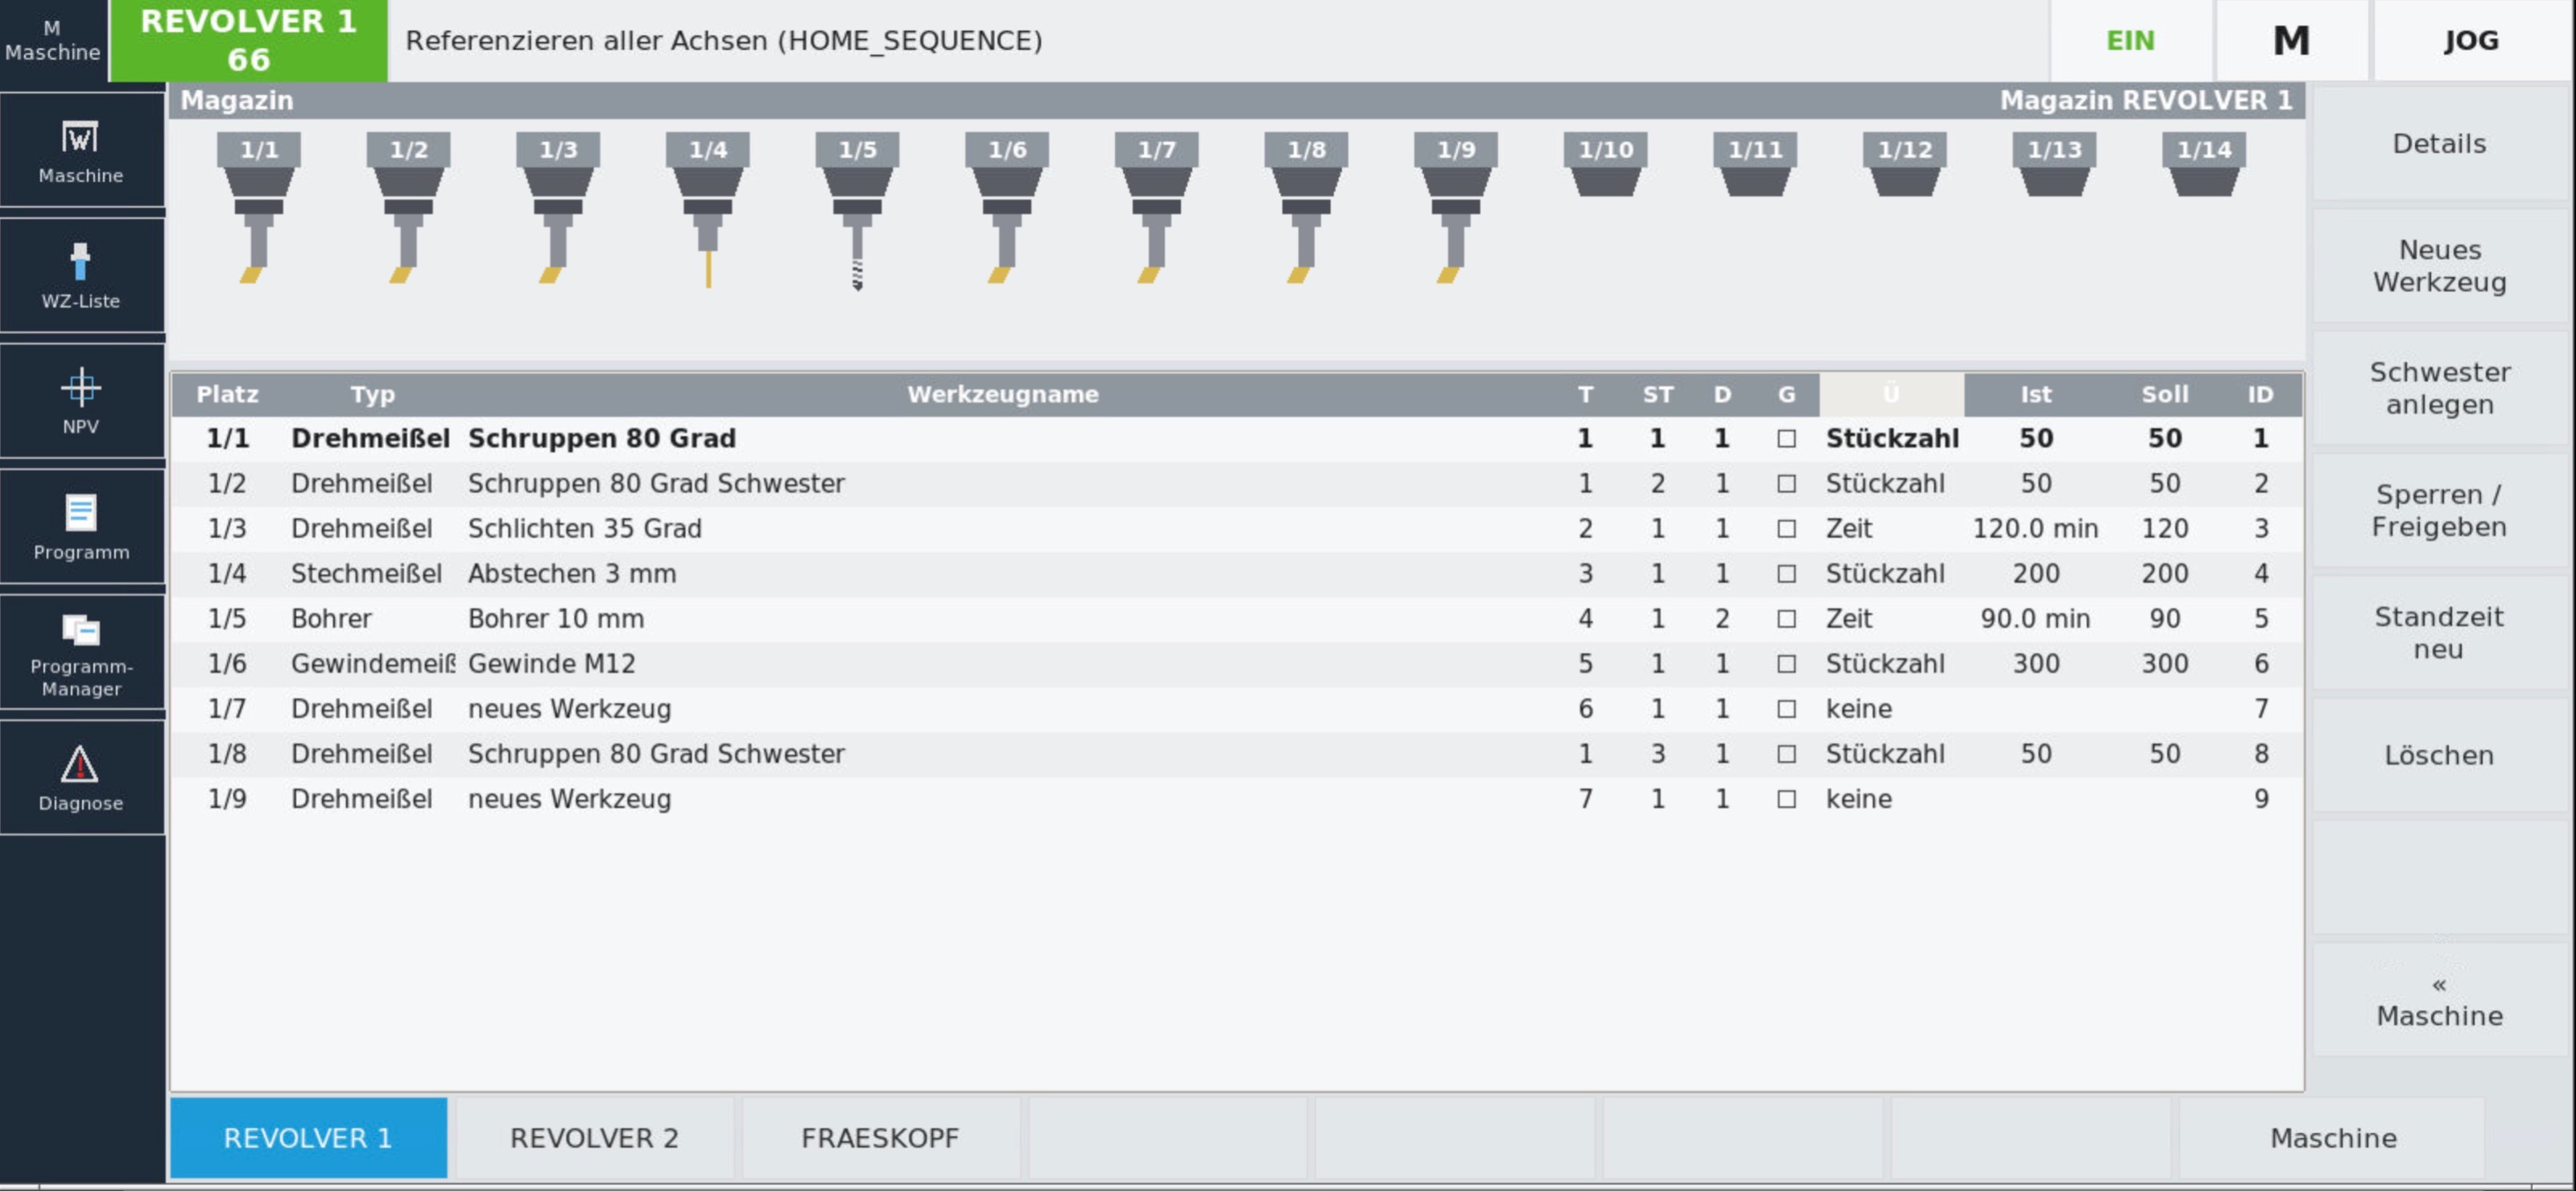
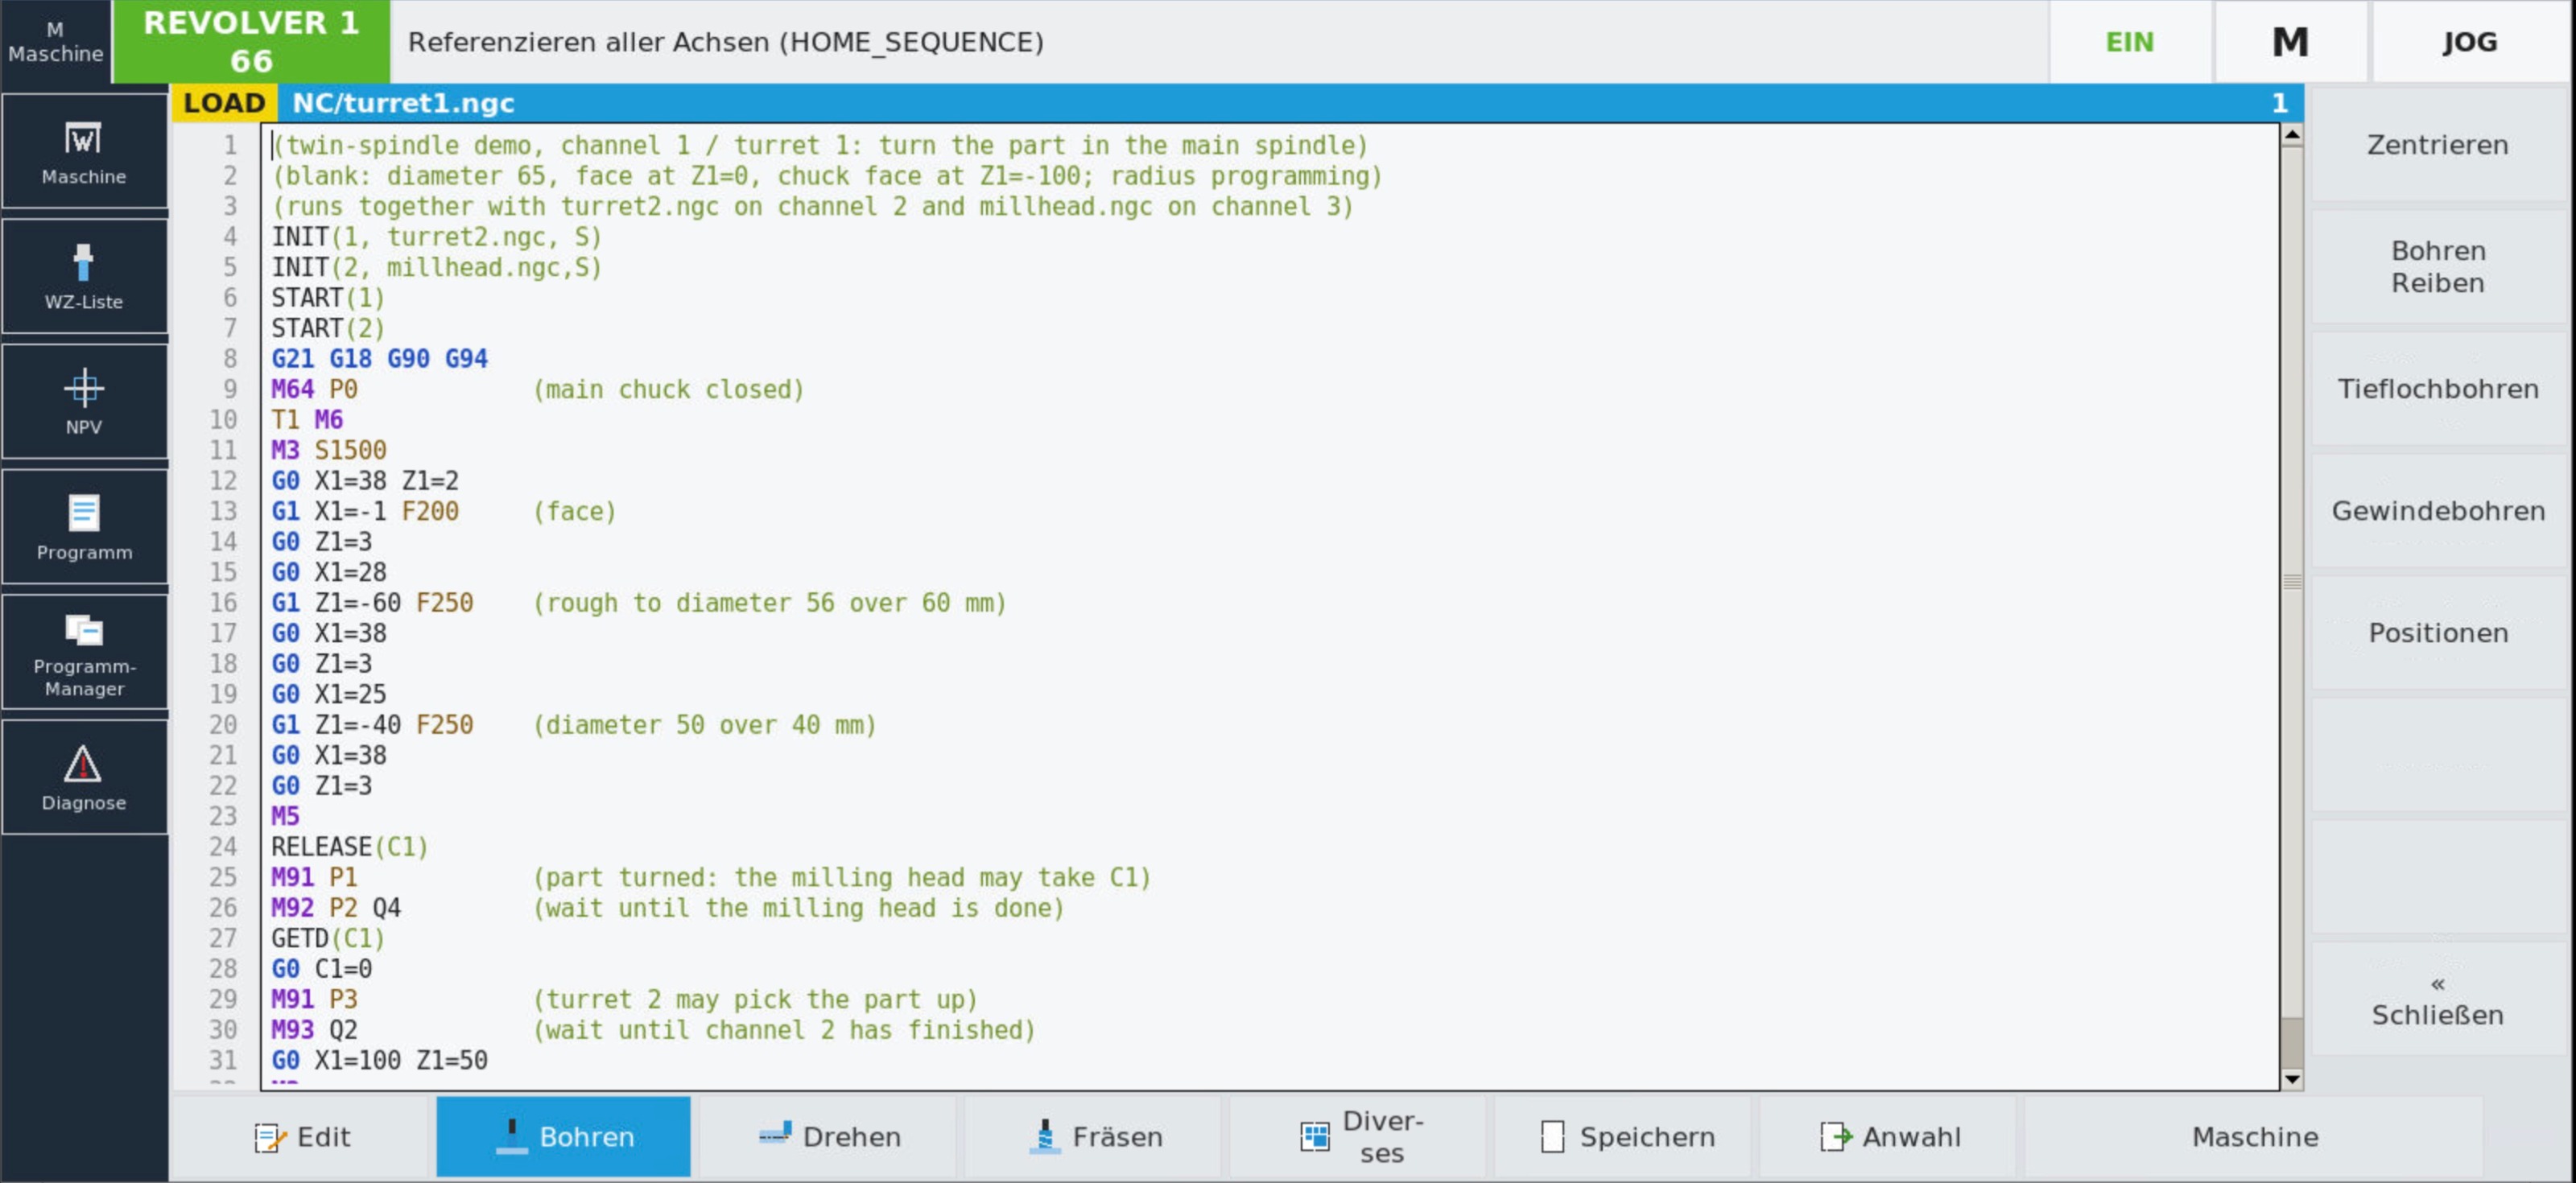
Hi everyone,I’ve been working on a new multi-channel extension for LinuxCNC, mainly targeting complex turning/milling machines such as INDEX, Gildemeister, multi-spindle lathes and other machines with several independent machining units.The goal is to bring LinuxCNC much closer to the functionality normally found on industrial controls such as Siemens SINUMERIK, especially for machines with multiple turrets, spindles and synchronized machining processes.Main featuresMultiple CNC channelsThe system can run multiple independent machining channels simultaneously. The architecture is not limited to just two channels and is designed to support a very large number of channels, depending mainly on the hardware and machine configuration.Each channel can execute its own NC program independently.Example:Dynamic axis assignmentAxes are not permanently tied to one channel.An axis can be transferred from one machining channel to another during operation.For example:This makes it possible to handle machines where several machining units need temporary access to the same spindle or axis.Channel synchronizationThe system includes synchronization functions similar to those used on industrial multi-channel controls.Channels can wait for each other or synchronize at defined points inside their NC programs.Typical applications are:
Channel 1 → Turret 1 / Main spindle
Channel 2 → Turret 2 / Sub spindle
Channel 3 → Milling unit
Channel 4 → Additional machining unit
...Channel 1:
X1 Z1 C1
Channel 2:
X2 Z2 C2
Transfer C1 →
Channel 2:
X2 Z2 C2 C1- part transfer between main and sub spindle
- synchronized machining
- waiting for another turret
- synchronized spindle operations
- coordinated tool changes
- machining sequences involving several channels
- cylindrical surface machining
- face machining
- C-axis milling
- turning/milling combinations
- complete machine geometry
- tools
- workpiece
- fixtures
- spindles
- turrets
- axis movements
- tool and machine
- tool and chuck
- tool and fixture
- turret and spindle
- machine components
- workpiece and machine
- tool geometry
- tool offsets
- sister tools
- tool life monitoring
- remaining tool life
- automatic replacement with sister tools
- tool status
- tool usage tracking
- INDEX machines
- Gildemeister / DMG machines
- multi-spindle machines
- dual-turret lathes
- main/sub-spindle machines
- complex LinuxCNC configurations
The following user(s) said Thank You: grandixximo, tommylight, jschulze, besriworld, COFHAL, hermann1976, spumco
Please Log in or Create an account to join the conversation.
- tommylight
-
- Away
- Moderator
-

Less
More
- Posts: 21951
- Thank you received: 7472
01 Oct 2026 21:13 #350053
by tommylight
Replied by tommylight on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
Thank you very much, this is a huge addition to the project, but i have to ask, is this going to be open source?
Or maybe i missed it from a quick glance....
Or maybe i missed it from a quick glance....
Please Log in or Create an account to join the conversation.
- spumco
- Away
- Platinum Member
-

Less
More
- Posts: 2180
- Thank you received: 905
02 Oct 2026 15:25 #350071
by spumco
Replied by spumco on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
If anyone is interested in testing the system, contributing, or discussing the architecture, I’d be happy to share more details, screenshots and videos.
I don't have a machine that's a perfect candidate for testing, but I do have a subspindle gang-tool lathe with a separate parting slide mounted to the headstock. Both the slide - configured as either a V or X axis using switchkins - and the subspindle could be re-configured in a separate channel if that would be of any use to you.
Just to clarify, my sub is mounted on the X-slide and is intended to be used with tools (eventually) mounted next to the headstock for back-work.
My operations are (will be) sequential, other than the parting and sub hand-off; it's not the textbook example of multi-channel like a swiss or sliding headstock.
I am not skilled enough to really help with coding, but if you can walk me through a configuration and GUI setup I'd be happy to try something. Servos are step/dir with glass scale feedback.
And another thing... I struggled with LCNC's limitations on axis letters. While my main spindle is also the C-axis, my sub is not defined as an axis despite being mechanically capable of it (servo driven). I'm not aware of any way to add axes beyond the standard 9 which also participate in the trajectory planner (i.e. not 'extra-joints'). I would rally have liked to name the sub "C2" or similar. In your post you indicated 'C1' and 'C2' and that axes could be shifted between channels, but it's not clear how axes beyond the usual letters are named or handled. I'd be interested in how you're addressing duplicate axis names - a basic swiss lathe capable of simultaneous sub work would need C1, X1, Z1 (main) and C2, X2, Z2 (sub).
As @tommylight said, this would be a monumental addition to LCNC.
The following user(s) said Thank You: COFHAL
Please Log in or Create an account to join the conversation.
- spumco
- Away
- Platinum Member
-
Less
More
- Posts: 2180
- Thank you received: 905
02 Oct 2026 15:31 #350072
by spumco
Replied by spumco on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
I’m also looking for a real machine for extended testing of the multi-channel system. It does not matter whether the machine still has the original drives.
Are you located in the US? If so, I can help you find/obtain a really cheap machine for testing. HGR Surplus typically has a number of obsolete swiss-type lathes for sale that can be had for essentially scrap value.
I'm only about an hour from HGR and can get eyes on any machine candidates if you're serious about acquiring hardware for testing.
The following user(s) said Thank You: tommylight, endian
Please Log in or Create an account to join the conversation.
- retrofitcenter
- Offline
- New Member
-
Less
More
- Posts: 5
- Thank you received: 10
05 Oct 2026 07:46 #350117
by retrofitcenter
Replied by retrofitcenter on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
Yes, it will be open source. I’m just still finalizing the first proper release before publishing everything.
At the moment I’m integrating a lot of functionality inspired by industrial CNC systems such as Siemens, especially channel synchronization, spindle/axis synchronization and transformations for turning/milling centers, including face and cylindrical surface machining.
Another major part is the simulation system, including material removal, machine visualization and collision/crash detection.
The tool management is also being heavily extended with a proper tool database, sister tools, lifetime monitoring and 3D models of tools and fixtures.
I’d rather release a solid first version with a clean structure and documentation than publish something half-finished. Once that first release is ready, the source will be made available.
Please Log in or Create an account to join the conversation.
- retrofitcenter
- Offline
- New Member
-
Less
More
- Posts: 5
- Thank you received: 10
05 Oct 2026 07:56 #350118
by retrofitcenter
Replied by retrofitcenter on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
Thanks a lot for the detailed description and the offer – that's exactly the kind of machine I'd like to test with.
Your setup is actually a very good candidate, even if it's not a classic swiss. A main spindle with its own X/Z, plus a parting slide and a subspindle that need to synchronise for the hand-off, is precisely the situation where a second channel makes sense. Sequential operations are fine – the interesting part is the synchronisation at the hand-off point, and that's what I want to validate on real hardware. Step/dir with glass scale feedback is also a good test case.
Regarding axis names: the 9-letter limit stays as it is inside each channel. Every channel has its own task, interpreter and trajectory planner, so each channel has its own XYZABCUVW namespace. A G-code program running in channel 2 simply uses X, Z and C – the interpreter doesn't need to know about "C2". The names C1/C2, X1/X2 etc. are the global, channel-qualified identifiers used in the configuration, the HAL side and the GUI, so a swiss with C1/X1/Z1 (main) and C2/X2/Z2 (sub) is no problem. In your case the sub would become a real C axis in channel 2 and take part in that channel's trajectory planner, instead of being an extra joint.
Axes are assigned to a channel in the configuration, and the idea is that an axis can be handed over from one channel to another at runtime (e.g. for a transfer move). That part is still being worked on.
No coding needed from your side – I'll prepare a configuration for your machine and walk you through it step by step. To get started, could you send me:
- your current INI and HAL files
- which hardware/FPGA card you use
- a short sketch or photo of the machine layout (main, sub, parting slide)
- a typical part program, especially the parting/hand-off sequence
Then I'll come back with a proposed 2-channel layout and a test plan. I'll also share screenshots and a short video of the current state soon.
@spumco – thank you very much for the offer, I really appreciate it. I'm based in Austria, not in the US. However, I'll be in California from October 17 to November 17. I'm tied up with an important project during that time, but I'd be glad to meet up while I'm there and talk about how we could move forward – whether that's a machine from HGR or another way to get real swiss-type hardware for testing. I know California isn't exactly next door for you, so a video call would work for me as well. Just send me a PM and we'll find a date.
Thanks again – and thanks @tommylight for the support!
The following user(s) said Thank You: tommylight, spumco
Please Log in or Create an account to join the conversation.
- spumco
- Away
- Platinum Member
-
Less
More
- Posts: 2180
- Thank you received: 905
05 Oct 2026 13:36 #350122
by spumco
Replied by spumco on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
@retrofitcenter...
This forum has no PM functionality. Do you have a github repo or similar location where I could provide my config and related files?
I have no issues posting files here, but the inevitable back-and-forth with file transfers during iteration gets really clumsy when done through a forum.
I'd be happy to discuss whatever you'd like during a video call.
This is the sort of thing I'm talking about: $6k for a 32mm swiss. Probably get it for 5.
hgrinc.com/productDetail/CNC/Used-Star-M...C-Lathe/11240360356/
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- tommylight
-
- Away
- Moderator
-
Less
More
- Posts: 21951
- Thank you received: 7472
05 Oct 2026 14:27 #350125
by tommylight
Replied by tommylight on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
Thank you.Yes, it will be open source.
Please Log in or Create an account to join the conversation.
- retrofitcenter
- Offline
- New Member
-
Less
More
- Posts: 5
- Thank you received: 10
05 Oct 2026 15:02 #350126
by retrofitcenter
Replied by retrofitcenter on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
absolutely. I agree that exchanging files through the forum would get cumbersome very quickly once we start iterating.
I’m using GitLab for the development, so I think that would be the easiest solution. I can set up a dedicated repository/project for the testing where you can upload your LinuxCNC configuration, HAL/INI files, custom components, machine documentation, etc. We can then track changes through Git and use issues for individual problems or features.
If you don’t want your machine configuration to be public, that’s no problem, I can make the repository private and give you access directly.
A video call would also be very useful. Especially at the beginning, it would probably save quite a bit of back-and-forth if you could show me the machine architecture, channels, spindles, axes and what you want to achieve.
And yes, the 32 mm Swiss-type machine is exactly the kind of machine I’m looking for. For around $5–6k it could be a very interesting test platform for the multichannel system.
I’ll prepare the GitLab structure and send you access/details.
The following user(s) said Thank You: spumco
Please Log in or Create an account to join the conversation.
- hermann1976
-
- Offline
- Senior Member
-

Less
More
- Posts: 67
- Thank you received: 16
05 Oct 2026 16:37 #350128
by hermann1976
Replied by hermann1976 on topic New LinuxCNC Multi-Channel System – Looking for Testers & Feedback
@retrofitcenter...
Hi , I gathered that you’re from Austria. I am too.
I think what you’re aiming to implement in LinuxCNC is great and exciting.
The multi-channel control option is definitely a real asset to the LinuxCNC project.
It makes it possible to successfully retrofit older machines—such as complete Homag woodworking centers with multiple table zones—using LinuxCNC. I work in the woodworking industry myself.
I also took a look around your website—you’re working on some great projects there.
What kind of training or education did you complete? Mechanical engineering?
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
Time to create page: 0.159 seconds