Planning to Retrofit a Mazak Integrex200Y Mill-Turn Machine

More
1 year 5 months ago - 1 year 5 months ago #327741 by jochen91
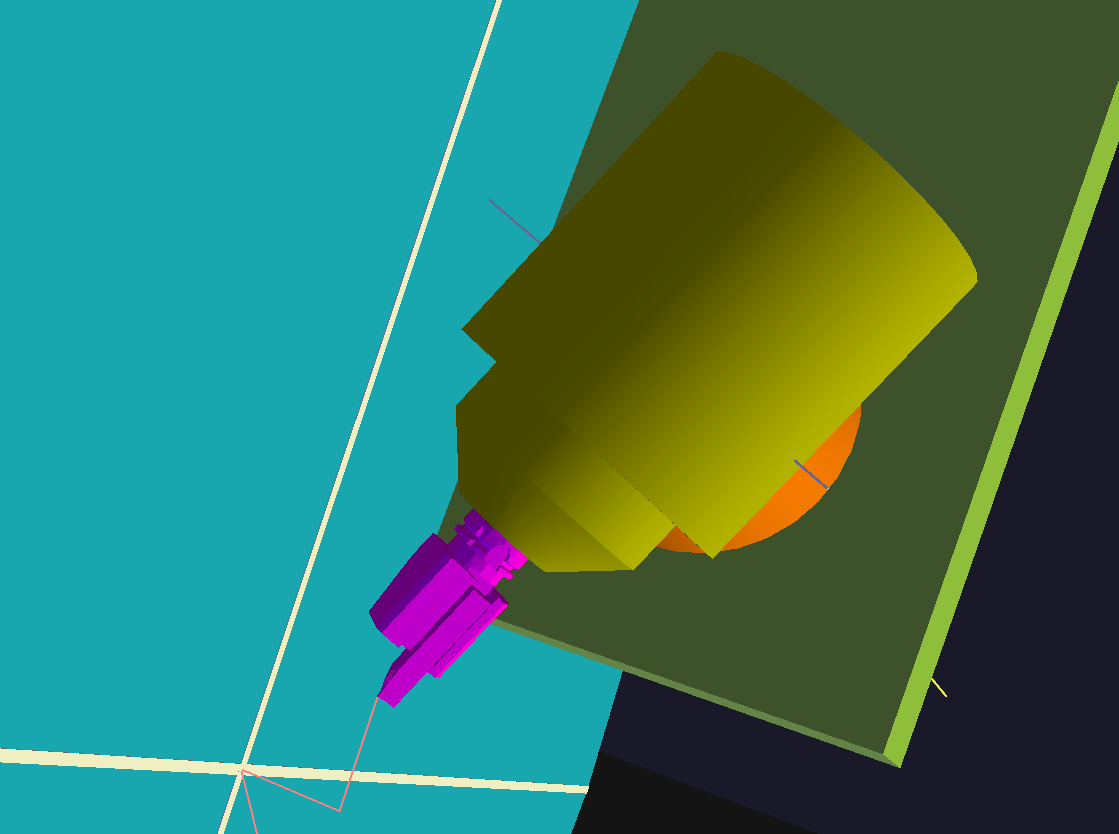
I did model up a test piece in Fusion:

The machine type selected in the PP was PUMA MX.

Warning: Spoiler!


It look like only G400/G368/G17 and G18 is used.You said that G17,G18 and G368 can be replaced with G68.3 and G53.1 which i understand, but what about G400 ? (Functionality is documented in the .pdf). I think if those GCodes changes are implemented into the PP. The Doosan PP is sorta ready for LCNC (besides various M-codes).I can't test the TCP behavior of the PP since i don't have the manufacturing extension for Fusion.

Kind regards,
Jochen 
Last edit: 1 year 5 months ago by jochen91.

Please Log in or Create an account to join the conversation.
More
1 year 5 months ago - 1 year 5 months ago #327744 by Aciera
Looks like G368/G369 can be handled by the TWP functionality.
G400 is different as it transforms the tool offset rather than the tool position.
I'm not very familiar with cnc turning so I have little idea how linuxcnc handles the tool orientation as set in 'R' and 'K' words. There is this document which also refers to tool orientation but I have really no idea if this is actually used in motion planning or only in the GUI.
linuxcnc.org/docs/html/lathe/lathe-user.html
I'd say it's certainly possible to recreate this using a python remap.
Note though that even Doosan suggest that it is more accurate to touch off the tool at the b-axis angle used in the operation.
Last edit: 1 year 5 months ago by Aciera.
The following user(s) said Thank You: jochen91

Please Log in or Create an account to join the conversation.

More
1 year 5 months ago #327756 by jochen91
Hello,
so after some digging around i found the Doosan G Code explanation sheet. I uploaded it into my GitHub so everybody can access it. It was a pain in the **** to get it.

github.com/jochenr91/Integrex

It explains every G-code the machine accepts. Including G400 starting on Page 155 (Page 157 with example pictures).

Also interessting: The Doosan Machine exepts G68:

Three-dimensional coordinate conversion without B-axis rotating (G68.1/G69.1)
Three-dimensional coordinate conversion with B-axis rotating (G368/G369)

The question is how to implement it into the PP or replace G400 in the PP. I get the benefits of using G400. But i don't need this functionality, at least to get things running. On the long run of course it would be quite nice, cause this is one of the huge benefits of a mill turn. Since this G code works with the tool offsets automatically it should be used by the motion planner?!

But yes the touch off should be at  B0.


The following user(s) said Thank You: Aciera

Please Log in or Create an account to join the conversation.

More
1 year 5 months ago #327840 by jochen91
I thought a little bit about it and came to the conclusion, that most of the functionality of the Millturn would be covered with the following G-codes:

G68.1/G69.1
G368/G369
G400
G490 (I think, I could do that myself by replacing the G code with a custom M code in the PP)

Do you think you could support me on more time image missing /media/kunena/emoticons/smile.png?

Kind regards,
Jochen

Please Log in or Create an account to join the conversation.

More
1 year 5 months ago #327846 by Aciera
I'm still working on it.
Having the tool pointing in the x direction instead of the z direction in the home position has turned out to be a bit more of a headache as Linuxcnc applies the tool offsets internally.
TCP with xyz tool offset and tool spindle orientation is done. The kinematic for Tilted work plane also works but the transformation of the work offset still needs some work.

Let me figure this out first and I'll post a new sim config so you can have a look at it. Then we can have a look at customizing the gcodes for your specific needs.
 
 
The following user(s) said Thank You: besriworld, jochen91

Please Log in or Create an account to join the conversation.

More
1 year 5 months ago #327927 by Aciera
Could you export the example part from your post here as an stl file and post it here?
forum.linuxcnc.org/10-advanced-configura...hine?start=40#327741

Please Log in or Create an account to join the conversation.

Time to create page: 0.281 seconds
Powered by Kunena Forum
