


Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Quite sure .... think you use a little bit force for tensioning image missing /media/kunena/emoticons/cheerful.png ( think you have some power on your hand ) .... Seriously I have to congratulate you for the work you do here on the forum .... in these days to remind me of the work I left halfway through I followed back the posts of grotius, yours (your thanks have become synonymous with posts to follow for me) and udos .... for more I also found mine I work a year ago on a stick with peek written ..... until I saw the udos comments I didn't know what it was for ....I have some mounted on a non finished mill, HTD5,
Please Log in or Create an account to join the conversation.
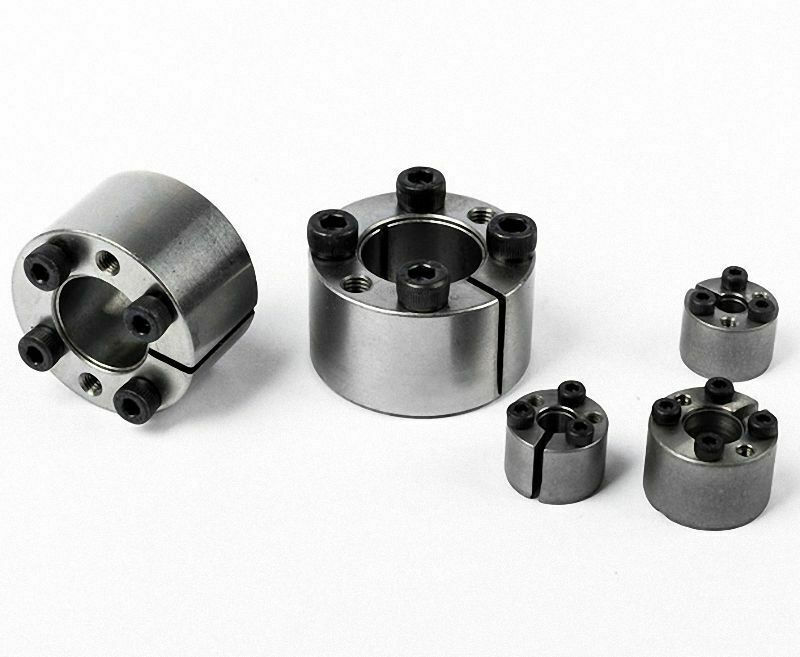
The AT profile is probably optimal; it's supposedly optimised for low/zero backlash. The question is what is most likely to cause problems on a mill: a taperlocked HTD pulley (possibly backlash from the HTD profile?) or a zero-backlash AT5 pulley attached using only a setscrew on a filed flat?
Edit: That is, if I could find AT5 pulleys with taperlock then I would get that, but alas...
Please Log in or Create an account to join the conversation.
Is the lack of taper-lock or QD bushing AT5 availability due to location?
Do you have a lathe available? If so, there are some fairly easy options available way better than a set screw.

I do not think it is from the type of pulley/belt, it is probably due to bad pulley or belt teeth.
I have some mounted on a non finished mill, HTD5, no backlash at all. But i am using belts and pulleys yanked out of old machines.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
