Spindle orient PID tuning [re-solved, yay]

More
4 years 4 months ago #245440 by mgm
Ralph:
Yes the bt30 is only to be aligned for depositing into the carusell. If the two notches are not in insertion direction then the holders do not clamp properly.
In principle, it should then be something like you have done now.
The positioning would then have to be made on the bt30 holder.

Thanks for the inspiration 

Michael


Please Log in or Create an account to join the conversation.

More
4 years 4 months ago #245441 by spumco
If you're using a high-speed router spindle with smallish diameter tools, I'd be inclined to remove the drive dogs and not worry about spindle orientation.  I suspect that's why many of the ATC spindles with built-in motors I've seen are ISO30 and not BT30.

On the other hand, if you intend to put a big face mill in it to flatten the panels then the drive dogs are probably a very good insurance policy. 

Spinning a holder in the taper can make an expensive mess.

So... what is driving your spindle, and what's the slowest it can rotate?

Please Log in or Create an account to join the conversation.
More
4 years 4 months ago #245442 by mgm
No eBay APP ID and/or Cert ID defined in Kunena configurationThe diameter of my tools is between 4 and 30 mm.
I had decided for the BT30, because they are cheaper than the ISO 30. It was only important to me that I have ER32, because in the carpenters many end mills, or diamond cutters have a 20 mm shank.
I was not aware at the time of purchase that there would be a problem, because the spindle has no holder for BT30!

I already have BT30 holder and the retaining clips.
I have not yet bought an ATC spindle, because I was not yet sure.
But I wanted to buy this kind.


The spindle is controlled with an inverter.
I can have my current spindle rotate from 0-18000 and programmable inputs and outputs the inverter also has.

This is the inverter
www.sourcetronic.com/shop/de/frequenzumr...00-230v.html#256=225

Please Log in or Create an account to join the conversation.

More
4 years 4 months ago #245445 by spumco
The Rattm ATC spindle is advertised as "BT30" on ebay and aliexpress, but...

It's not BT30.  It's ISO30 - same taper, but without the drive dogs.  All the photos show a spindle that's missing the drive dogs, plus I found this on the aliexpress page:


Note the highlighted area.  I think some of the Chinese vendors play a little fast & loose with BT vs ISO designations.  The tapers are interchangable, so who cares, right?image missing /media/kunena/emoticons/ermm.png

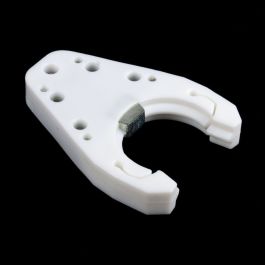
If you do a search for "BT30 Tool Fork" you'll find dozens of plastic forks from China that don't have alignment tabs built in.  Some have a provision for tabs, but very, very few of them come with tabs.  They're all really meant for ISO30 or (BT30 with no spindle drive dogs).

About the only ones that do have tabs - i.e. required for an actual BT30 spindle - are the metal ones intended for Robodrills or similar VMCs - not routers.  The one exception I've found are the Tormach 1100MX holders - those are plastic but have molded-in metal alignment tabs.


There is an actual difference between ISO30 and BT30 holders besides the slots; I think the tool fork groove is different - maybe different diameter or angle or something.  Not sure, TBH.

If you get that ebay spindle you don't need to worry about orienting the spindle.  Your holders may have drive dog slots, but the spindle doesn't need to be lined up with them and your ATC forks wont need alignment tabs.

Please Log in or Create an account to join the conversation.

More
4 years 4 months ago #245475 by mgm
Hello Ralph,

Thank you for looking at this!
 

Please Log in or Create an account to join the conversation.

More
4 years 4 months ago #245506 by spumco

And another thing...

I just noticed it's not going to the same orient location each time I start up the machine.  I spent quite some time fiddling with the INI orient_offset a couple days ago to get it perfectly lined up with the carousel pockets, and the 'completed' orient cycle today (attached) wound up about 60 degrees off from the last time I had the machine running.


Sadly, this is still a problem.

Orient does not go to the same place every startup.  The testing I did with the new shotpin worked great... but I'd already run orient without it that session.

I can't tell if LCNC is ignoring the index signal at the start of orient, or my various settings are wrong.

I won't post my silly hal file again, but here are the values I think may be relevant:

(INI file)
ORIENT_OFFSET = 0.328
ENCODER_SCALE = 4096

(HAL)
orient.0.tolerance              1.0
encoder.00.counter-mode   0
encoder.00.filter                 1
encoder.00.index-invert       0
encoder.00.index-mask       0
encoder.00.index-mask-invert   0

net spindle-index-enable encoder.00.index-enable spindle.0.index-enable

Is the orient tolerance way off? I though I read it's in degrees... but if it's in some strange unit that might explain why ORIENT_OFFSET needed to be that odd 0.328 to get things lined up with the ATC pockets.

Anyone want to take a stab at this?

Please Log in or Create an account to join the conversation.

Time to create page: 0.188 seconds
Powered by Kunena Forum
