Retrofit of Precix 5x10 CNC

More
5 years 7 months ago #202103 by jmelson
Replied by jmelson on topic Retrofit of Precix 5x10 CNC
What type of motors and drives are you using? Do you have position feedback to the PC? If so, move the machine manually and watch the DRO to see if the position changes smoothly and the correct amount. If not, then the encoder or anything in the chain back to the PC is suspect.

If you don't have position feedback to the PC, it is a little harder to diagnose. If the drives have a programming port you might be able to run diagnostics on the drive and see if it shows an issue or error.

Jon

Please Log in or Create an account to join the conversation.

More
5 years 7 months ago #202107 by jmelson
Replied by jmelson on topic Retrofit of Precix 5x10 CNC
OK, I gather you are using the original Copley and AMC analog servo amps. Are you using tachometers in the motors for velocity servo mode, or are you using them in torque mode (no tachs)? If you are using the tachs, it is possible the tach or tach cable has gone bad. That will definitely cause a jump if the amp doesn't see the tach showing velocity when it starts to command movement.

If you are running the amps in torque mode (no tachs) then it probably is an encoder feedback issue, or possibly a failure in the servo amp. Since you have the Mesa interface, you do have position feedback to the PC, so check the DRO as described in the previous message. You can also use Halscope to display encoder velocity and the PID command out to see which is causing the jump.

Jon

Please Log in or Create an account to join the conversation.
More
5 years 7 months ago #202123 by randypetersen
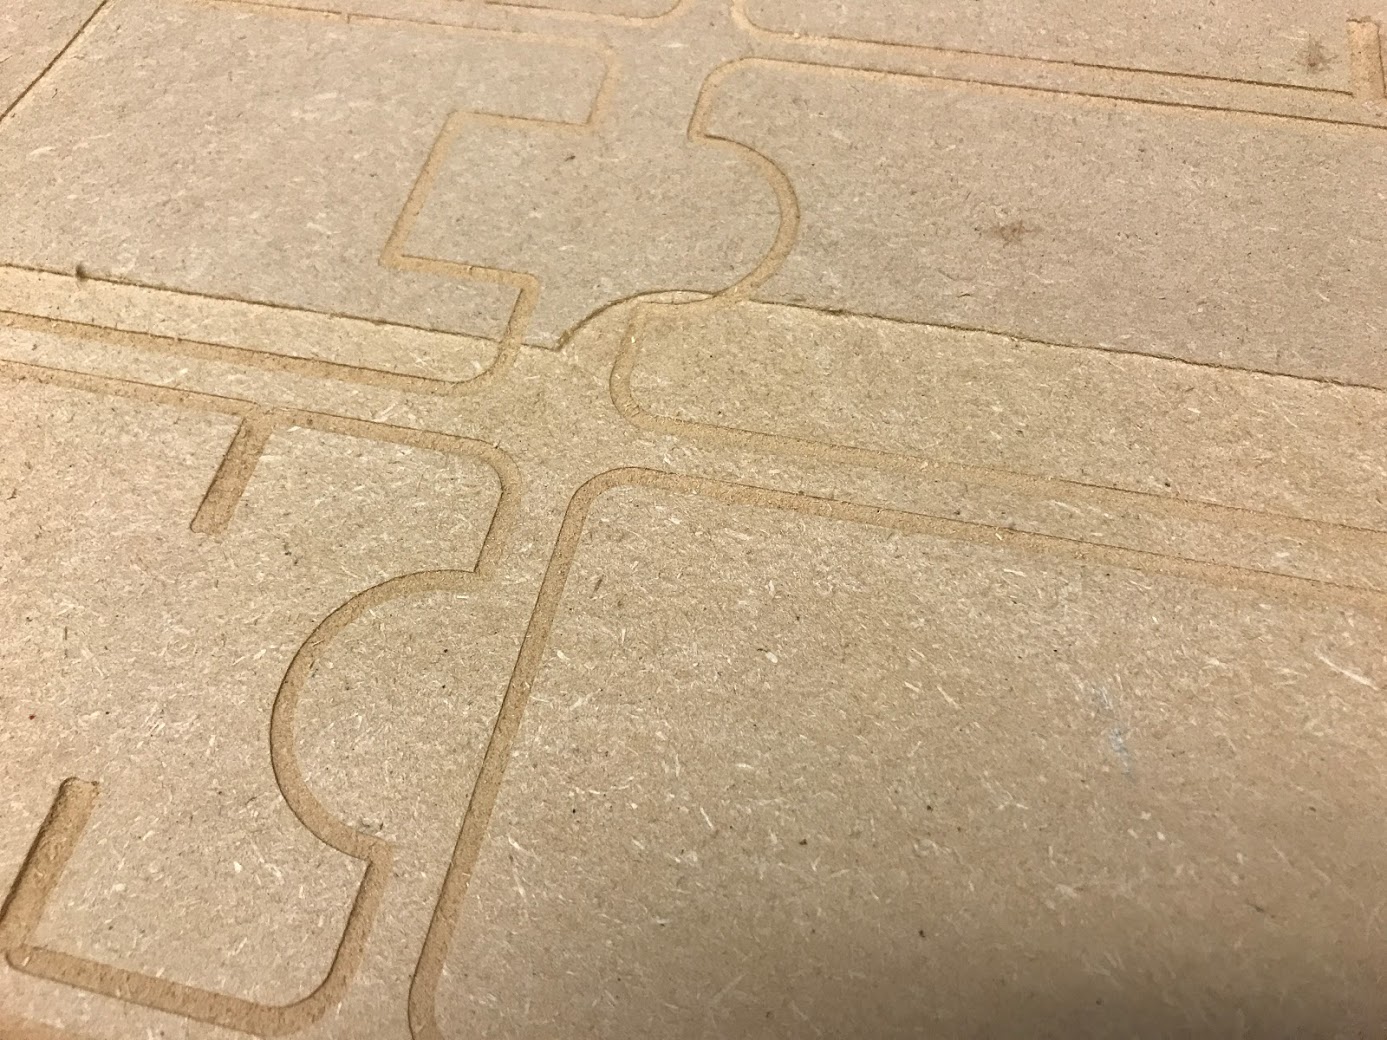
I remember reading something about these PRECIX controllers need a change of capacitors in the power supply. Since my machine is 20yrs old, figured it was time. I had thought about changing them out and/or getting a new power supply at one point. I haven't since it was working fine. Today I got a following error, so I am looking at my servo tuning. Happened while I was resurfacing my spoilboard, and about 25% through I got a following error. Just shuttered and errored out. Didn't hit anything... just taking 0.05" off spoilboard with very little load on spindle.

Please Log in or Create an account to join the conversation.

More
5 years 7 months ago - 5 years 7 months ago #202167 by randypetersen
Since I have brand new encoder cables I am thinking it's the motor or tuning. Odd since this machine was behaving up until today. This motor is pretty ancient. It could be the power supply failing I suppose.

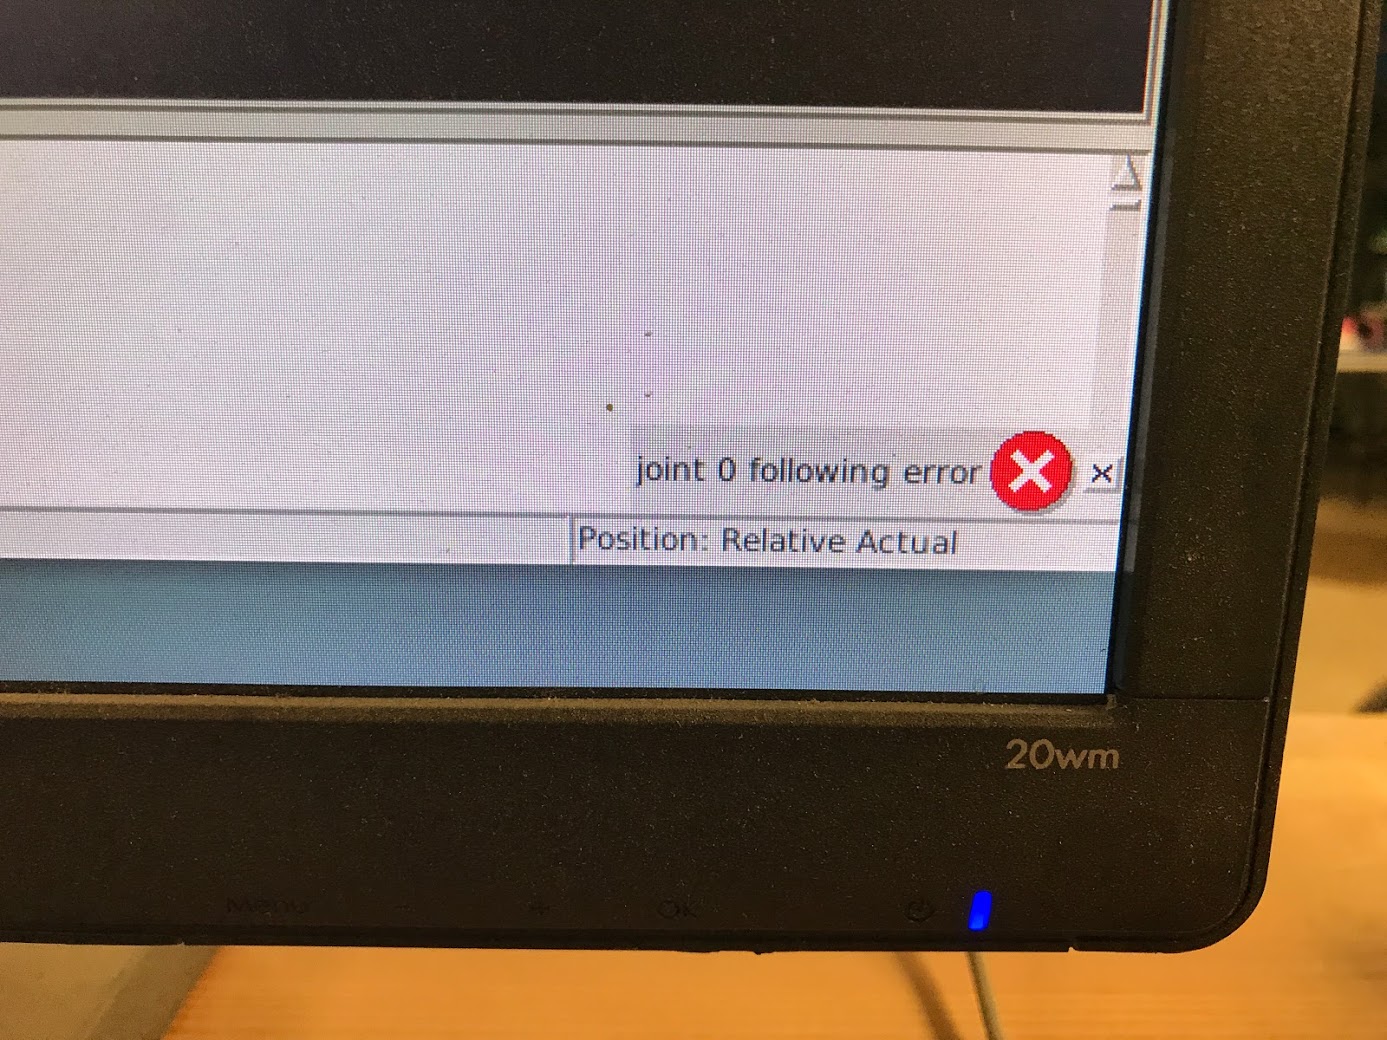
Anyone have any input on why I'd be getting joint 0 following errors all of a sudden?

Debating on getting 3 new NEMA 34 servos/driver/power supplies, one for each axis. Looks like you can get a set for around $800. Wefixprecix had motor/encoder assembly for $550.00 a year ago, not sure if he still has any available.

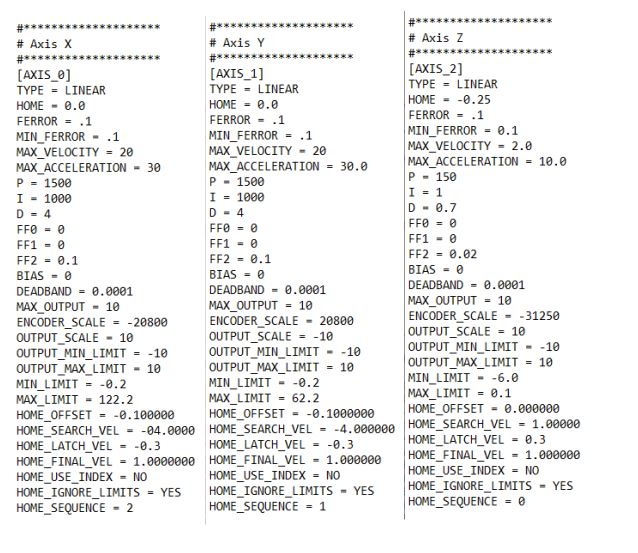
I notice my PID numbers look way off compared to most posts where I read about PID tuning for SERVO motors.

Think I need to start from scratch. Odd I haven't touched my setting in months. Although the last thing I did to was lower the ferror, I was told it was too high.

error, which I am sure everyone has seen :)


where it stopped the 1st time, 2nd time didn't get even that far..


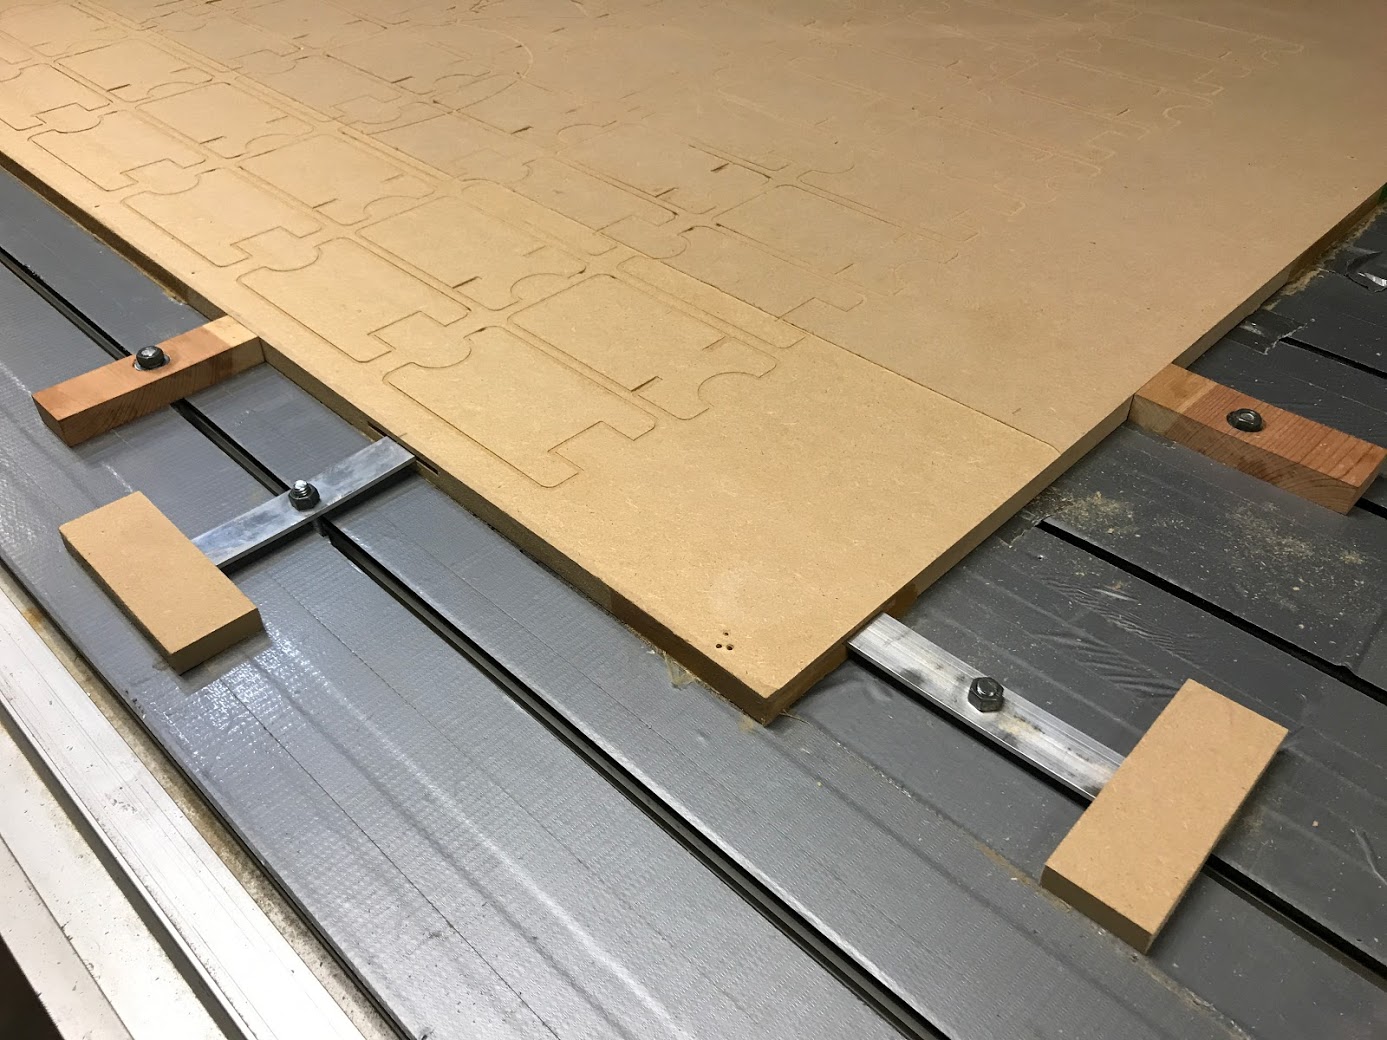
my crappy way of holding down my spoilboard - biscuit slots & aluminum flat stock holding it down to table/t-track


Thanks for any input!
Last edit: 5 years 7 months ago by randypetersen.

Please Log in or Create an account to join the conversation.
More
5 years 7 months ago #202171 by jmelson
Replied by jmelson on topic Retrofit of Precix 5x10 CNC
Are these settings AFTER you reduced the error limits? Are you running with inch units or mm? If inches, then 0.1 is allowing an errot tolerance of 1/10 of an inch, which is a lot. On X and Y, that is 2080 encoder counts. You need to fire up Halscope and see what the actual error is, and what it looks like in the time domain. If your amps are running out of headroom, you will see a slowly accumulating error. If there is a bad connection (cables, worn brushes, etc.) then there will be a sudden increase in error.

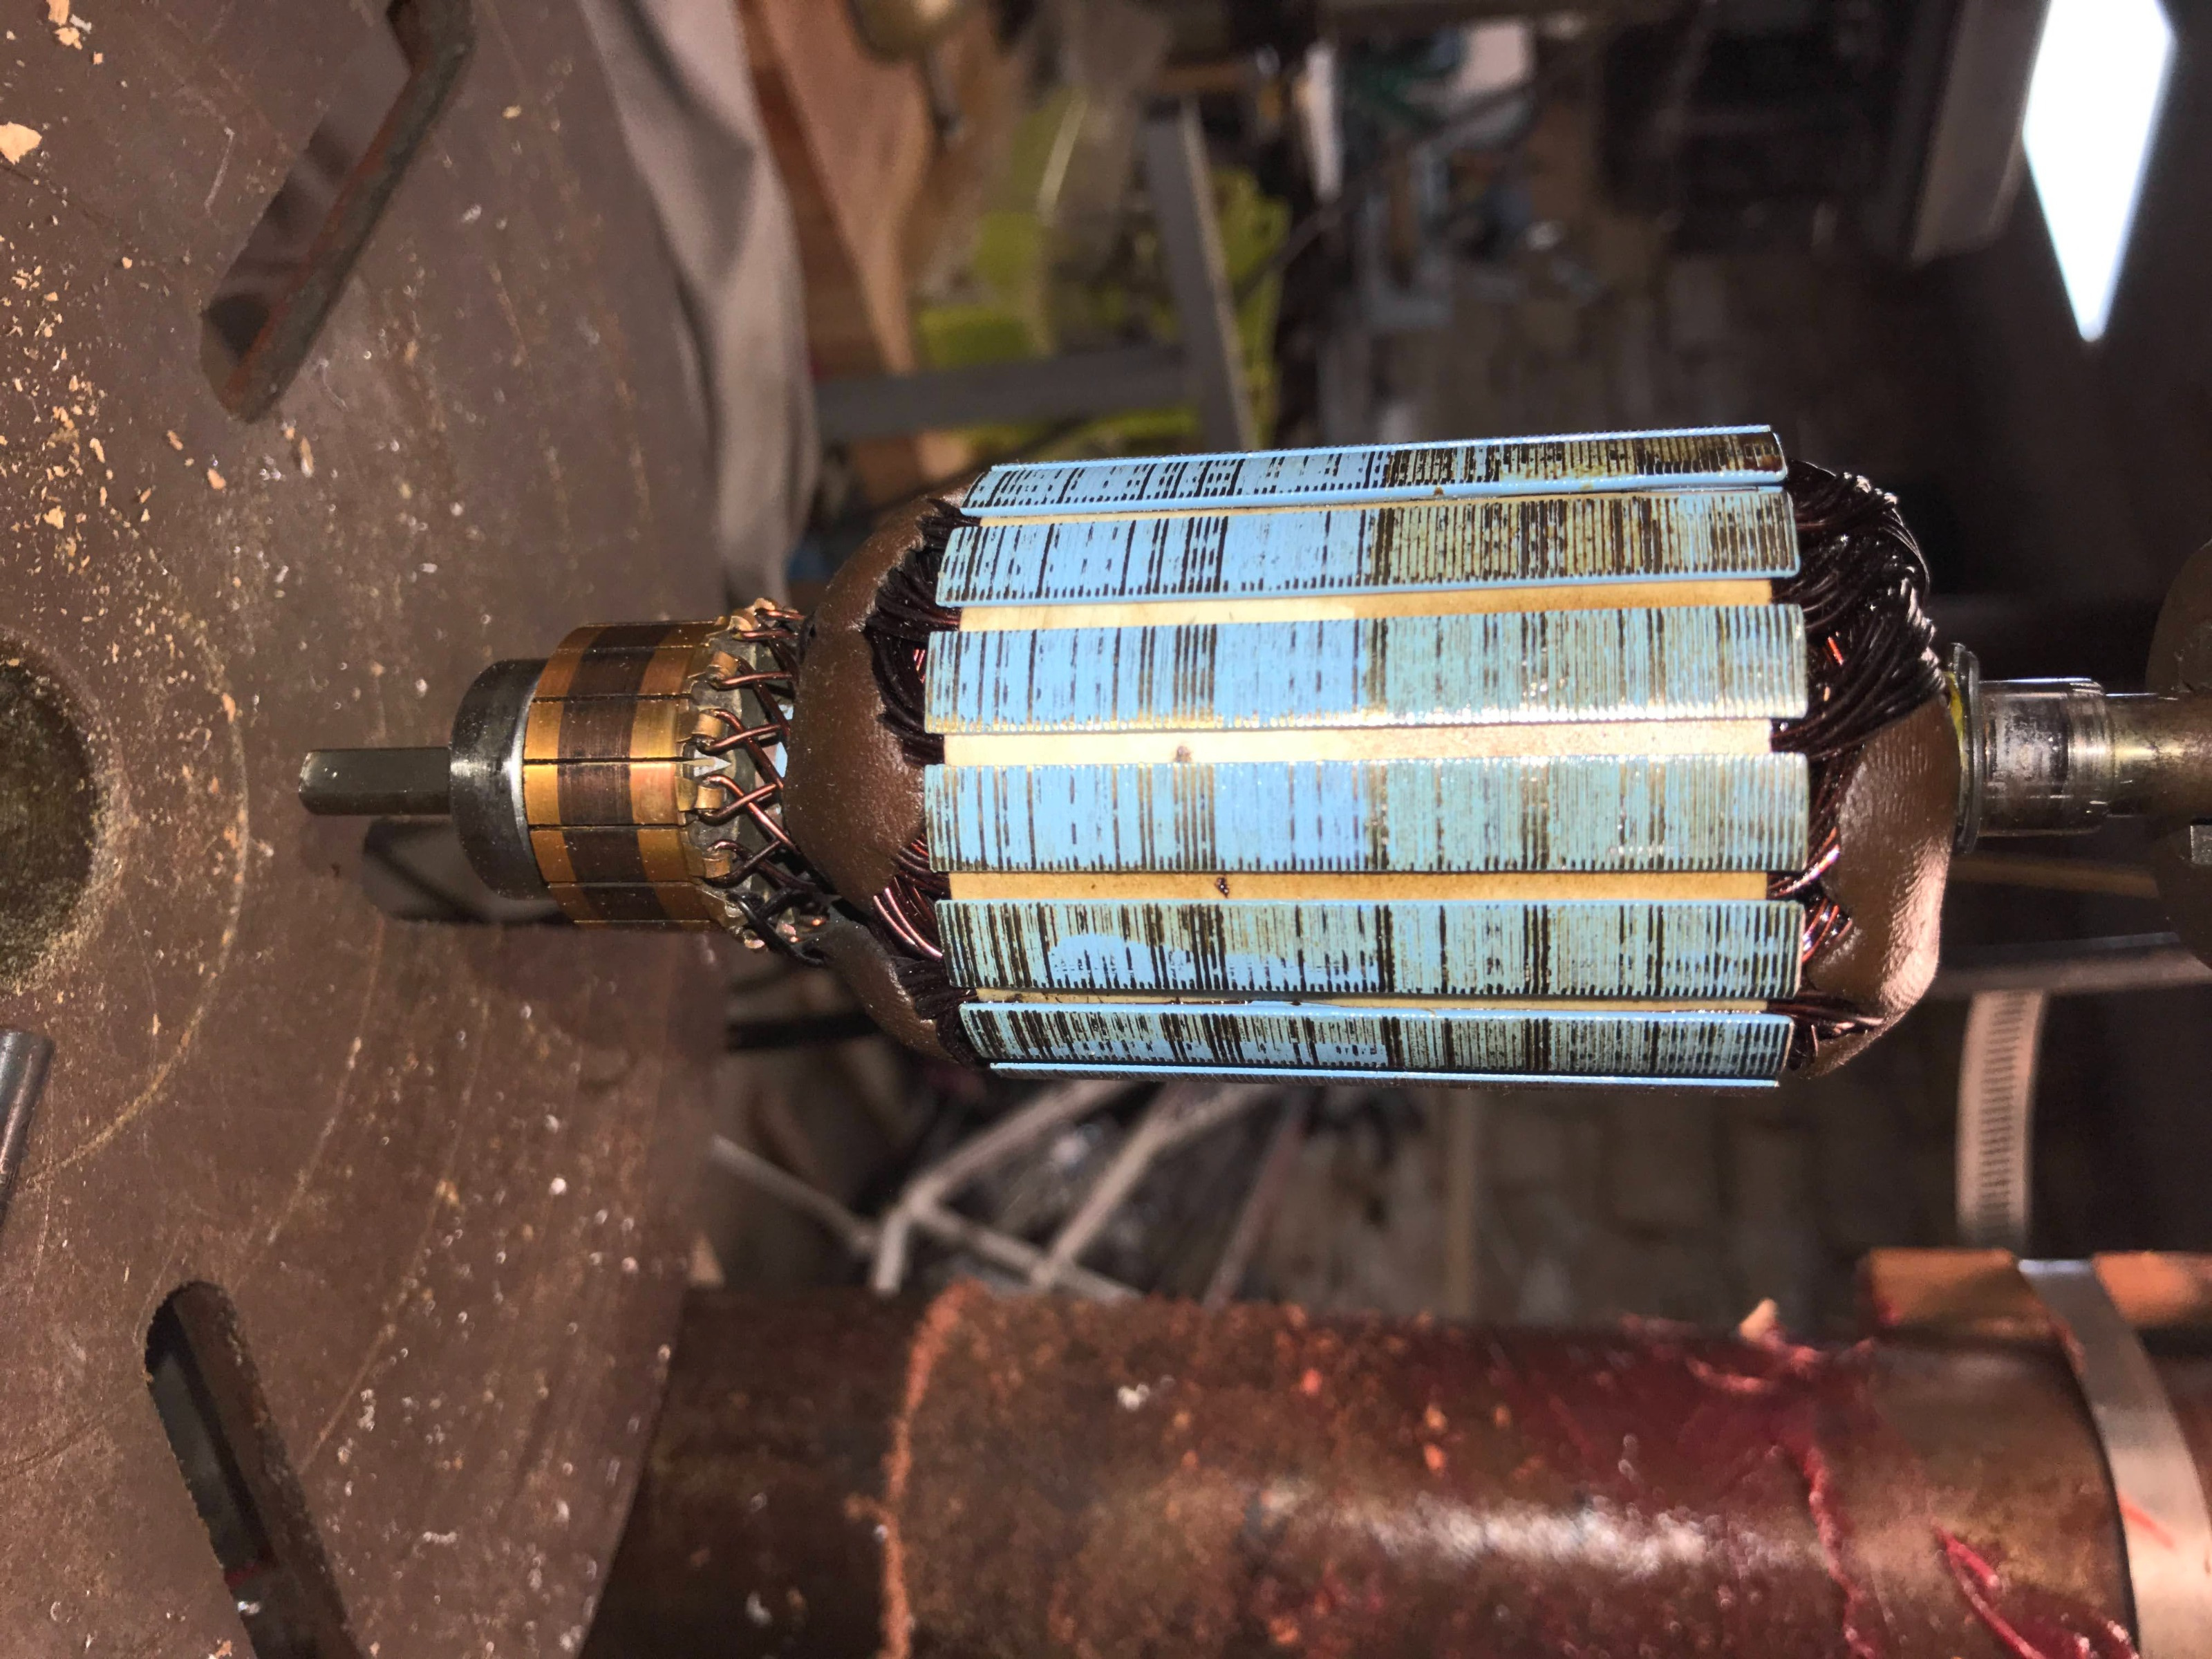
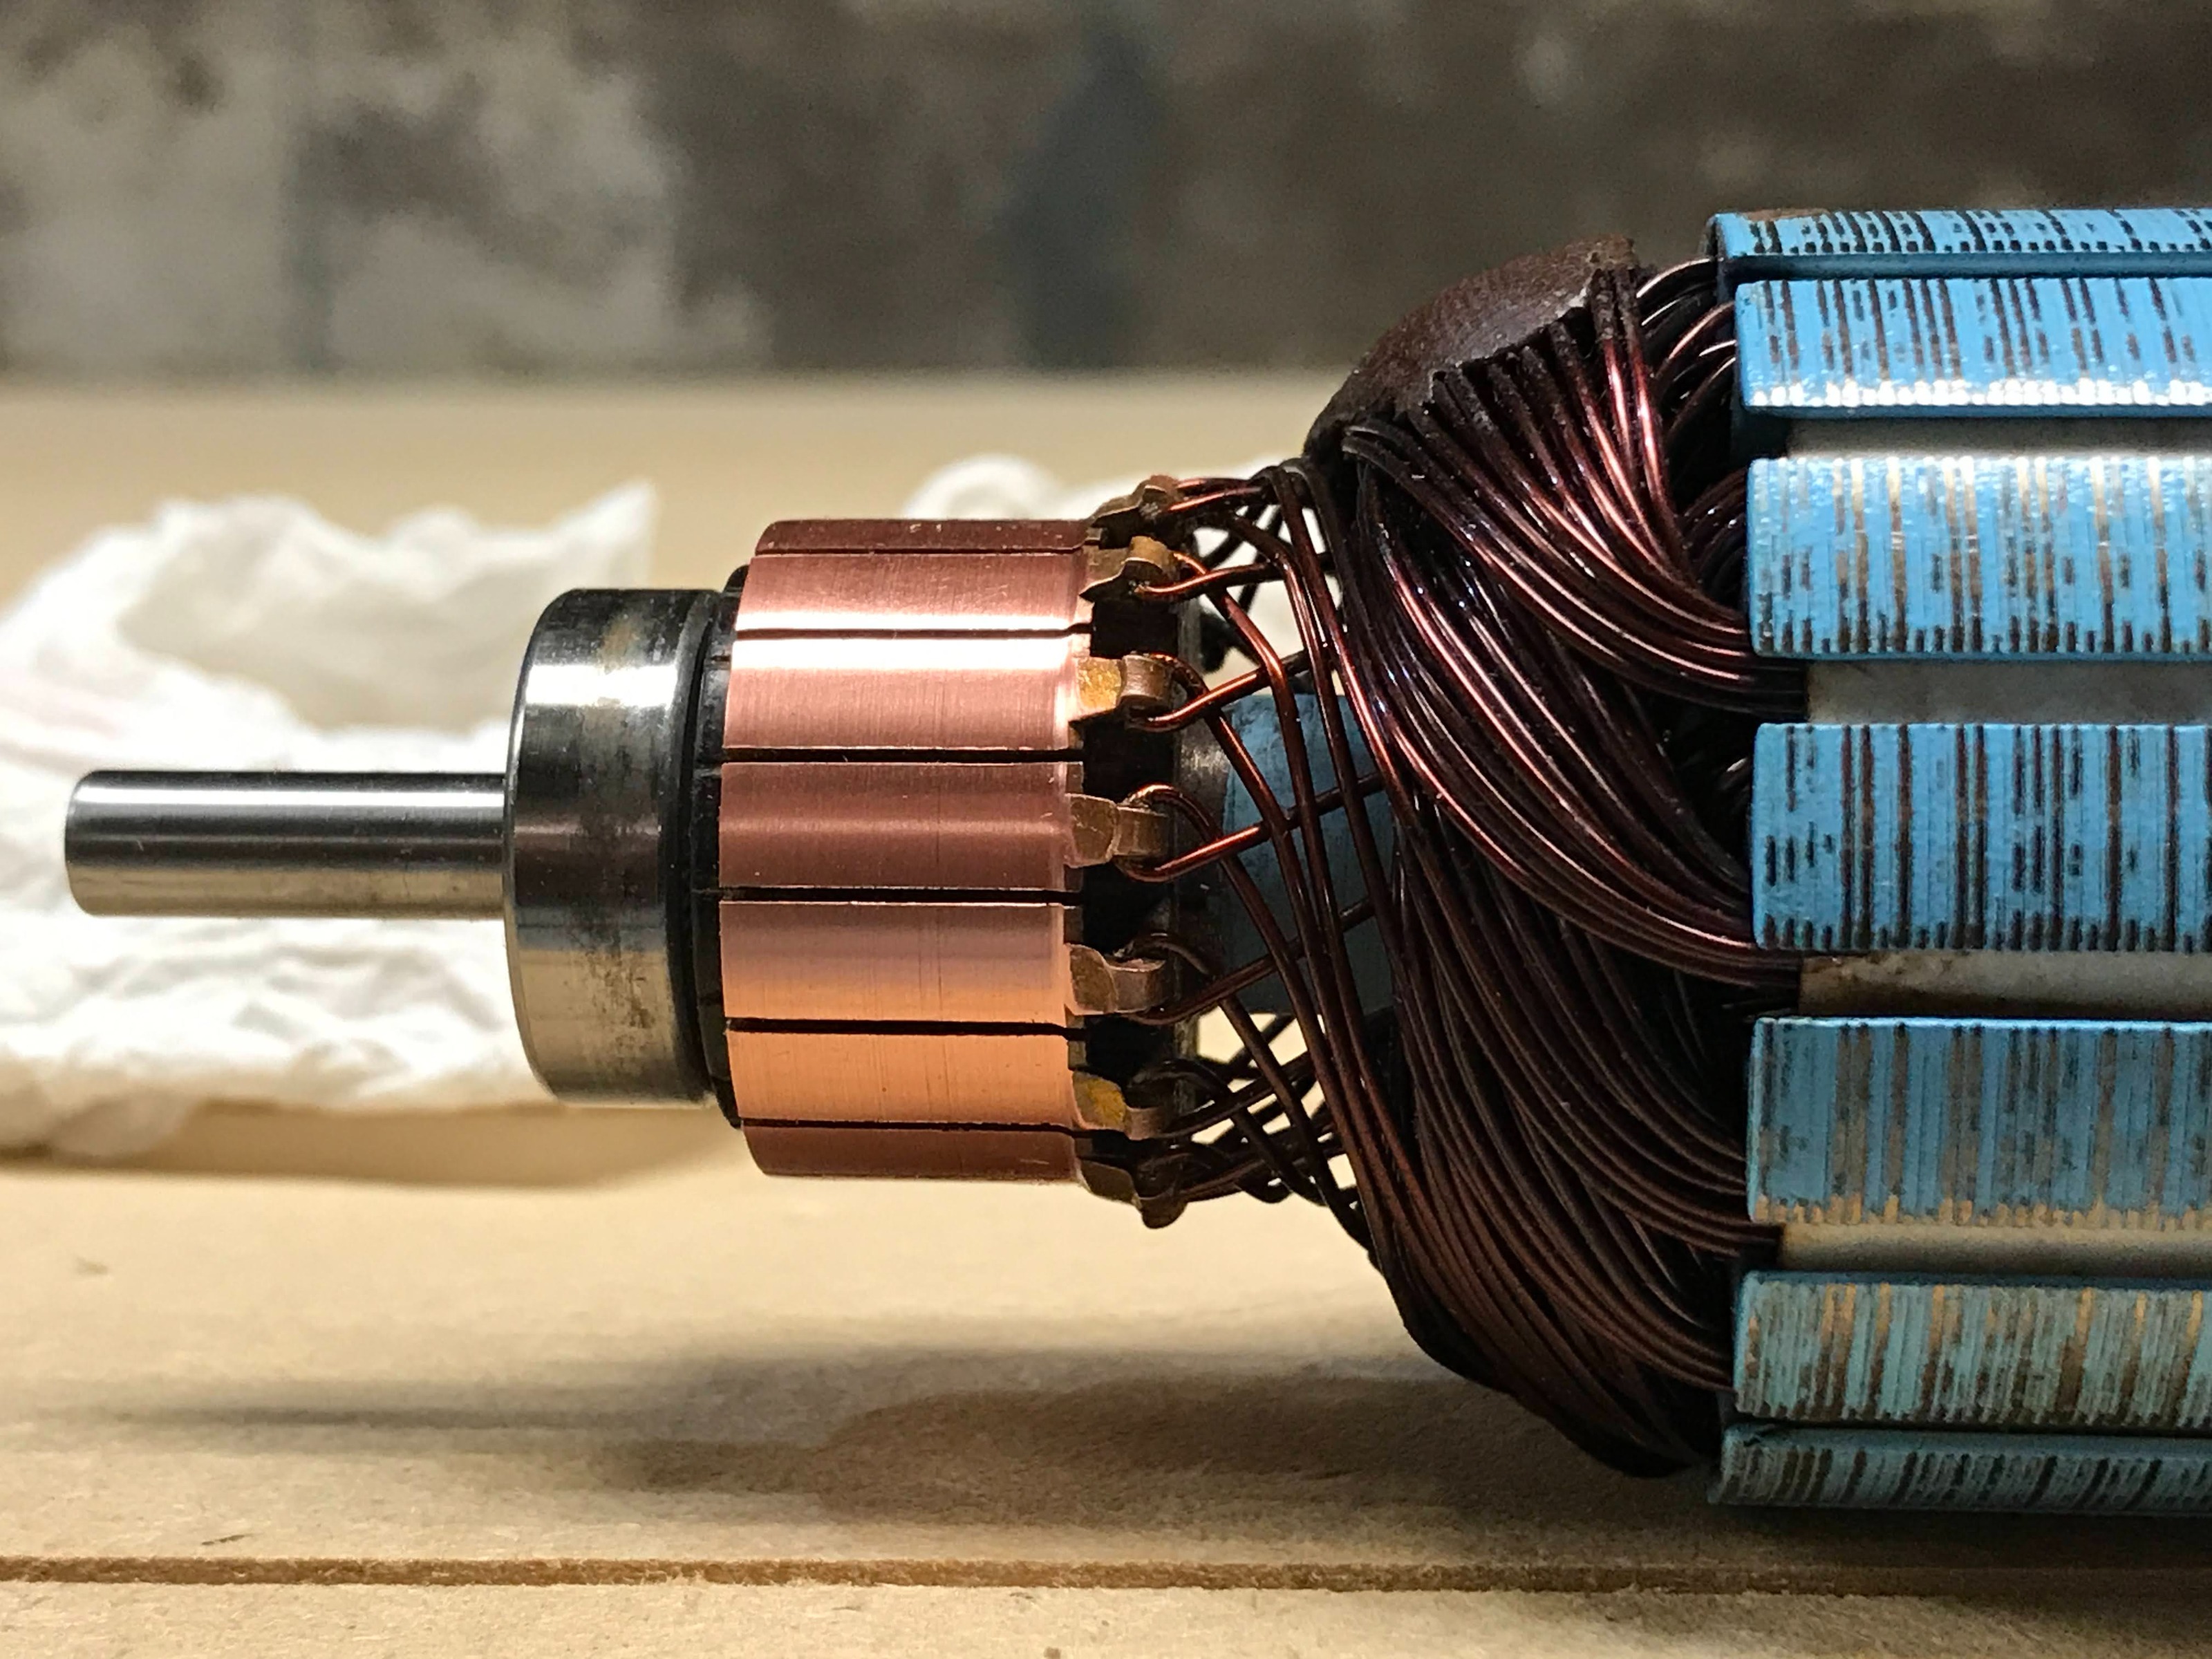
I'd pull the brushes out of the suspect motor and inspect the commutator. Either brushes or commutator could have developed wear, or the commutator slots are filled with copper dust, shorting out the armature.

Jon

Please Log in or Create an account to join the conversation.
More
5 years 7 months ago #202289 by randypetersen
Thanks jmelson!

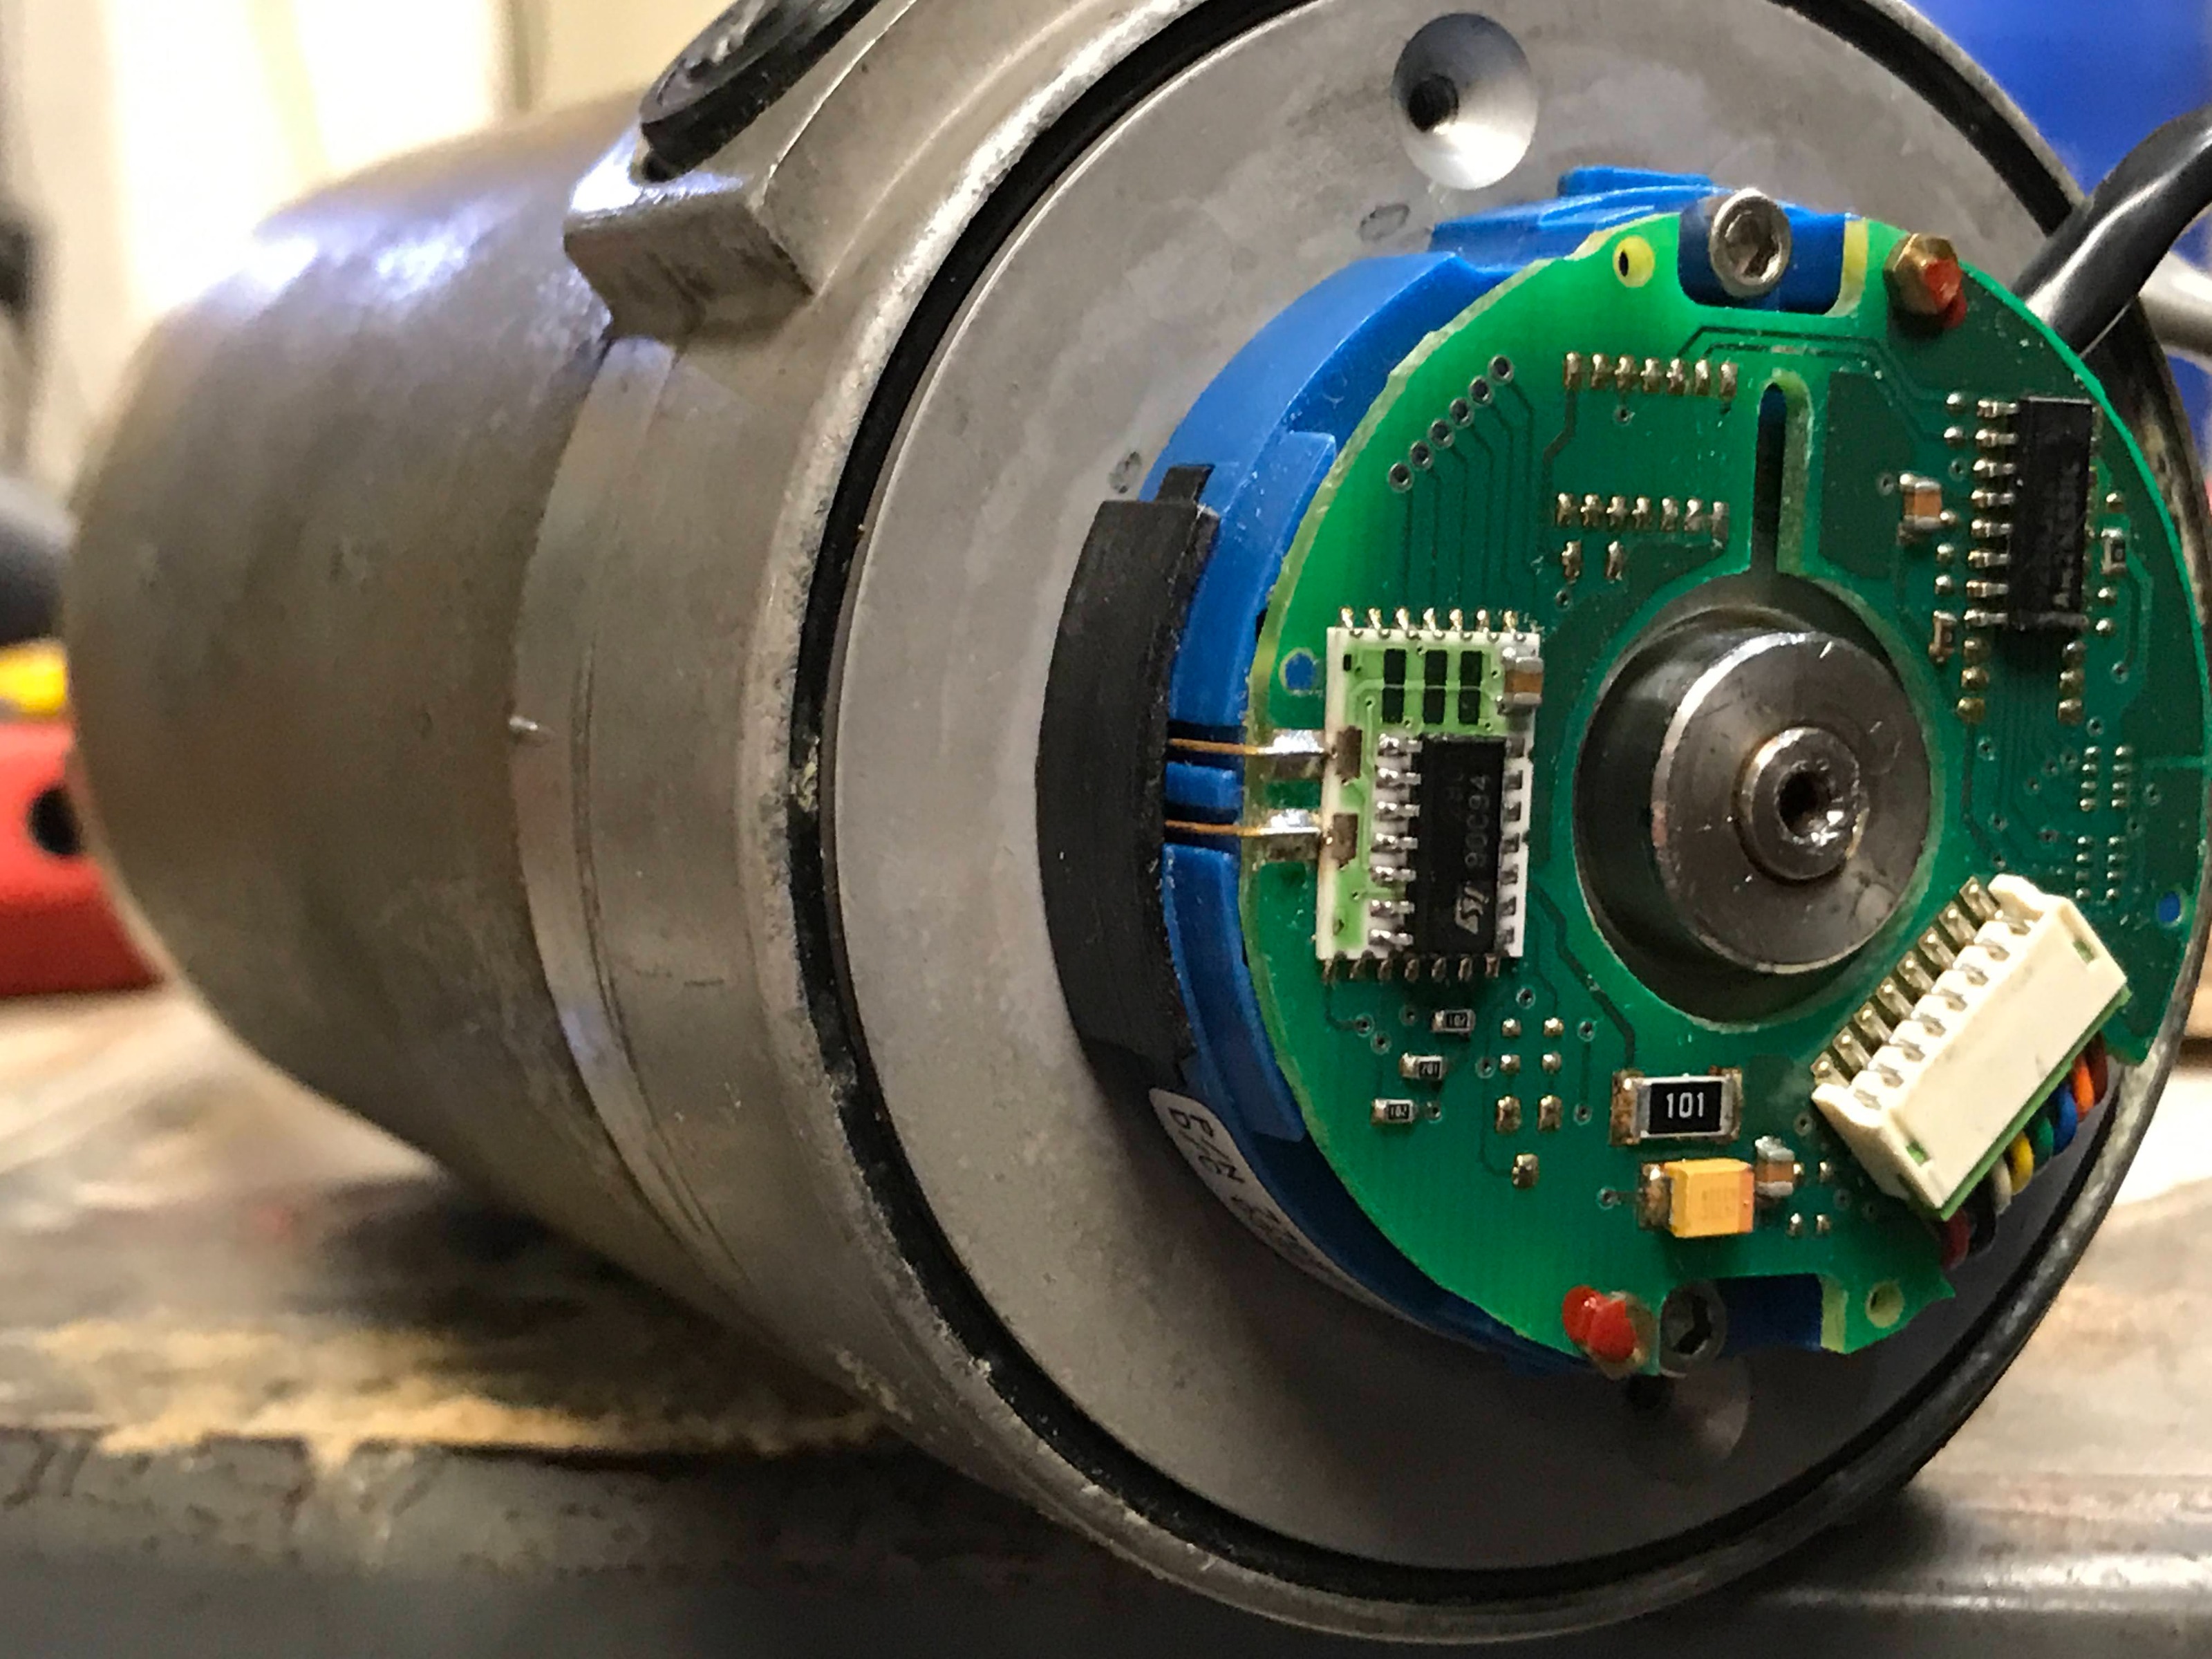
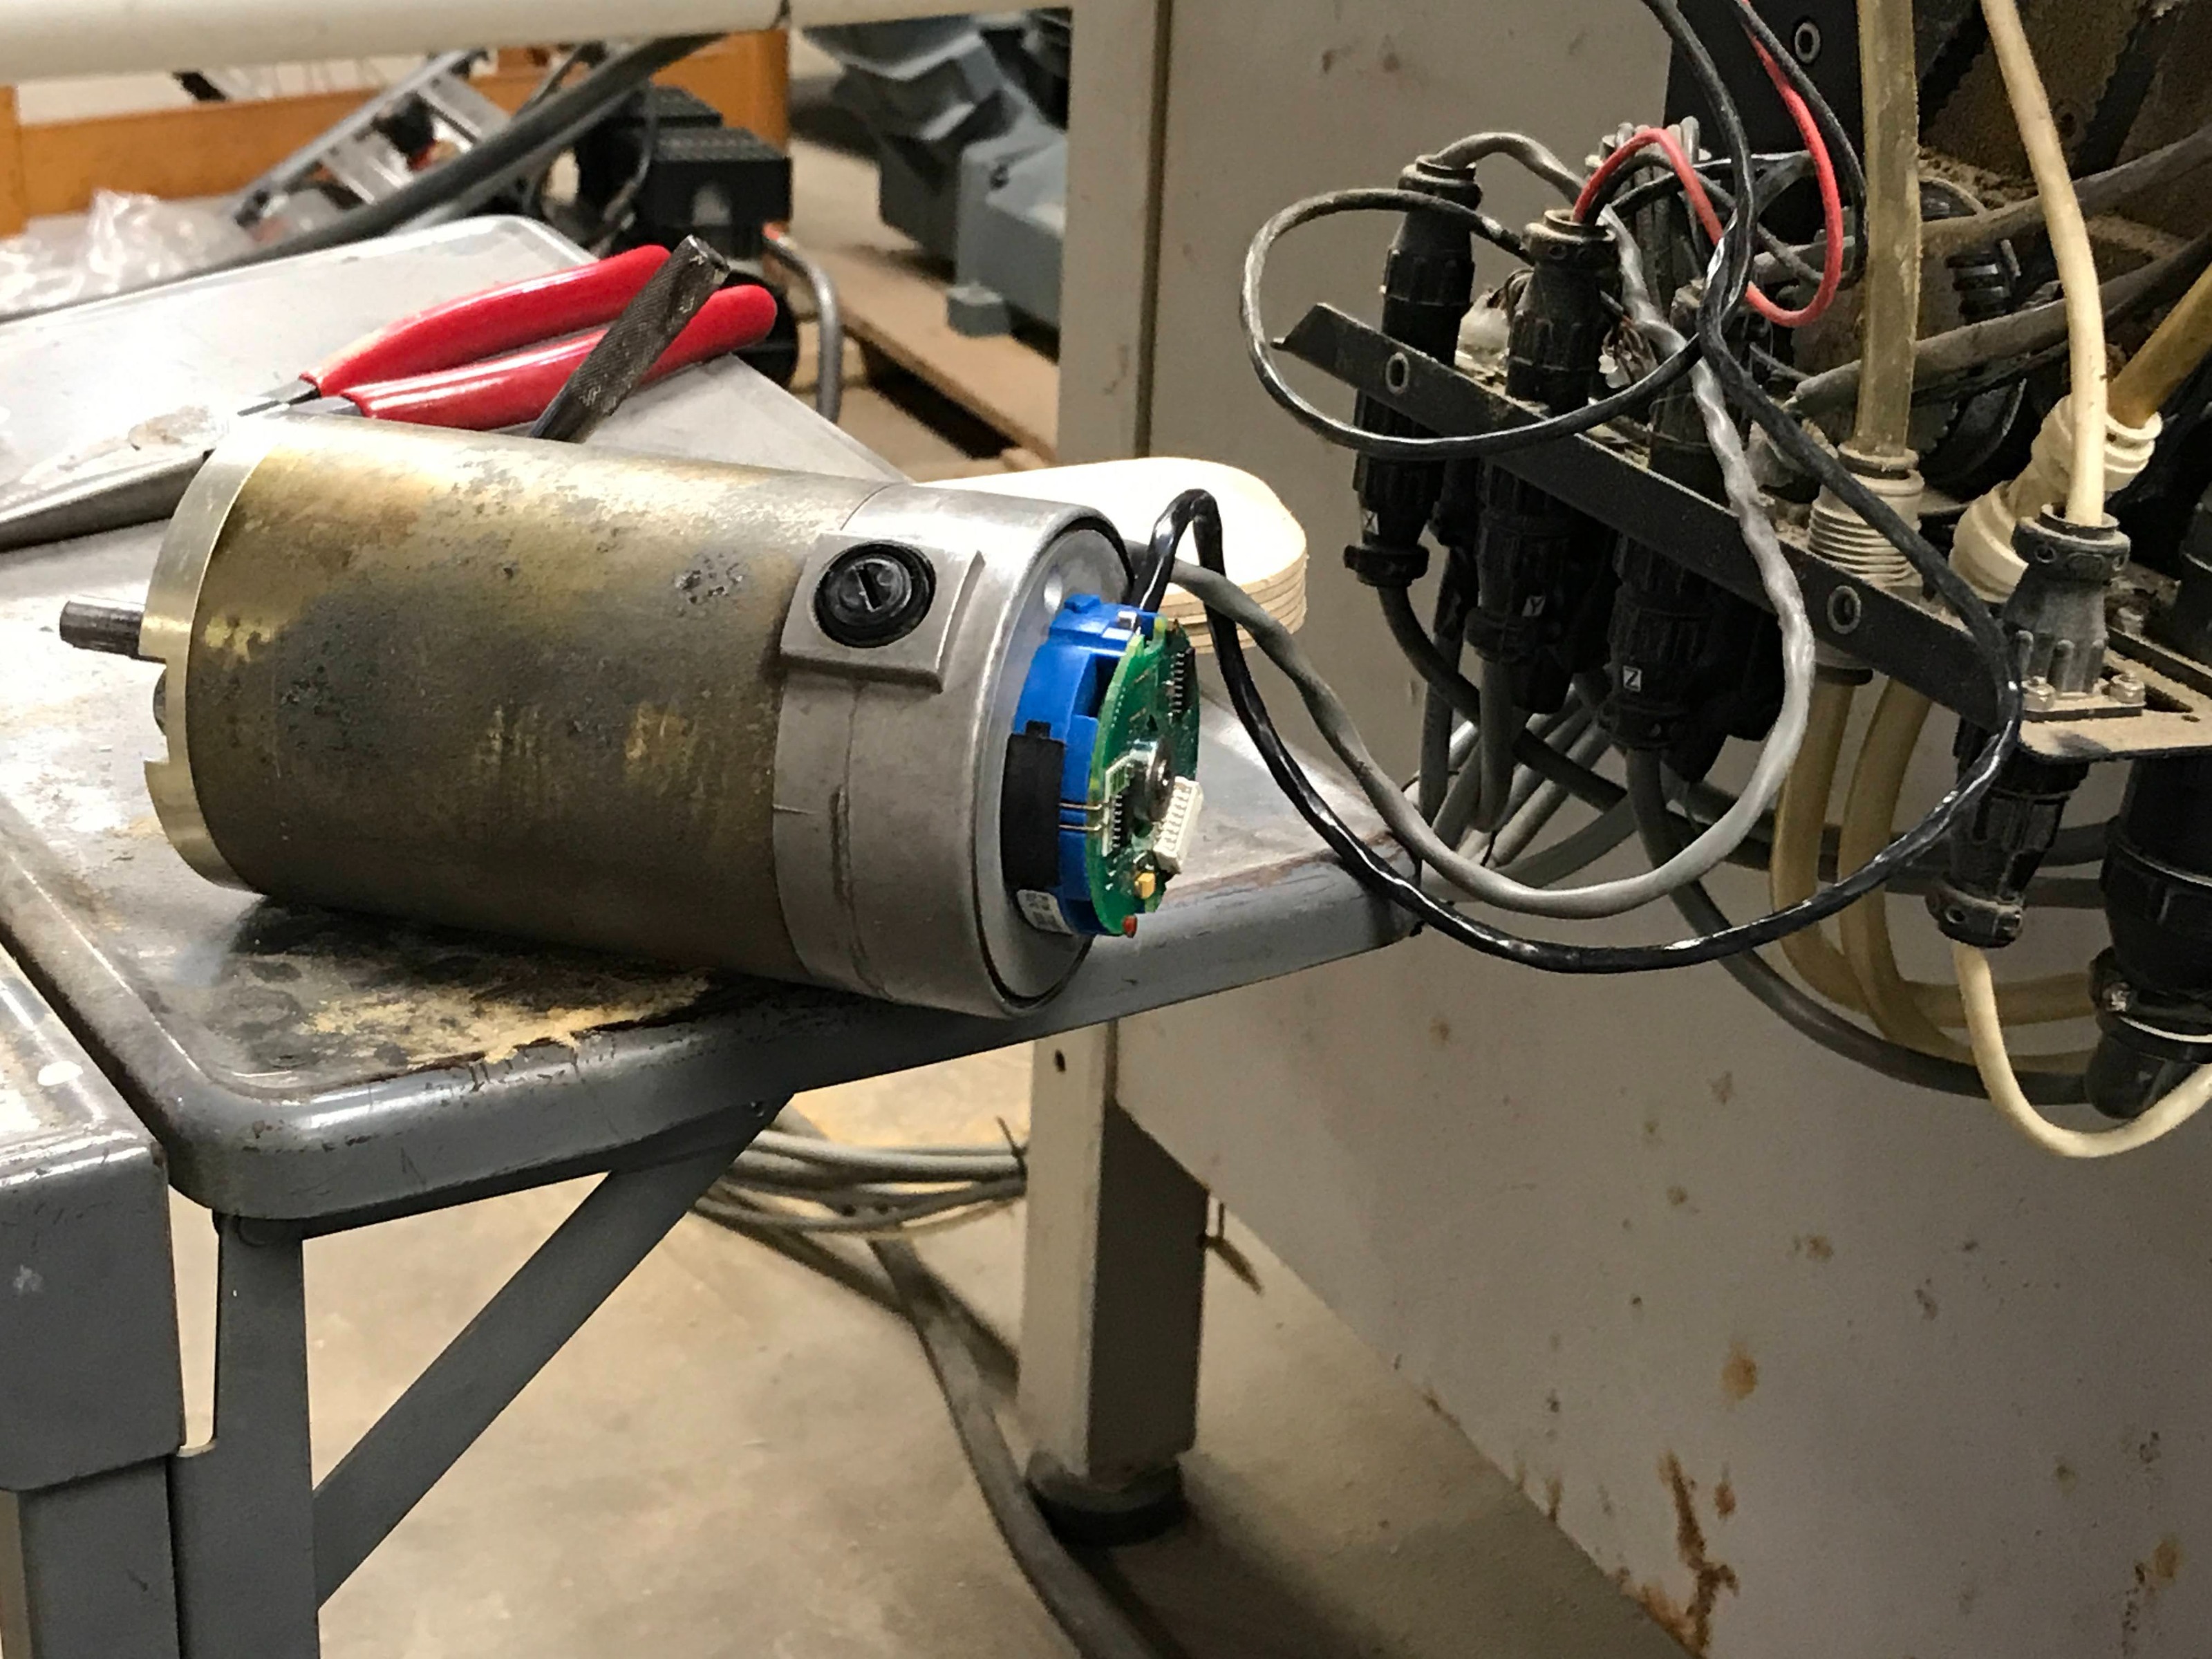
I took the servo motor apart.


Cleaned it up, but it didn't look terrible.


Putting it back together and the encoder was really hit and miss.


Then I moved the stop just a tiny amount and it was behaving much better. The encoder does seem somewhat sensitive.


I think this unit started off with some older motors, and the Y and Z axis were replaced with the magmotor units. I am thinking I could either replace the X with a magmotor or replace all the motors with some more modern units.

I have yet to connect the motor with the gears yet, hoping to test it a bit more.

Thanks again for the help!

Please Log in or Create an account to join the conversation.
Moderators: PCW, jmelson
Time to create page: 0.127 seconds
Powered by Kunena Forum