

- Posts: 5
- Thank you received: 0
Newbie question
8 years 7 months ago #107722
by schaet
Newbie question was created by schaet
Hello,
I am a total newbie here feeling my through. I tried running my first program and got the following error:
"Cannot feed with zero spindle speed in feed per rev mode"
Can anyone shed some light on this? I'm sure it's a simple setting I have wrong
Attached is my g-code
Thank you
Steven
My setup:
Sherline 5400 CNC
LinuxCNC
BobCAD/CAM with the Sherline post processor
I am a total newbie here feeling my through. I tried running my first program and got the following error:
"Cannot feed with zero spindle speed in feed per rev mode"
Can anyone shed some light on this? I'm sure it's a simple setting I have wrong
Attached is my g-code
Thank you
Steven
My setup:
Sherline 5400 CNC
LinuxCNC
BobCAD/CAM with the Sherline post processor
Please Log in or Create an account to join the conversation.

8 years 7 months ago - 8 years 7 months ago #107725
by DanMN
Replied by DanMN on topic Newbie question
I'm presuming you start your spindle manually, i.e., not via gcode -- since you only have M0 specified -- which is spindle stop. In essence, the you are instructing the machine to plunge cutter that isn't spinning. Obviously, in systems that have spindle control automated this would be a big no-no.
Try adding an M3 statement here:
(MSG, " Spindle Speed 1191")
(M0)
M3 S1 F1
Touch off your Z well above your table or workpiece for a dry run. Let the spindle cut some air while you observe the behavior and become comfortable with the new instructions. I always test creative new ideas with my hand on the e-stop button
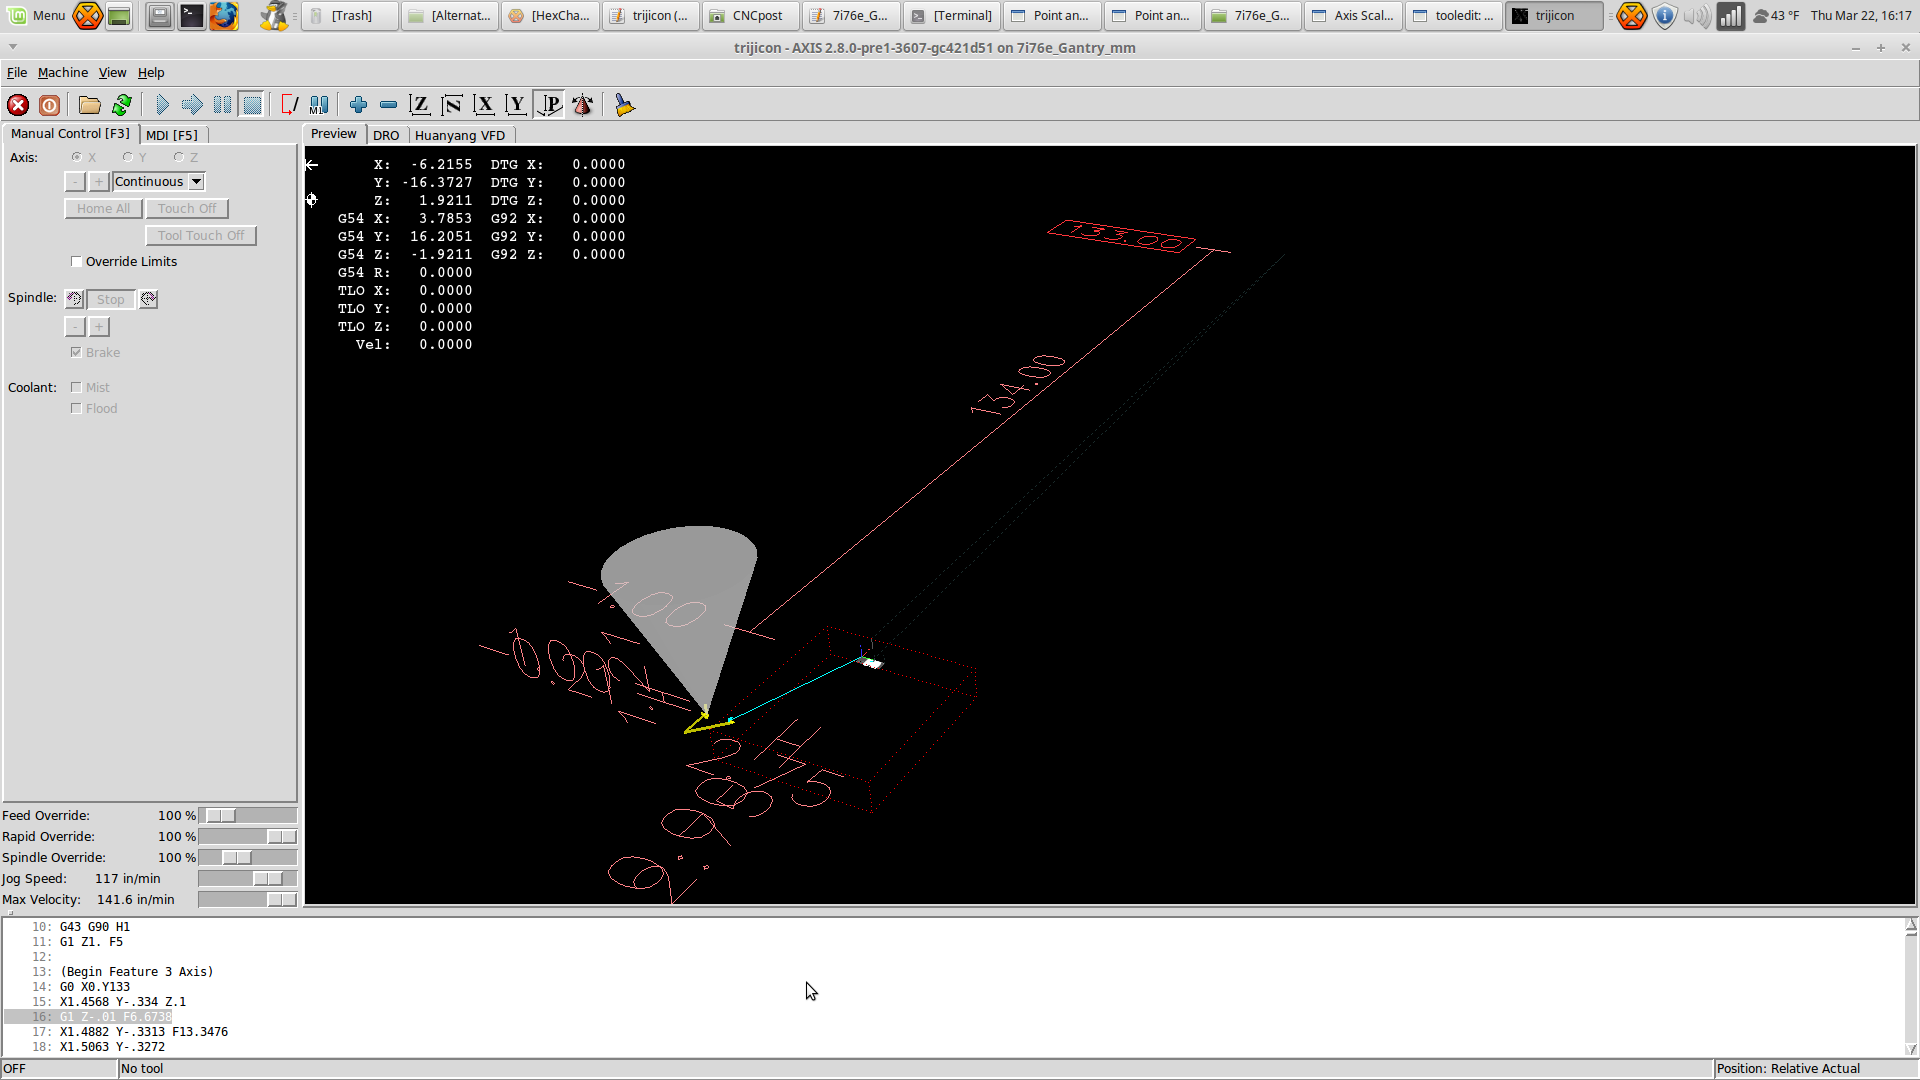
PS: I just modified and loaded your file, and you have other problems -- namely that line 11 command being a country mile long and obviously weird. I changed the Y value to 133 and it loaded, but with some expected problems with scale. It looks like you're cutting a postage stamp size object on a billiard table -- so, you've got some CAM setup issues to work out as well.
Try adding an M3 statement here:
(MSG, " Spindle Speed 1191")
(M0)
M3 S1 F1
Touch off your Z well above your table or workpiece for a dry run. Let the spindle cut some air while you observe the behavior and become comfortable with the new instructions. I always test creative new ideas with my hand on the e-stop button
PS: I just modified and loaded your file, and you have other problems -- namely that line 11 command being a country mile long and obviously weird. I changed the Y value to 133 and it loaded, but with some expected problems with scale. It looks like you're cutting a postage stamp size object on a billiard table -- so, you've got some CAM setup issues to work out as well.
Last edit: 8 years 7 months ago by DanMN. Reason: Added observation..
Please Log in or Create an account to join the conversation.
8 years 7 months ago #107730
by schaet
Replied by schaet on topic Newbie question
DanMN,
Thanks for the info. I'll check it out when I get home tonight.
Any ideas what to look for with the CAM setup? Maybe I'll re-create the job and do a stare and compare with the two posts.
Also, what was it that you saw that showed you that the scale was off?
Thanks again!
Thanks for the info. I'll check it out when I get home tonight.
Any ideas what to look for with the CAM setup? Maybe I'll re-create the job and do a stare and compare with the two posts.
Also, what was it that you saw that showed you that the scale was off?
Thanks again!
Please Log in or Create an account to join the conversation.
8 years 7 months ago #107738
by DanMN
Replied by DanMN on topic Newbie question
My comment on the scale was due to this picture -- notice your part is that tiny tool path in white, and for some reason your are getting gcode that tells you your toolpath includes a point 133 inches north in empty space. I don't have any explanation for that, but your original line 11 had a Y value that required a line wrap on my wide screen monitor -- I gave up looking after a few dozen digits. That's the value I shortened from 133 bazillion to just 133.
Please Log in or Create an account to join the conversation.

8 years 7 months ago #107739
by JohnnyCNC
Replied by JohnnyCNC on topic Newbie question
You might try G94 instead of G95 along with what DanMN said. M0 is program pause. I'm new at this also so trust but verify. Good Luck John
G94 - is Units per Minute Mode. In units per minute feed mode, an F word is interpreted to mean the controlled point should move at a certain number of inches per minute, millimeters per minute, or degrees per minute, depending upon what length units are being used and which axis or axes are moving.
G95 - is Units per Revolution Mode In units per revolution mode, an F word is interpreted to mean the controlled point should move a certain number of inches per revolution of the spindle, depending on what length units are being used and which axis or axes are moving. G95 is not suitable for threading, for threading use G33 or G76. G95 requires that motion.spindle-speed-in to be connected.
M0 - pause a running program temporarily. LinuxCNC remains in the Auto Mode so MDI and other manual actions are not enabled. Pressing the cycle start button will restart the program at the following line.
(TRIJICONV4-2.NC)
G17 G20 G95 G40 G49 G80 G90 G00 X0 Y0 Z0
(MSG, " Change to .25 ENDMILL ROUGH")
(MSG, " Spindle Speed 1191")
(M0)
G43 G90 H1
G1 Z1. F5
(M0)
(Begin Feature 3 Axis)
G94 - is Units per Minute Mode. In units per minute feed mode, an F word is interpreted to mean the controlled point should move at a certain number of inches per minute, millimeters per minute, or degrees per minute, depending upon what length units are being used and which axis or axes are moving.
G95 - is Units per Revolution Mode In units per revolution mode, an F word is interpreted to mean the controlled point should move a certain number of inches per revolution of the spindle, depending on what length units are being used and which axis or axes are moving. G95 is not suitable for threading, for threading use G33 or G76. G95 requires that motion.spindle-speed-in to be connected.
M0 - pause a running program temporarily. LinuxCNC remains in the Auto Mode so MDI and other manual actions are not enabled. Pressing the cycle start button will restart the program at the following line.
(TRIJICONV4-2.NC)
G17 G20 G95 G40 G49 G80 G90 G00 X0 Y0 Z0
(MSG, " Change to .25 ENDMILL ROUGH")
(MSG, " Spindle Speed 1191")
(M0)
G43 G90 H1
G1 Z1. F5
(M0)
(Begin Feature 3 Axis)
Please Log in or Create an account to join the conversation.
8 years 7 months ago #107741
by JohnnyCNC
Replied by JohnnyCNC on topic Newbie question
I changed the G95 to G94 and line 14 Y1333... to Y2 and Z2 to Z1 so it didn't exceed the bounds of my machine and the code will run.
%
( tool 1 ENDMILL ROUGH D.25 C0. L2.5)
(TRIJICONV4-2.NC)
G17 G20 G94 G40 G49 G80 G90 G00 X0 Y0 Z0
(MSG, " Change to .25 ENDMILL ROUGH")
(MSG, " Spindle Speed 1191")
(M0)
G43 G90 H1
G1 Z1. F5
(M0)
(Begin Feature 3 Axis)
G0 X0. Y2 Z.1
%
( tool 1 ENDMILL ROUGH D.25 C0. L2.5)
(TRIJICONV4-2.NC)
G17 G20 G94 G40 G49 G80 G90 G00 X0 Y0 Z0
(MSG, " Change to .25 ENDMILL ROUGH")
(MSG, " Spindle Speed 1191")
(M0)
G43 G90 H1
G1 Z1. F5
(M0)
(Begin Feature 3 Axis)
G0 X0. Y2 Z.1
Please Log in or Create an account to join the conversation.
Time to create page: 0.216 seconds