- Posts: 29
- Thank you received: 4


Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
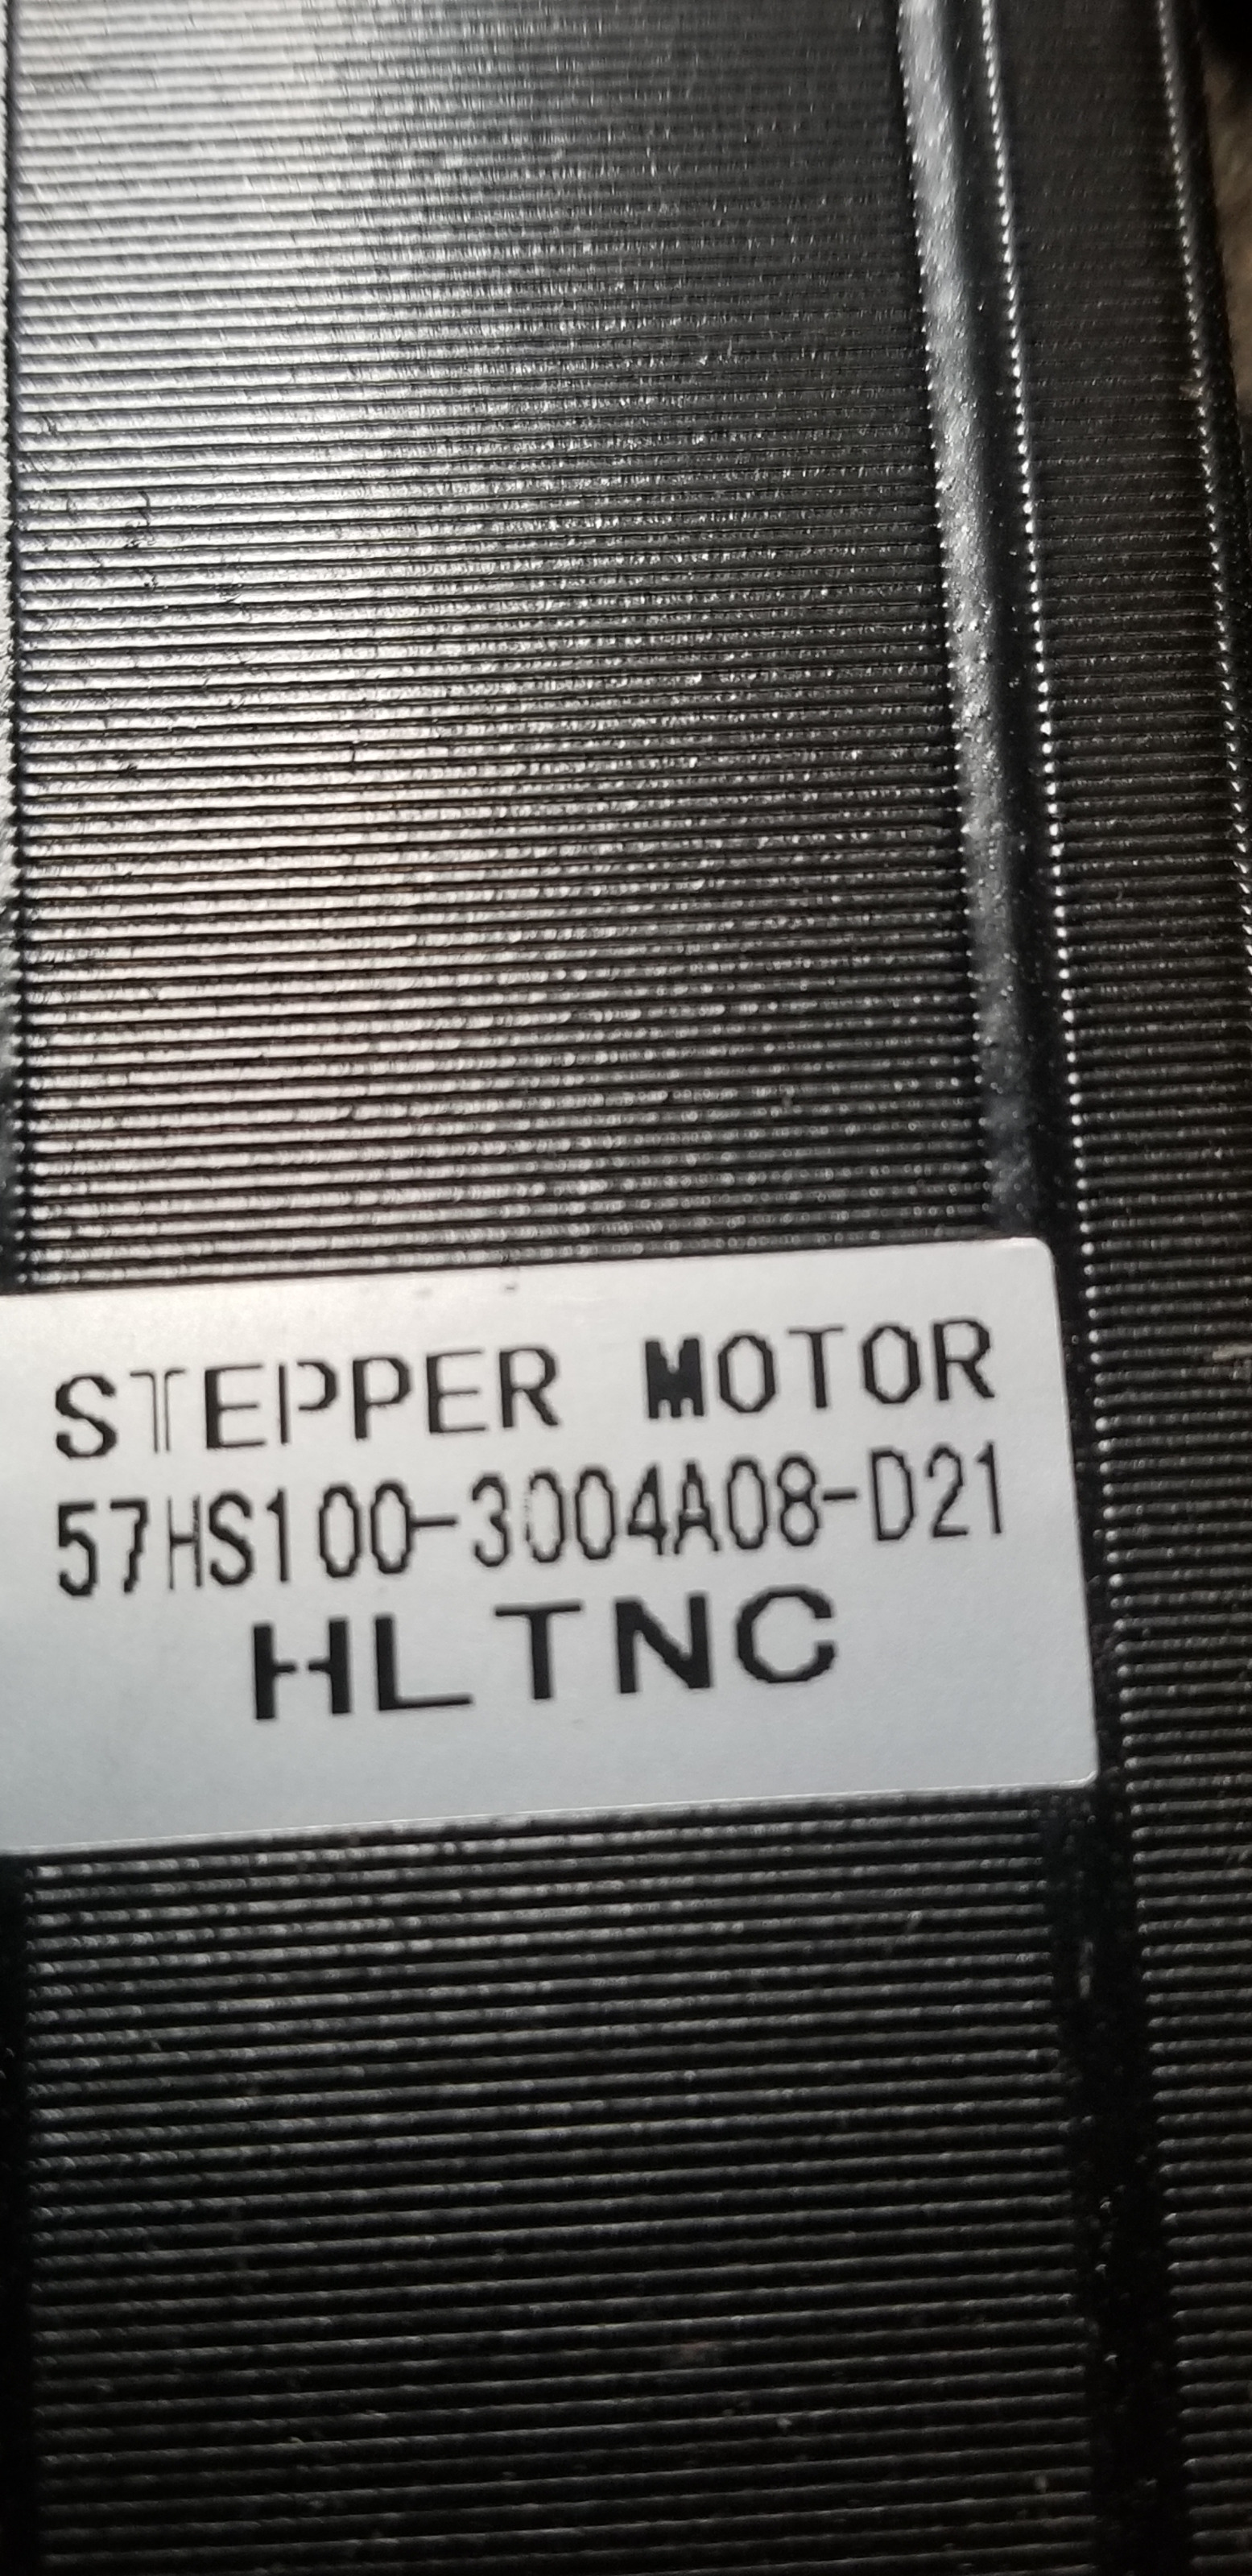
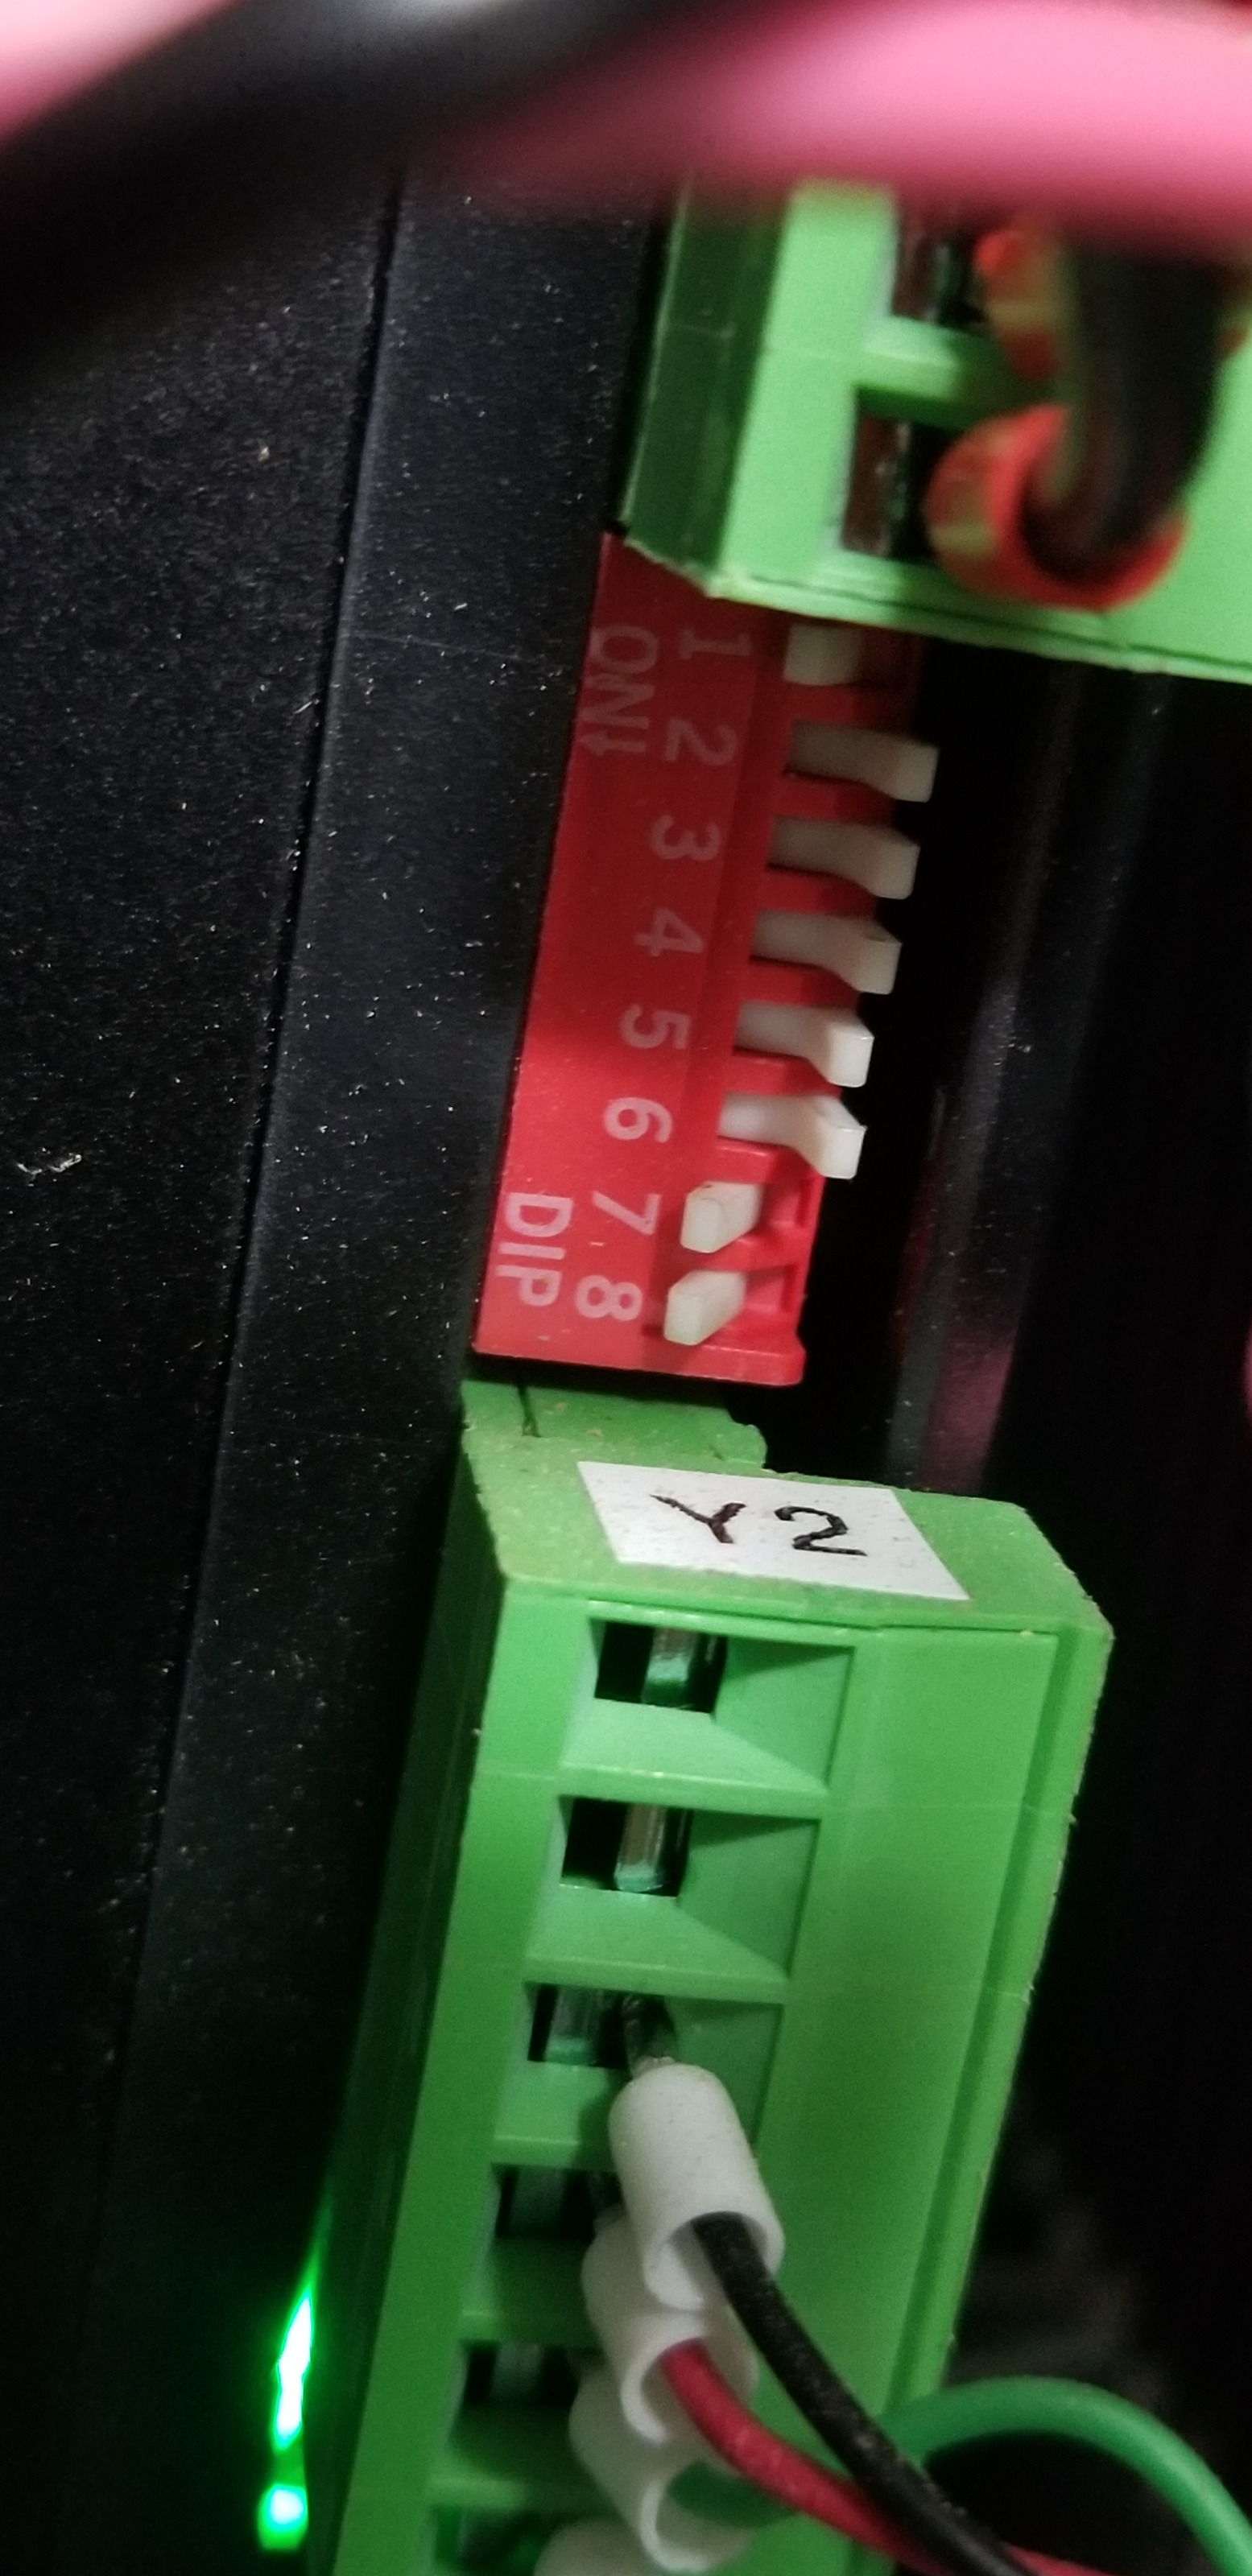
Stepper Drivers: DM542, Leadshine knock-offs. Microstep: 8. Steps/Rev: 1600 for 1.8 degree motor.Sounds like you are loosing steps on the y axis during actual machining which leads to a positional offset between the actual machine and the controller. That would then lead to the Y axis exceeding it's soft limit when issuing G0 X0 Y0 (presuming your machine has no positional feedback like encoders or scales).
Which is why hardware limit switches are useful.
[edit]
Could you provide some information about the motors and drives?
First thing you could try is to reduce acceleration and velocities for the Y axis/joint and try again.
Please Log in or Create an account to join the conversation.
Sounds like a mechanical or lost step issue
I would verify that jogging Y back and forth does not
result in accumulated position errors
Please Log in or Create an account to join the conversation.
Actually since your rapids seem to be ok you may want to try running the job again with a reduced cutting feed rate (eg feed override at say 70%).The second part of your response, should that be changing the microstep to 4 at 800 steps/rev on driver or is that a change in the INI file? Attached in my machine INI file.
Please Log in or Create an account to join the conversation.