Help - Program Not Maintaining 'Y'???

More
3 years 2 weeks ago #282998 by Lethal69GTO
I checked the machine squareness using 3-4-5 method and it was good enough for my purposes, less than a MIL.

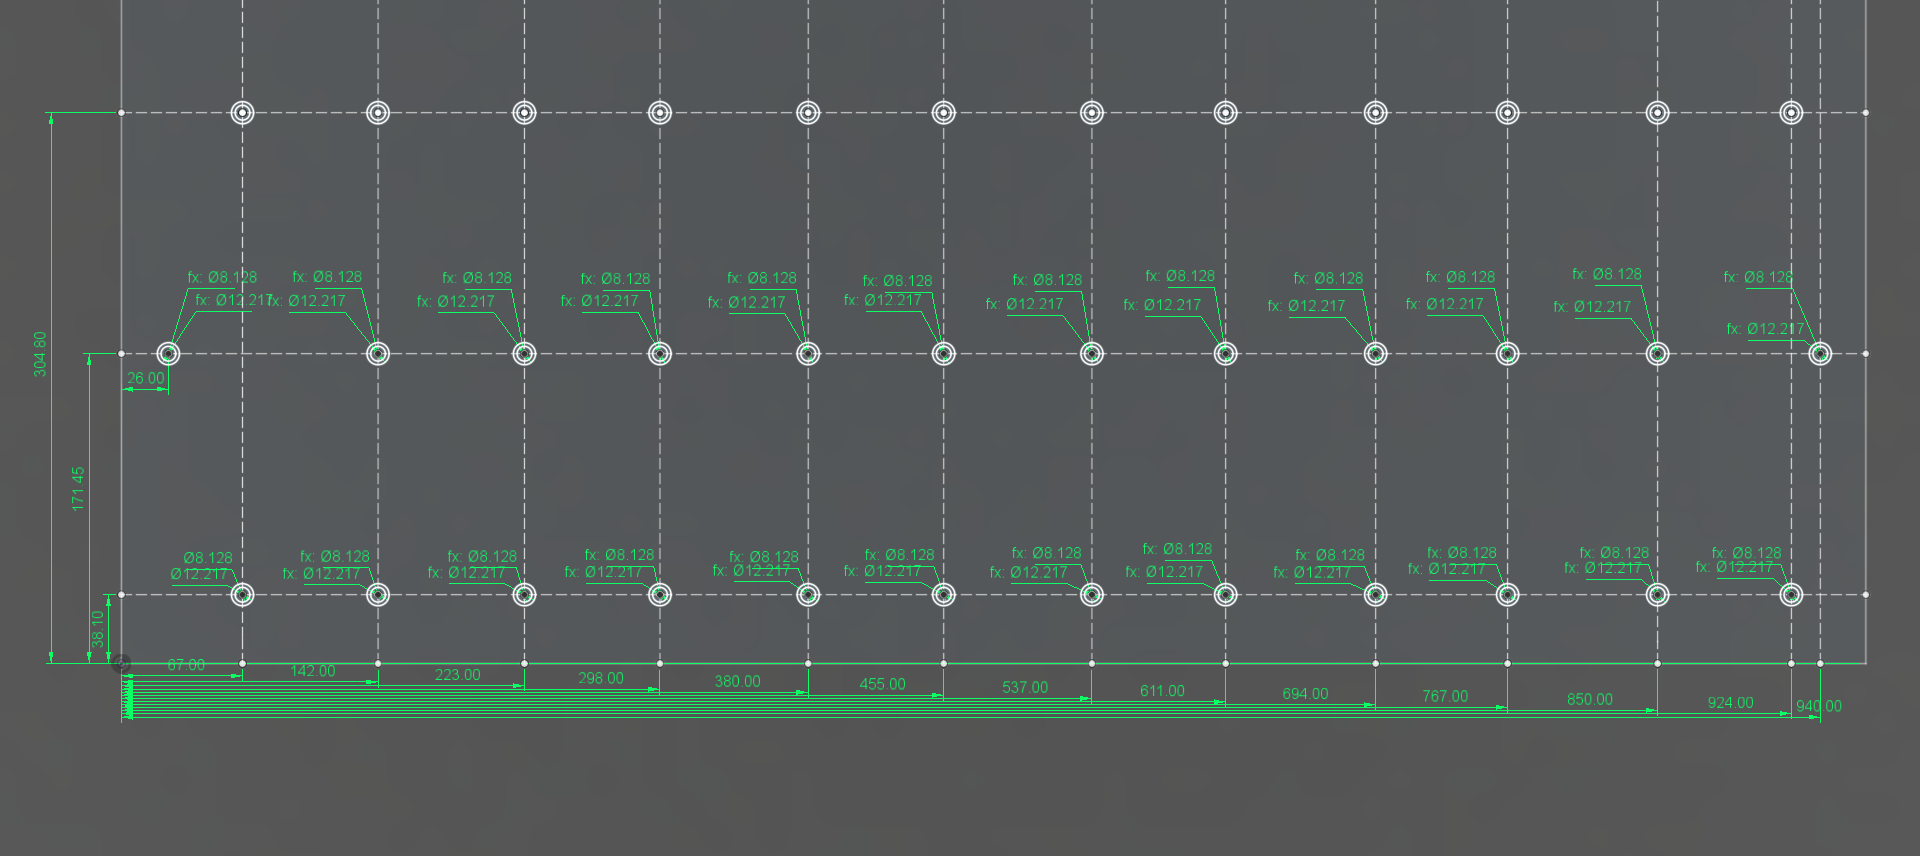
I loaded the program, set X & Y zero.  Being my first program ever, I manually jogged to all the bores hole locations, marking the X-min an X-max (as specified in the program) with lines delineating the expected positioning and hole diameter.  I just ran my program, 2 of 5 rows each with 12 holes per row.  The first row runs left to right and second row right to left  The positioning along x-axis is as expected matching the previously made marks for both rows.  The issue is that when the program is running, the Y-position of the second rows creeps towards the first row not matching the previously marked expected position, the spacing between the holes is decreasing moving right to left.

I just stopped the program and issued G0 X0, Y0.  Unanticipated was the crashing of the Y, subsequently re-squaring of the machine will need to completed again.

Post processor is EMC2 and I am using F360.

Attached is the NGC file if needed.

Please Log in or Create an account to join the conversation.

More
3 years 2 weeks ago - 3 years 2 weeks ago #283001 by Aciera
Sounds like you are loosing steps on the y axis during actual machining which leads to a positional offset between the actual machine and the controller. That would then lead to the Y axis exceeding it's soft limit when issuing G0 X0 Y0 (presuming your machine has no positional feedback like encoders or scales).
Which is why hardware limit switches are useful.

[edit]
Could you provide some information about the motors and drives?
First thing you could try is to reduce acceleration and velocities for the Y axis/joint and try again.
Last edit: 3 years 2 weeks ago by Aciera.

Please Log in or Create an account to join the conversation.

More
3 years 2 weeks ago #283002 by PCW
Sounds like a mechanical or lost step issue

I would verify that jogging Y back and forth does not
result in accumulated position errors

Please Log in or Create an account to join the conversation.

More
3 years 2 weeks ago #283019 by Lethal69GTO

Sounds like you are loosing steps on the y axis during actual machining which leads to a positional offset between the actual machine and the controller. That would then lead to the Y axis exceeding it's soft limit when issuing G0 X0 Y0 (presuming your machine has no positional feedback like encoders or scales).
Which is why hardware limit switches are useful.

[edit]
Could you provide some information about the motors and drives?
First thing you could try is to reduce acceleration and velocities for the Y axis/joint and try again.
 
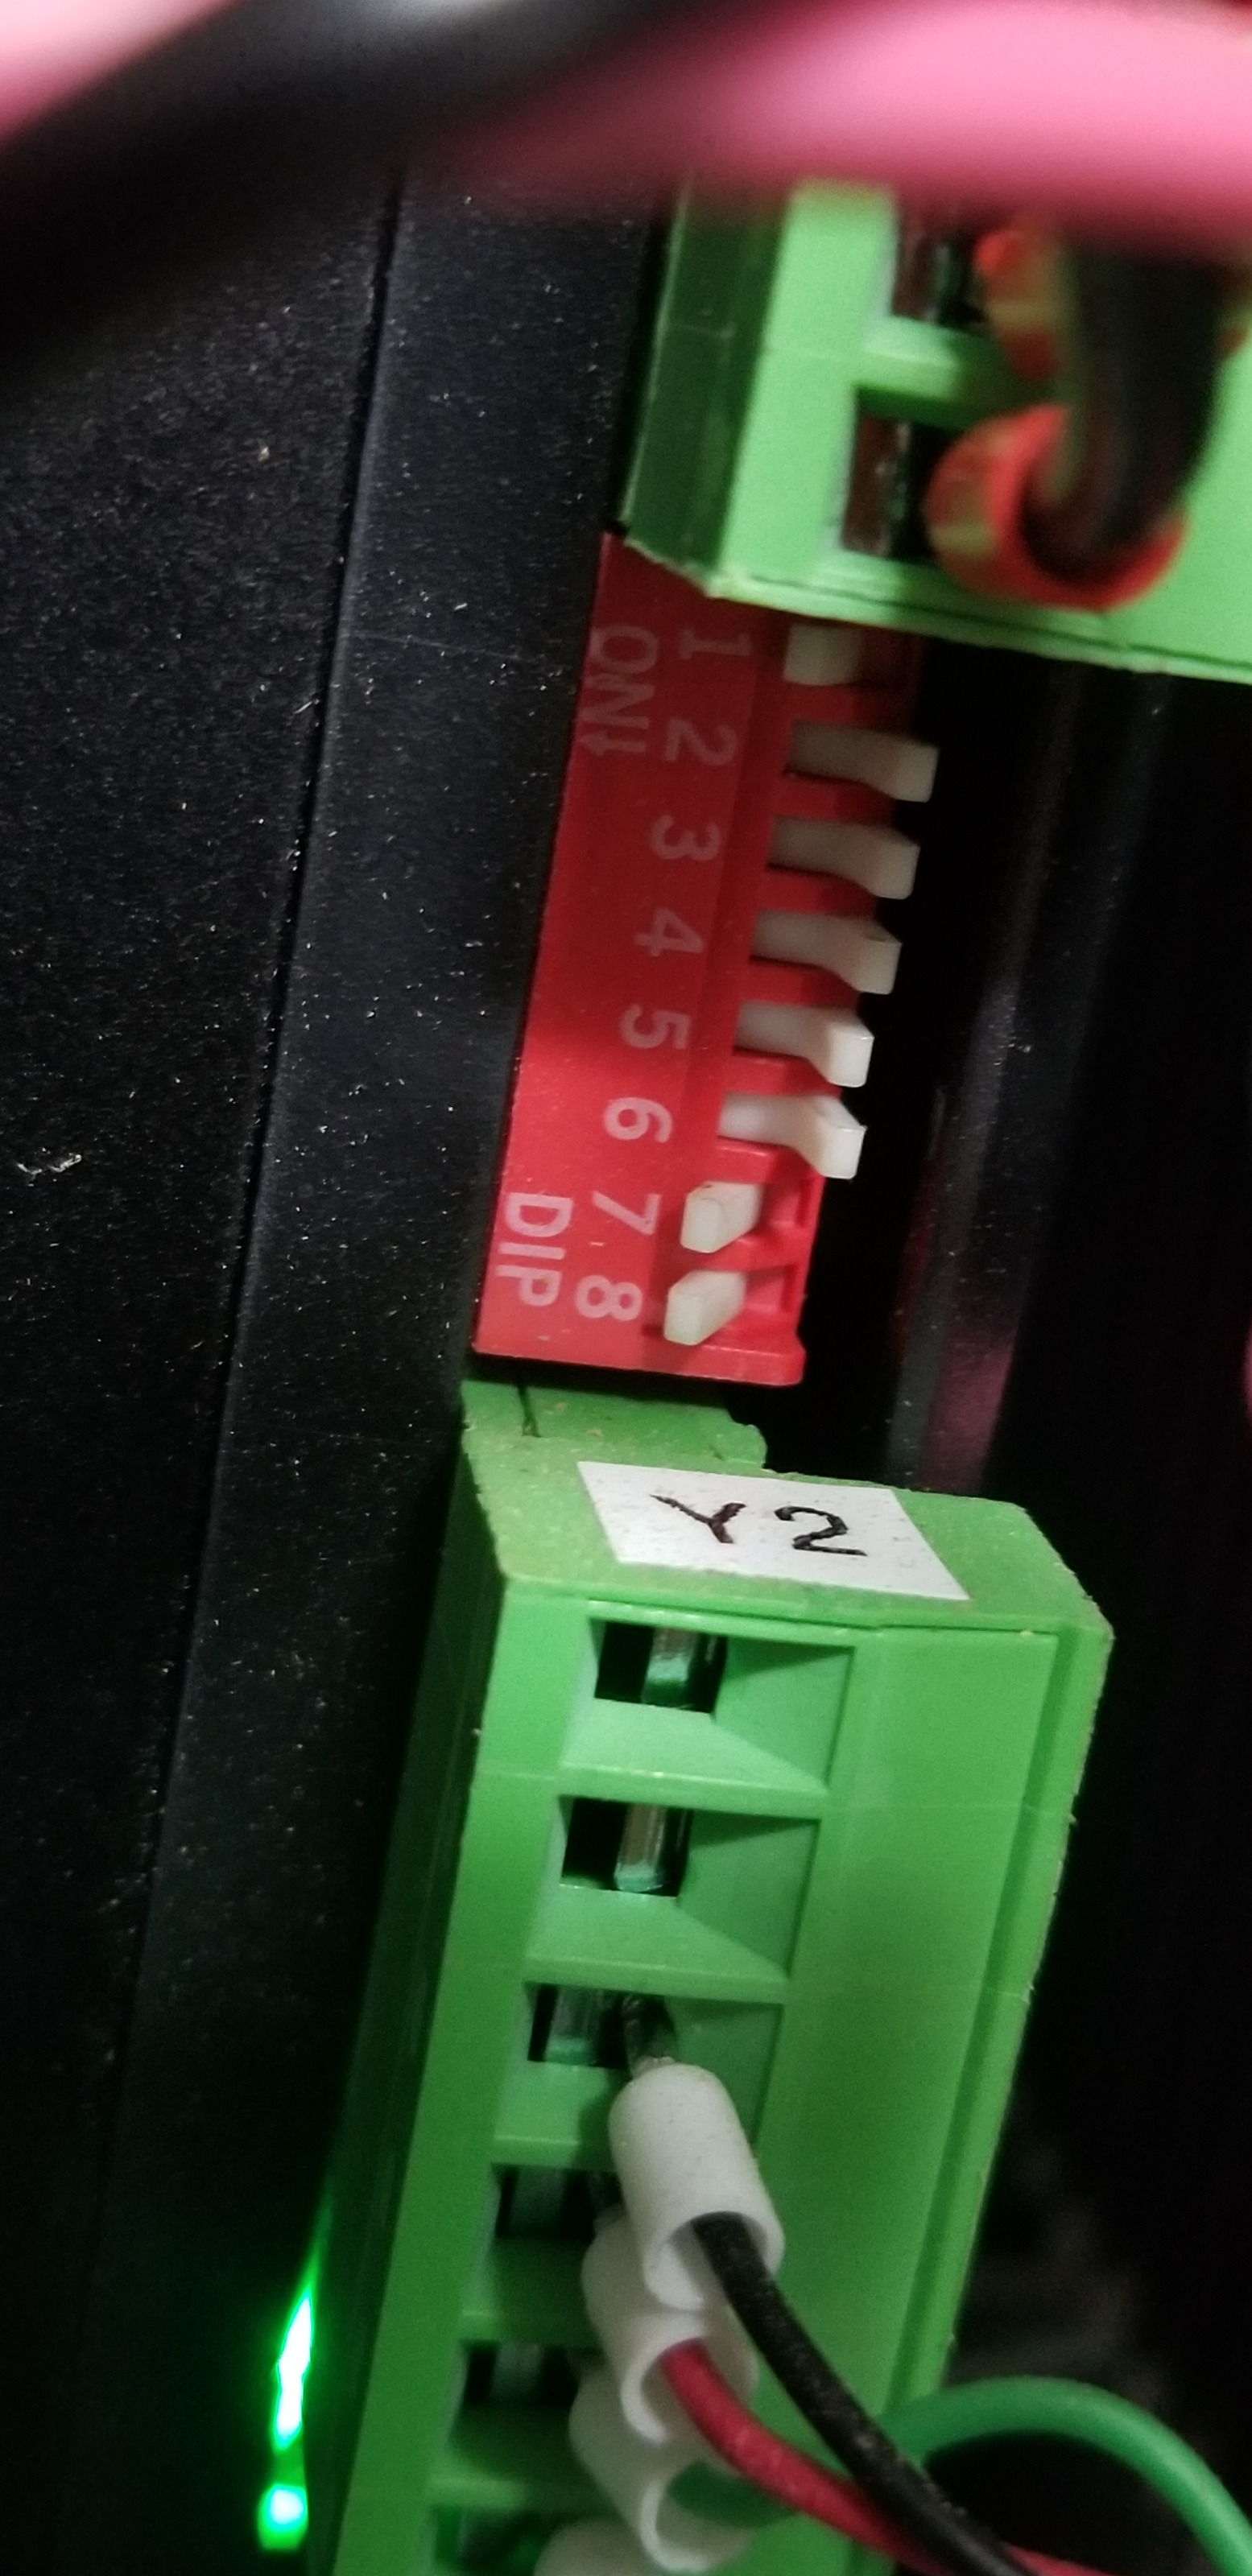
Stepper Drivers: DM542, Leadshine knock-offs.  Microstep: 8.  Steps/Rev: 1600 for 1.8 degree motor.
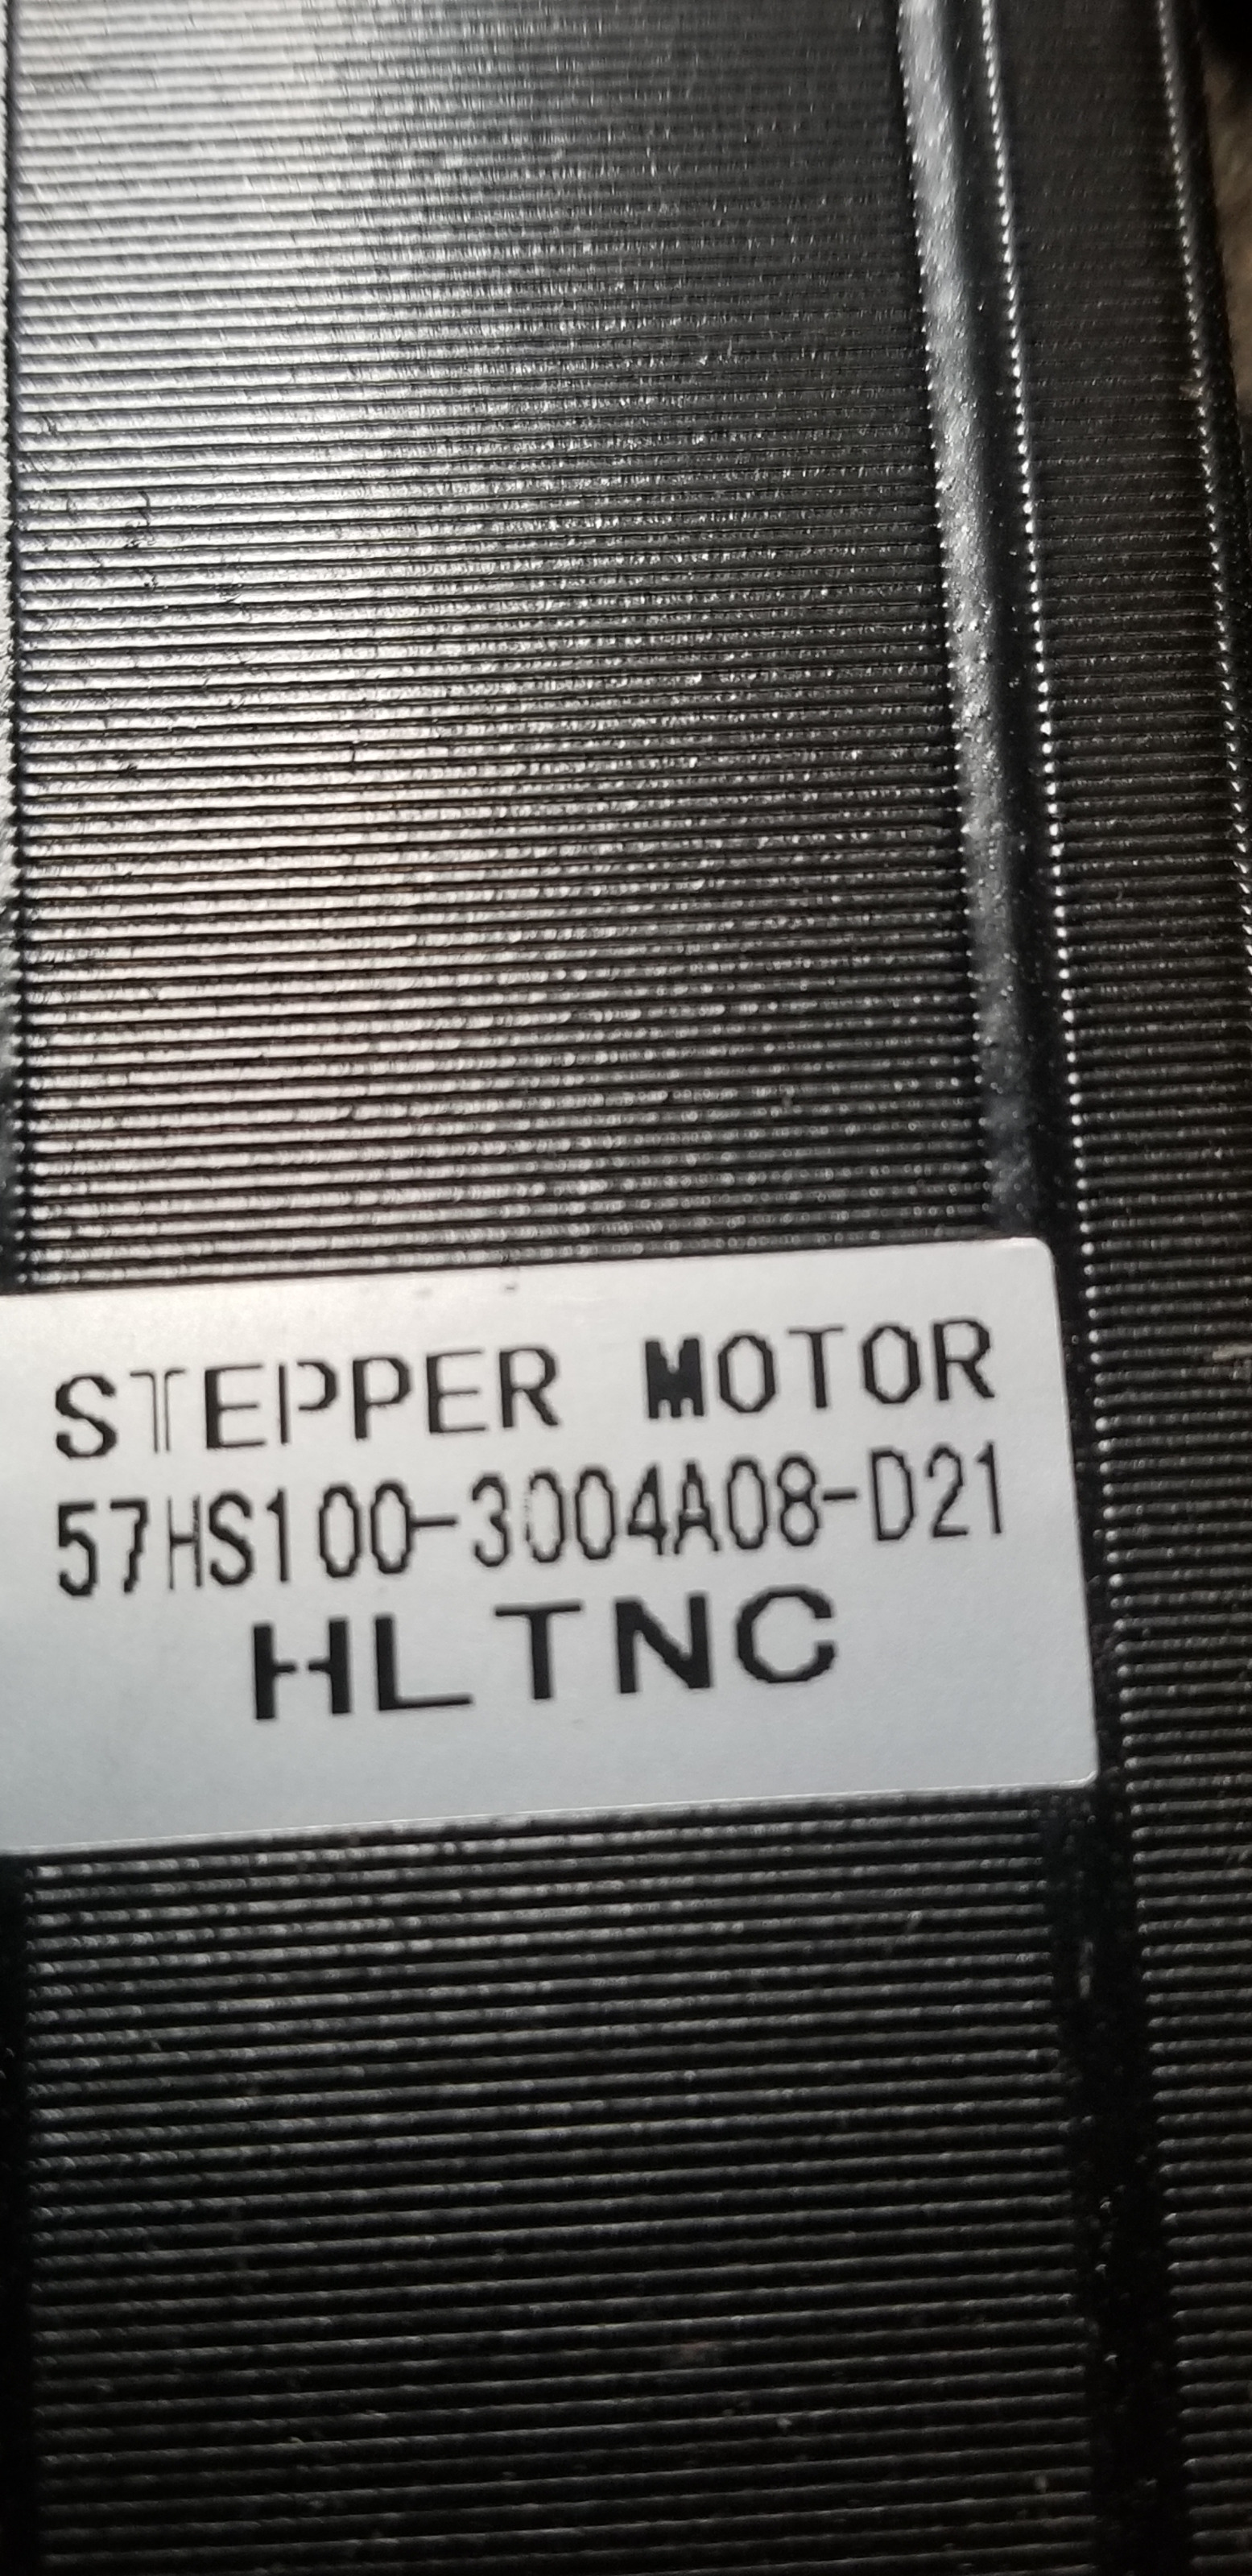
Stepper Motors: NEMA 23.  HLTNC.  4-wire, Step Angle 1.8 degrees.  Rated: 3V, 3A

The second part of your response, should that be changing the microstep to 4 at 800 steps/rev on driver or is that a change in the INI file?  Attached in my machine INI file.


Please Log in or Create an account to join the conversation.

More
3 years 2 weeks ago #283020 by Lethal69GTO

Sounds like a mechanical or lost step issue

I would verify that jogging Y back and forth does not
result in accumulated position errors
 

I was thinking the same (losing steps) and went ahead and bought replacement DM542 drivers.
I think I have been doing what you suggested moving to each Y position as shown in the sketch across all five rows, but will give it another go and take note of the Y value within the DRO display.
 

Please Log in or Create an account to join the conversation.

More
3 years 2 weeks ago #283033 by Aciera

The second part of your response, should that be changing the microstep to 4 at 800 steps/rev on driver or is that a change in the INI file?  Attached in my machine INI file.

Actually since your rapids seem to be ok you may want to try running the job again with a reduced cutting feed rate (eg feed override at say 70%).

Please Log in or Create an account to join the conversation.
Time to create page: 0.346 seconds
Powered by Kunena Forum