Rods "Spaceship" Scratch built Plasma Cutter build

More
4 years 6 months ago - 4 years 6 months ago #240984 by rodw
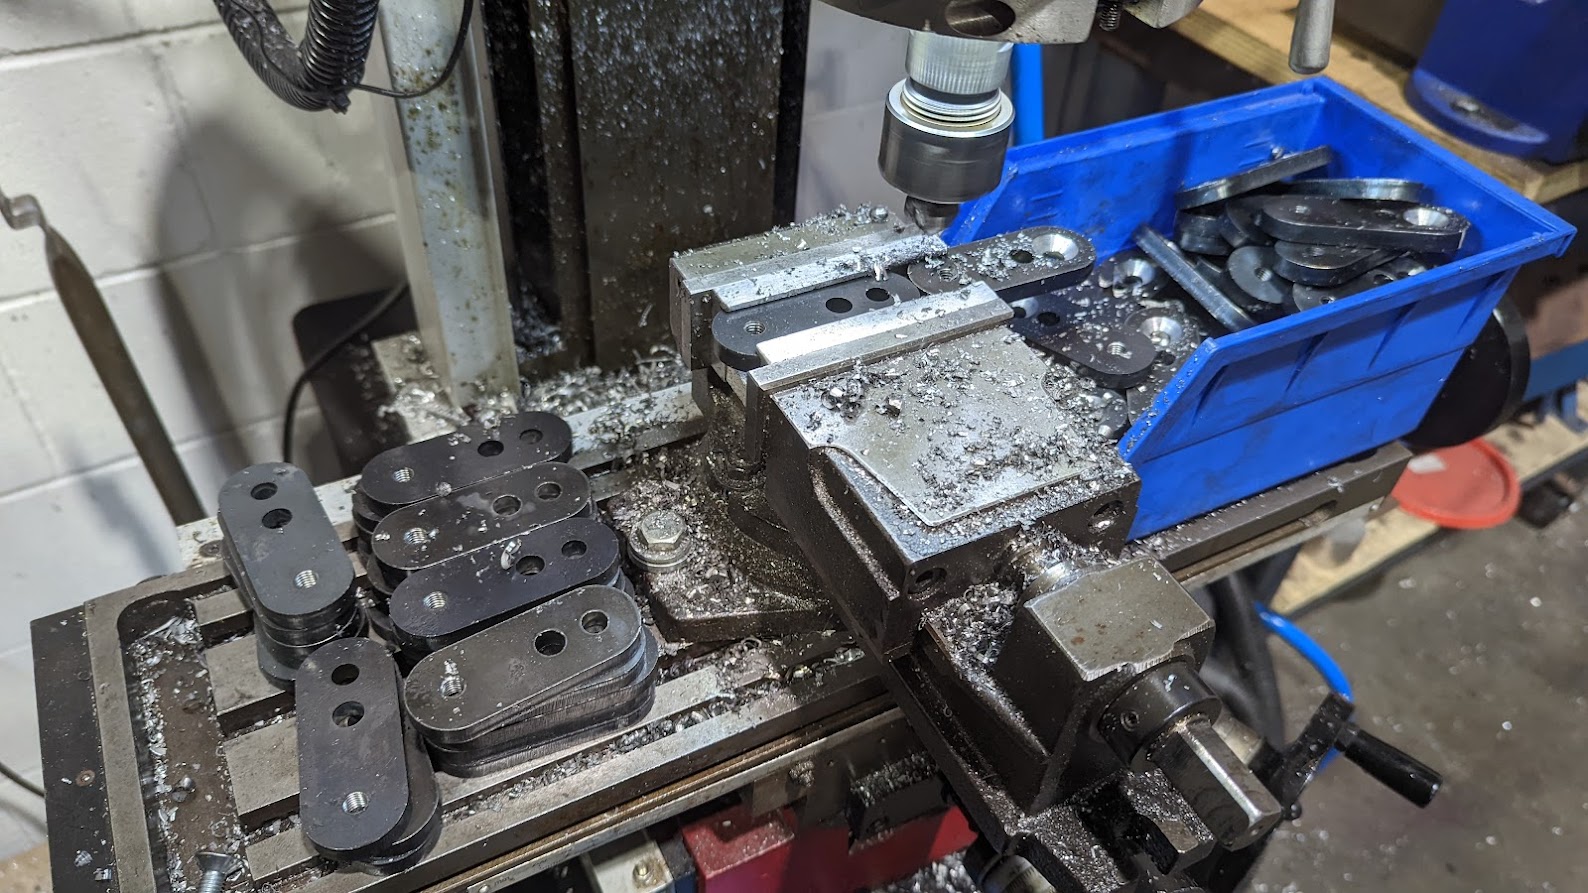
Thanks, The bit was held in an ER32 collet so I doubt it would slip. I think the real issue is the Z axis motor coupler has been slipping where the bellows attaches to the end (eg not on the shaft). I have another one here but have not had time to try swapping it out. I wanted to make a jig to hold parts for drilling and tapping but I ran out of time so  I did a batch of 200 on my  manual mill.

 
This is pretty easy with a sliding jig but its a bit underpowered on the countersinking

This means the pressure is off for now but the job is still setup so I can counterbore the holes 30mm diameter for a nut to hold it to the mill T slots and the plan is to press in some dowell pins I have to align it in the T slot.

But yes, the jacks underneath are a good idea. Thanks.
Last edit: 4 years 6 months ago by rodw.

Please Log in or Create an account to join the conversation.

More
4 years 6 months ago #241000 by machinedude
ER 32 is bigger in size so if you tighten it well it should not move on you. drill chucks i don't have as much faith in. i don't really have trouble with slipping in a tool holder but my belief is there is no such thing as too tight for the most part.

i have done manual stuff like you are doing in the past just not on parts that big. the sliding fixtures work it just gets old fast doing large runs. you might be able to use a tapping head and tap holes like that as well. tapping heads are expensive to begin with and only get more expensive as the size gets bigger but i have used them in the same way you are working now with the sliding fixture. once again not fun doing tens of thousands of parts this way but it does work fast.

sometimes work is not very precise and you get into a need for just the basics and simple quick operations like this. the work i have seen like this was from stamped out parts.
The following user(s) said Thank You: rodw

Please Log in or Create an account to join the conversation.

More
4 years 6 months ago #241029 by rodw
Yes, when I started making these parts 12 years ago I cut down 32mm x 8mm flat bar, drilled the holes and used a tapping head in a drill press. Then I got the blanks laser cut. Then I outsourced the whole job in Australia but they would often stuff up. So I sent it to China for a while and they never stuffed up.

But with all the logistics issues ex China, I decided to bring it back in house.
The little Seig SX3 mill shown with the sliding jig has a tapping function so pressing a button on the handle reverses direction so it works really well. Much easier than the bulky tapping head.

Using the jog function on the CNC VFD in manual mode is also just as good as the SX3 tapping mode and the 1.5 kW 3 phase spindle eats the countersinking.

The CNC plan is to hold 10 at a time with the parts located on a 10mm dowel in the spare hole that is needed for clearance purposes. For threading in the absence of an encoder input on the Ethercat electronics, I plan to use a 3 thread M8 x 1.25 threadmill. I've tested this in aluminium and the results are perfect.

Somebody suggested milling the countersink with a 12mm 45 deg spot drill to make it easier on the machine but I think just plunging with a countersink will be faster.

Please Log in or Create an account to join the conversation.

More
4 years 6 months ago #241044 by machinedude
plunging with the counter sink would be faster and faster is better until something breaks :) then a ramping tool path is going to seem like a great idea after the fact :) well that's usually how my luck goes most of the time anyways :)

sometimes slow and easy wins the race in the long run, if you have something running smooth then it frees you up to do other things and not worry about the one machine that is pushing it's limits. fixturing to do as many parts as you can fit on the machine is good too. the longer it runs the more productive you are doing other things.

Please Log in or Create an account to join the conversation.
More
4 years 3 months ago #247081 by SJDrummond
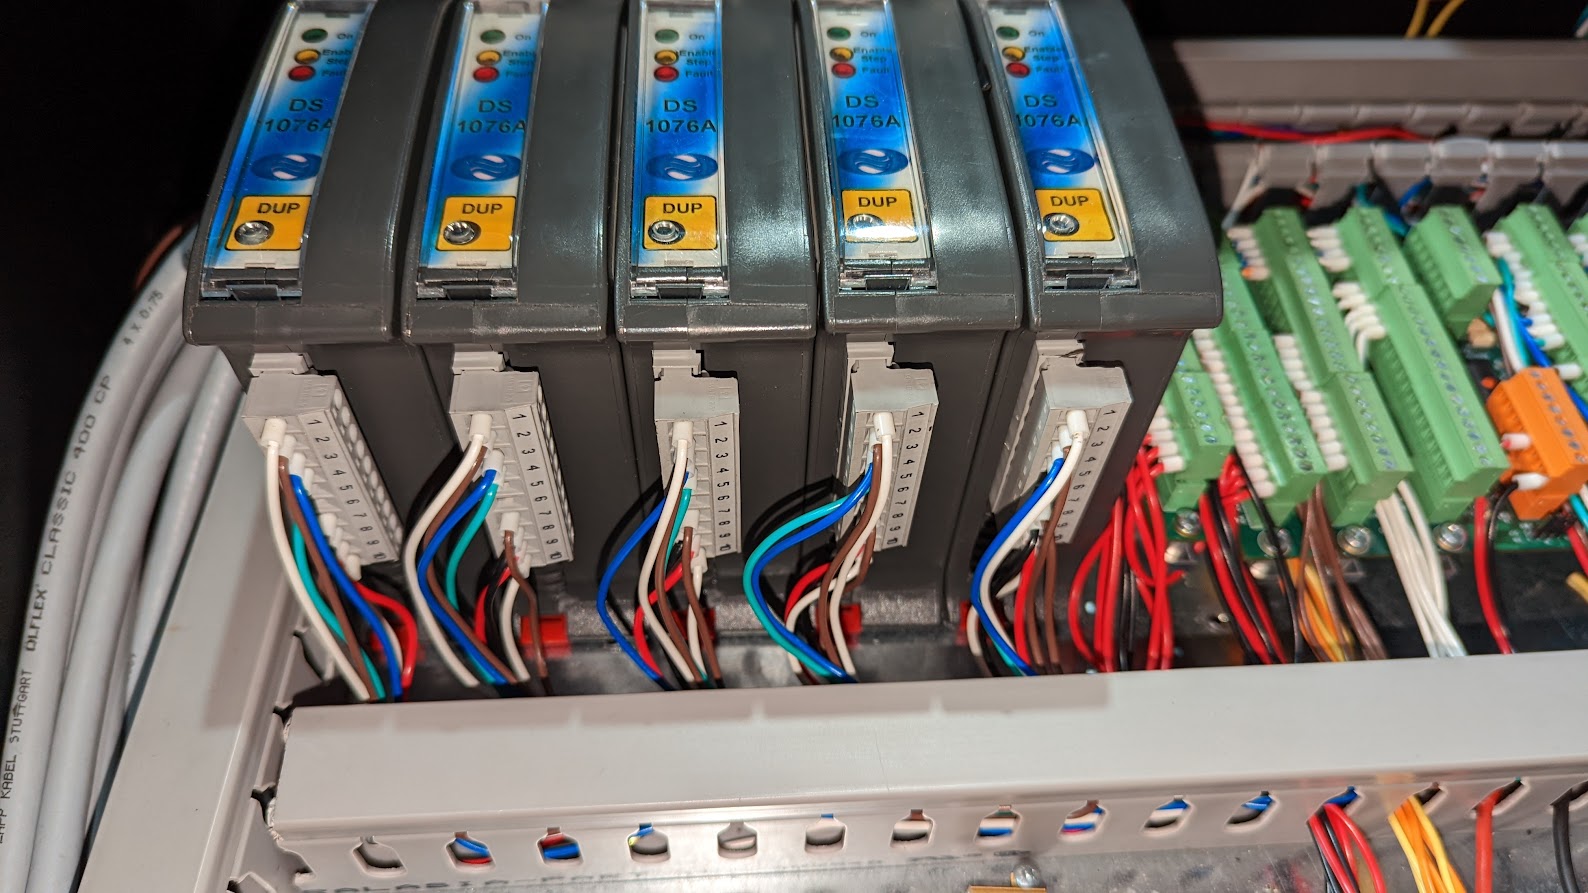
First off I'd like to say a big thank you for the information you have provided on your build. Ive been following your Spaceship Plasma build for a while and decided to take the plunge and swap my OpenBuilds Blackbox 4X control to a QTPlasmaC setup, using your electronics design as a base (albeit with different drivers).

My build so far contains:
- Mains filter IEC connector.
- A 70+70V 1000VA AC toroid from Airlink Transformers.
- Meanwell MDR-40-24 for Field power,
- Meanwell HDR-15-24 for ohmic sensing,
- 4 x DM860T AC Stepper drivers,
- MESA 7i96s with bulkhead ethernet connector, (7i76e was out of stock)
- MESA THCAD-10 for voltage reading,
- MESA THCAD-5 for Hypersensing (using Rods special magic),
- Hypertherm Powermax 45XP with Machine Torch and CPC.

Ive got a few questions that would really help me out if you have a minute.

- I was wondering if you had any updates/ new images of the control box at all?
- What the box is to the left of your Meadwell-MDR-40 on your "Spaceship MkII" image you uploaded previously?
- Which fuse holders did you use? Struggling to find similar ones.
- What are your relays being used for?

Ive done by best to find this information across all the forums but I think Ive now exhausted most of the list.

Thanks so much.
All the best,
Sean

Please Log in or Create an account to join the conversation.
More
4 years 3 months ago #247089 by rodw
The part to the left is a contactor that is activated by the red safety relay
The fuse holders are from Ocean Controls Here in Australia  oceancontrols.com.au/

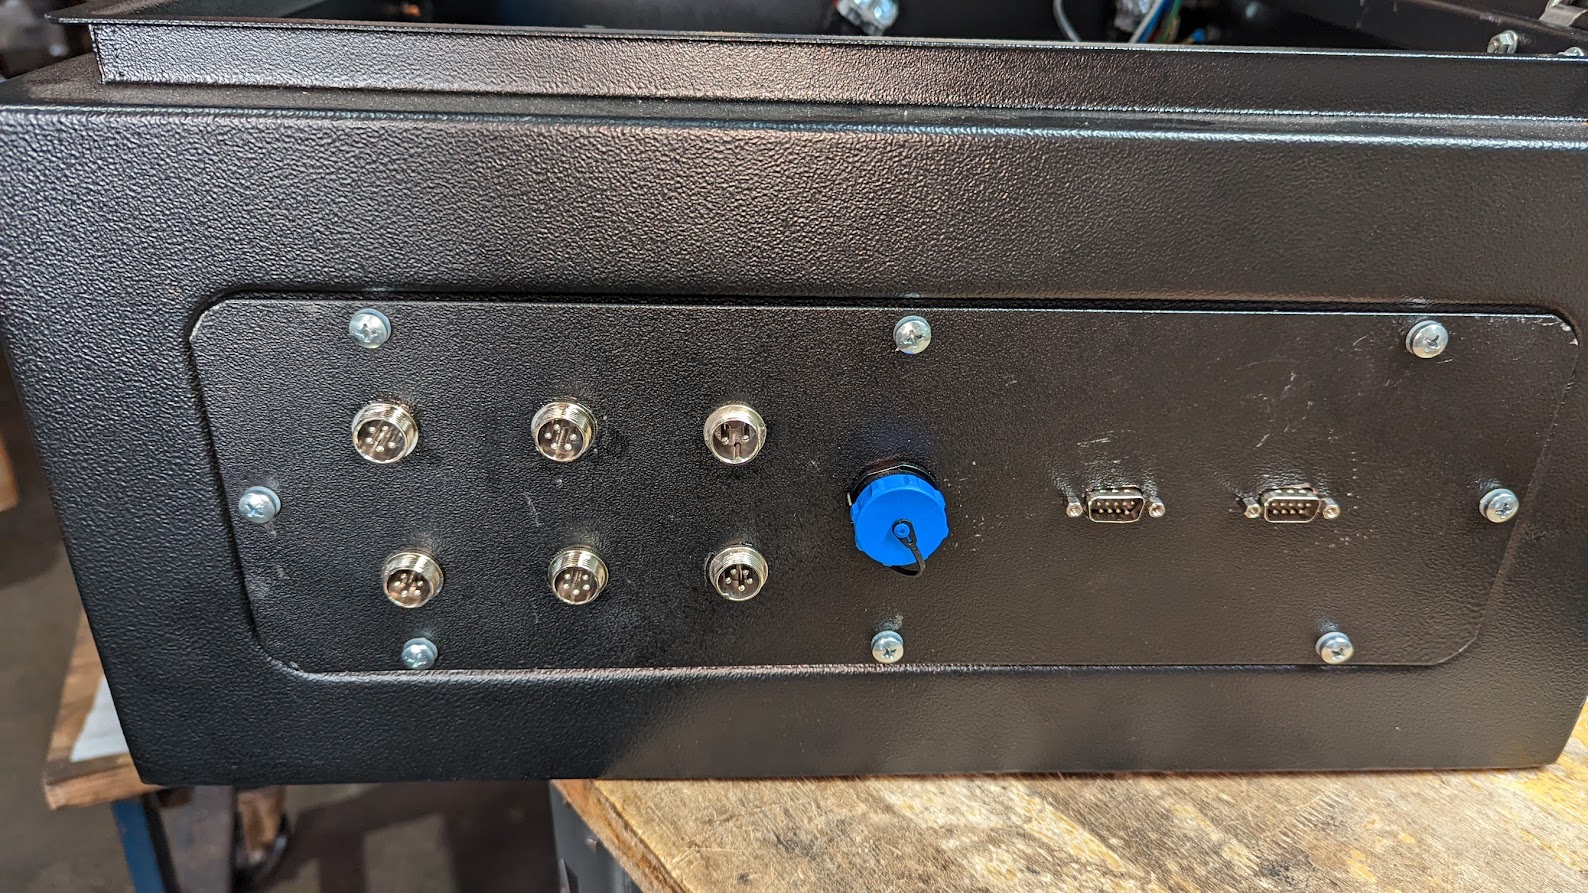
The control box is still a work in progress. All the wiring to the stepper controllers are done
 
I got a friend to solder in all the connectors for the stepper motors because he's been trained to NASA standards when it come sot soldering
 

We used 5 pin connectors so the shield can be passed through right to the controllers themselves.
The 2 pin connector is for ohmic sensing. 
The blue one is a Weipu 12 pin connector that goes to the Hypertherm CPC connector.

There is not really much left to do now. The DB9 connectors are for table and X axis sensors. So its just a matter of wiring them up and a couple of extra wires.

I would not use the silver GX616 connectors again as they are too time consuming to solder. The last control box on the mill just used cable glands and the wire went right to the drivers.
 
The following user(s) said Thank You: tommylight, my1987toyota, RNJFAB, SJDrummond

Please Log in or Create an account to join the conversation.

Time to create page: 0.574 seconds
Powered by Kunena Forum