Hi Peeps,
Im pulling my hair out trying to debug a poor surface problem. I have a LinuxCNC retrofit Haas mini mill. Dimensional accuracy is within 5 microns, perfect. Backlash is around 3 microns.
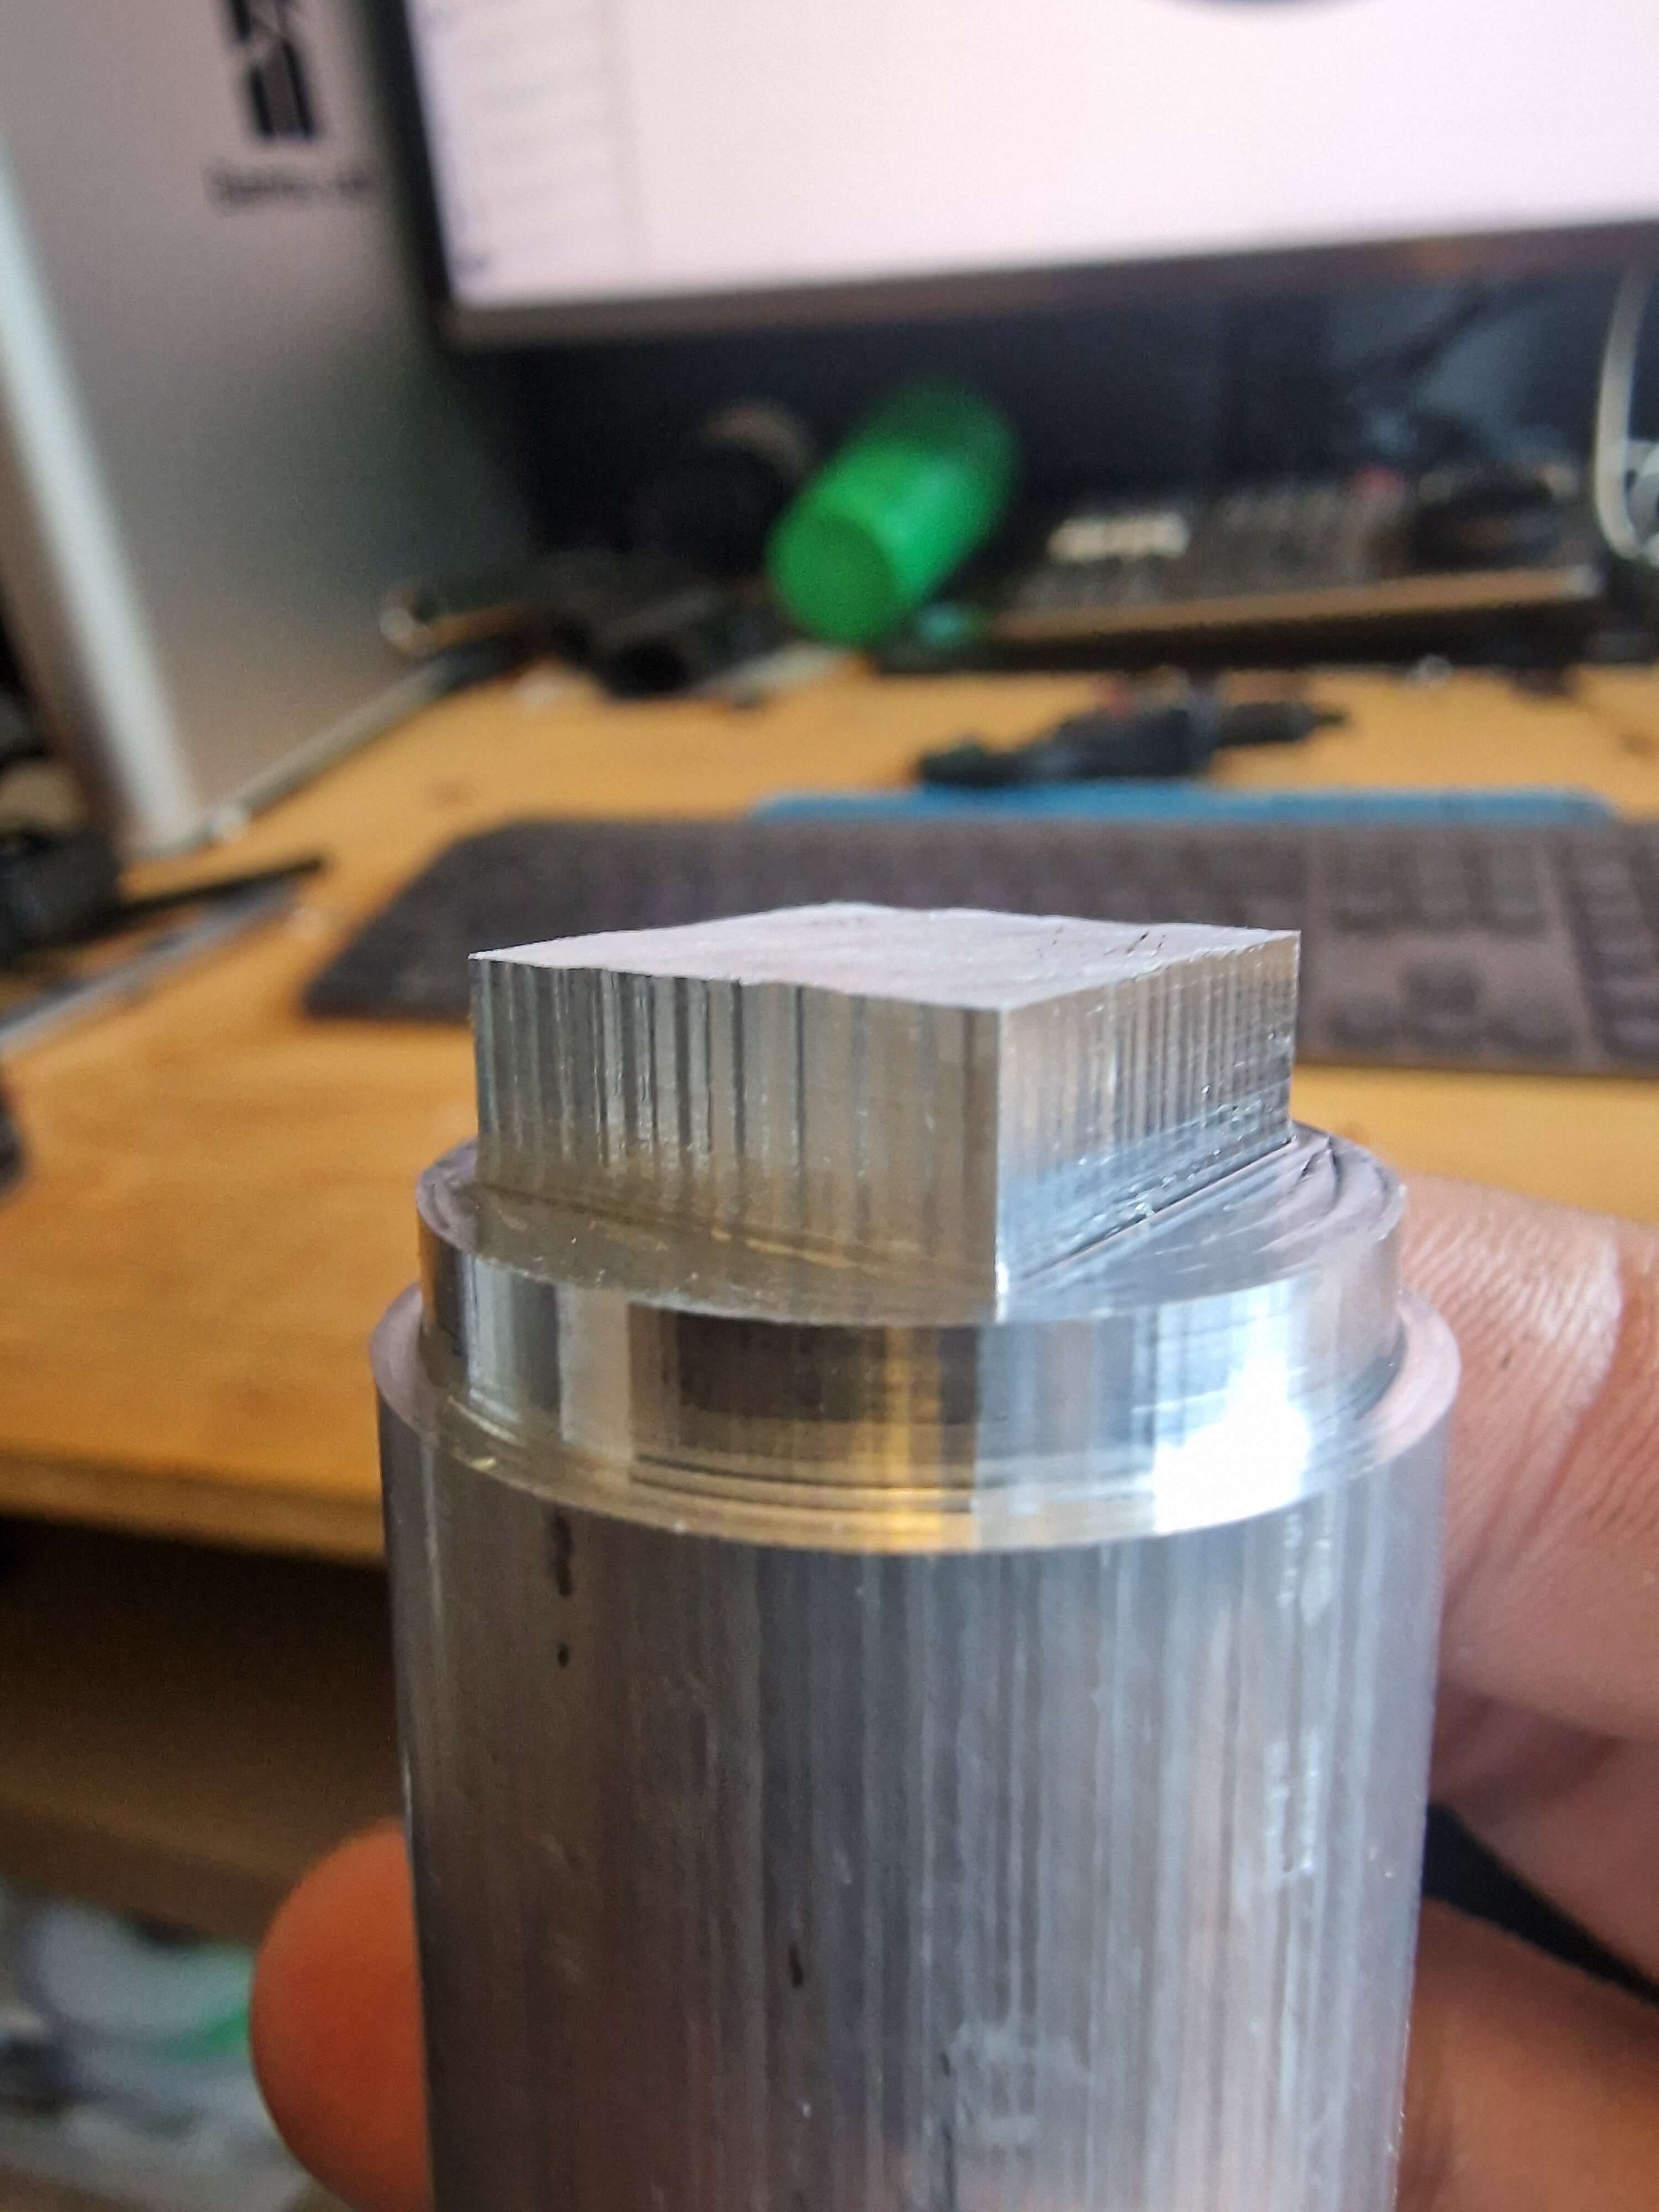
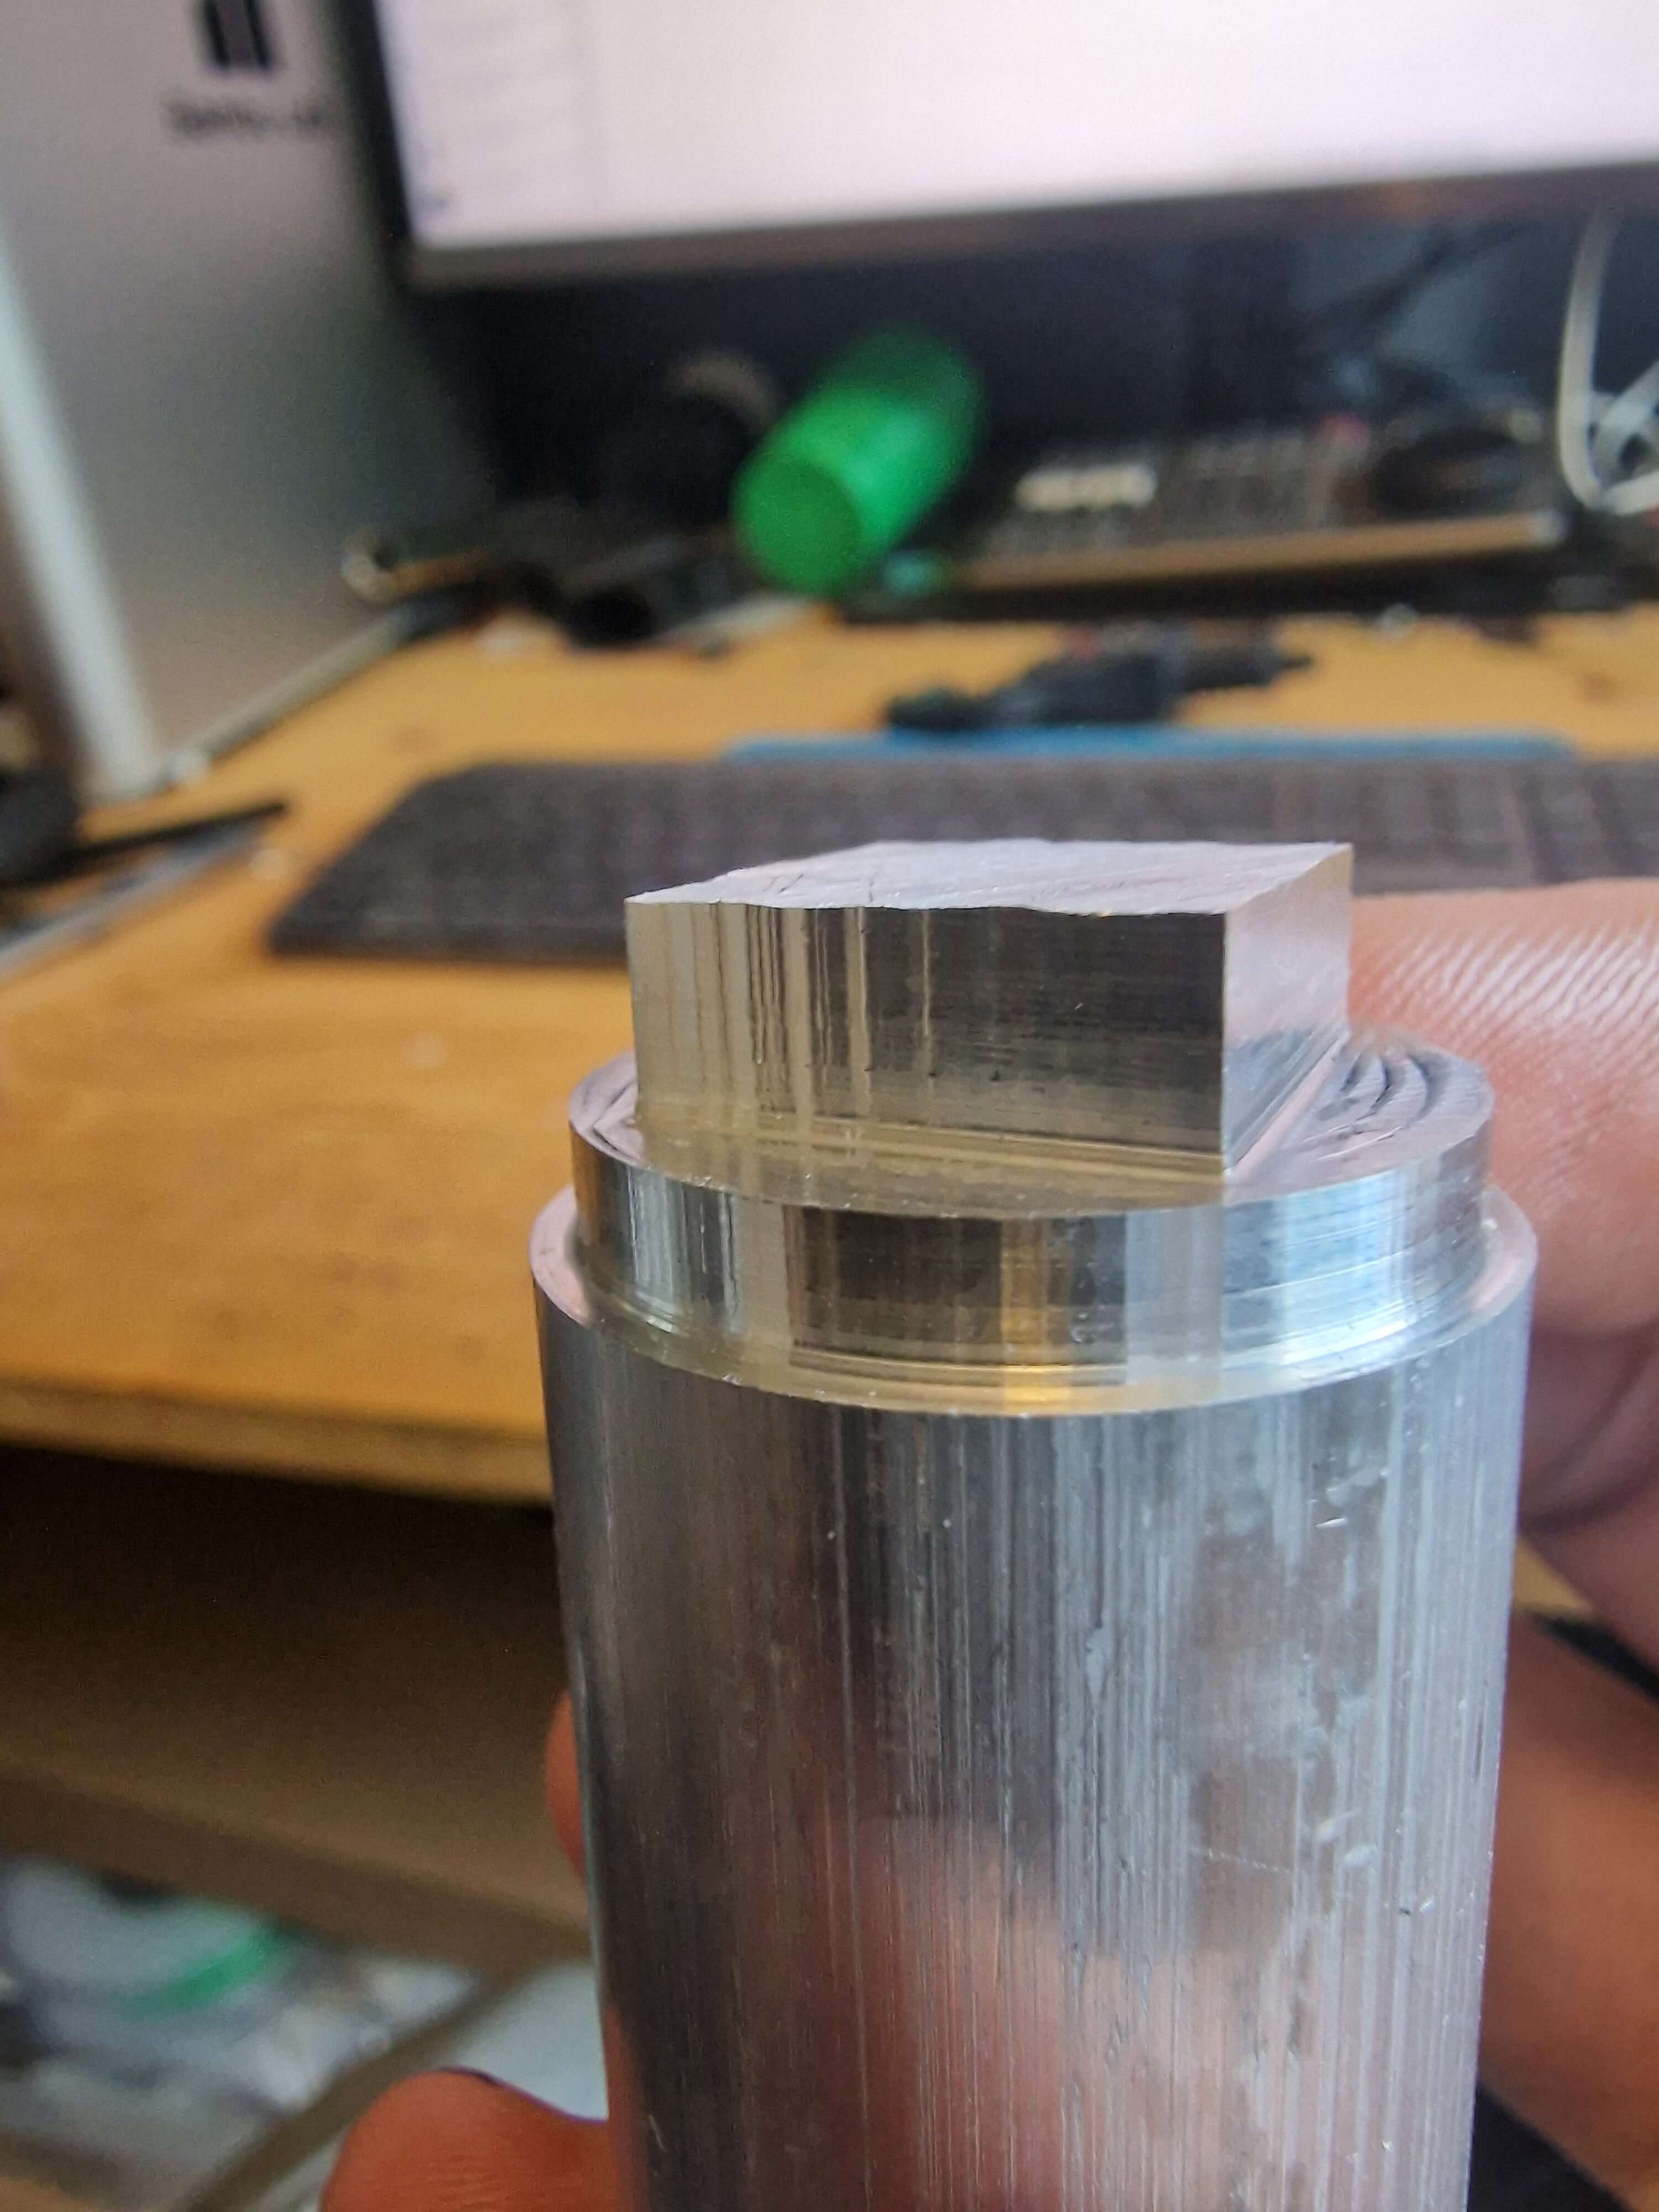
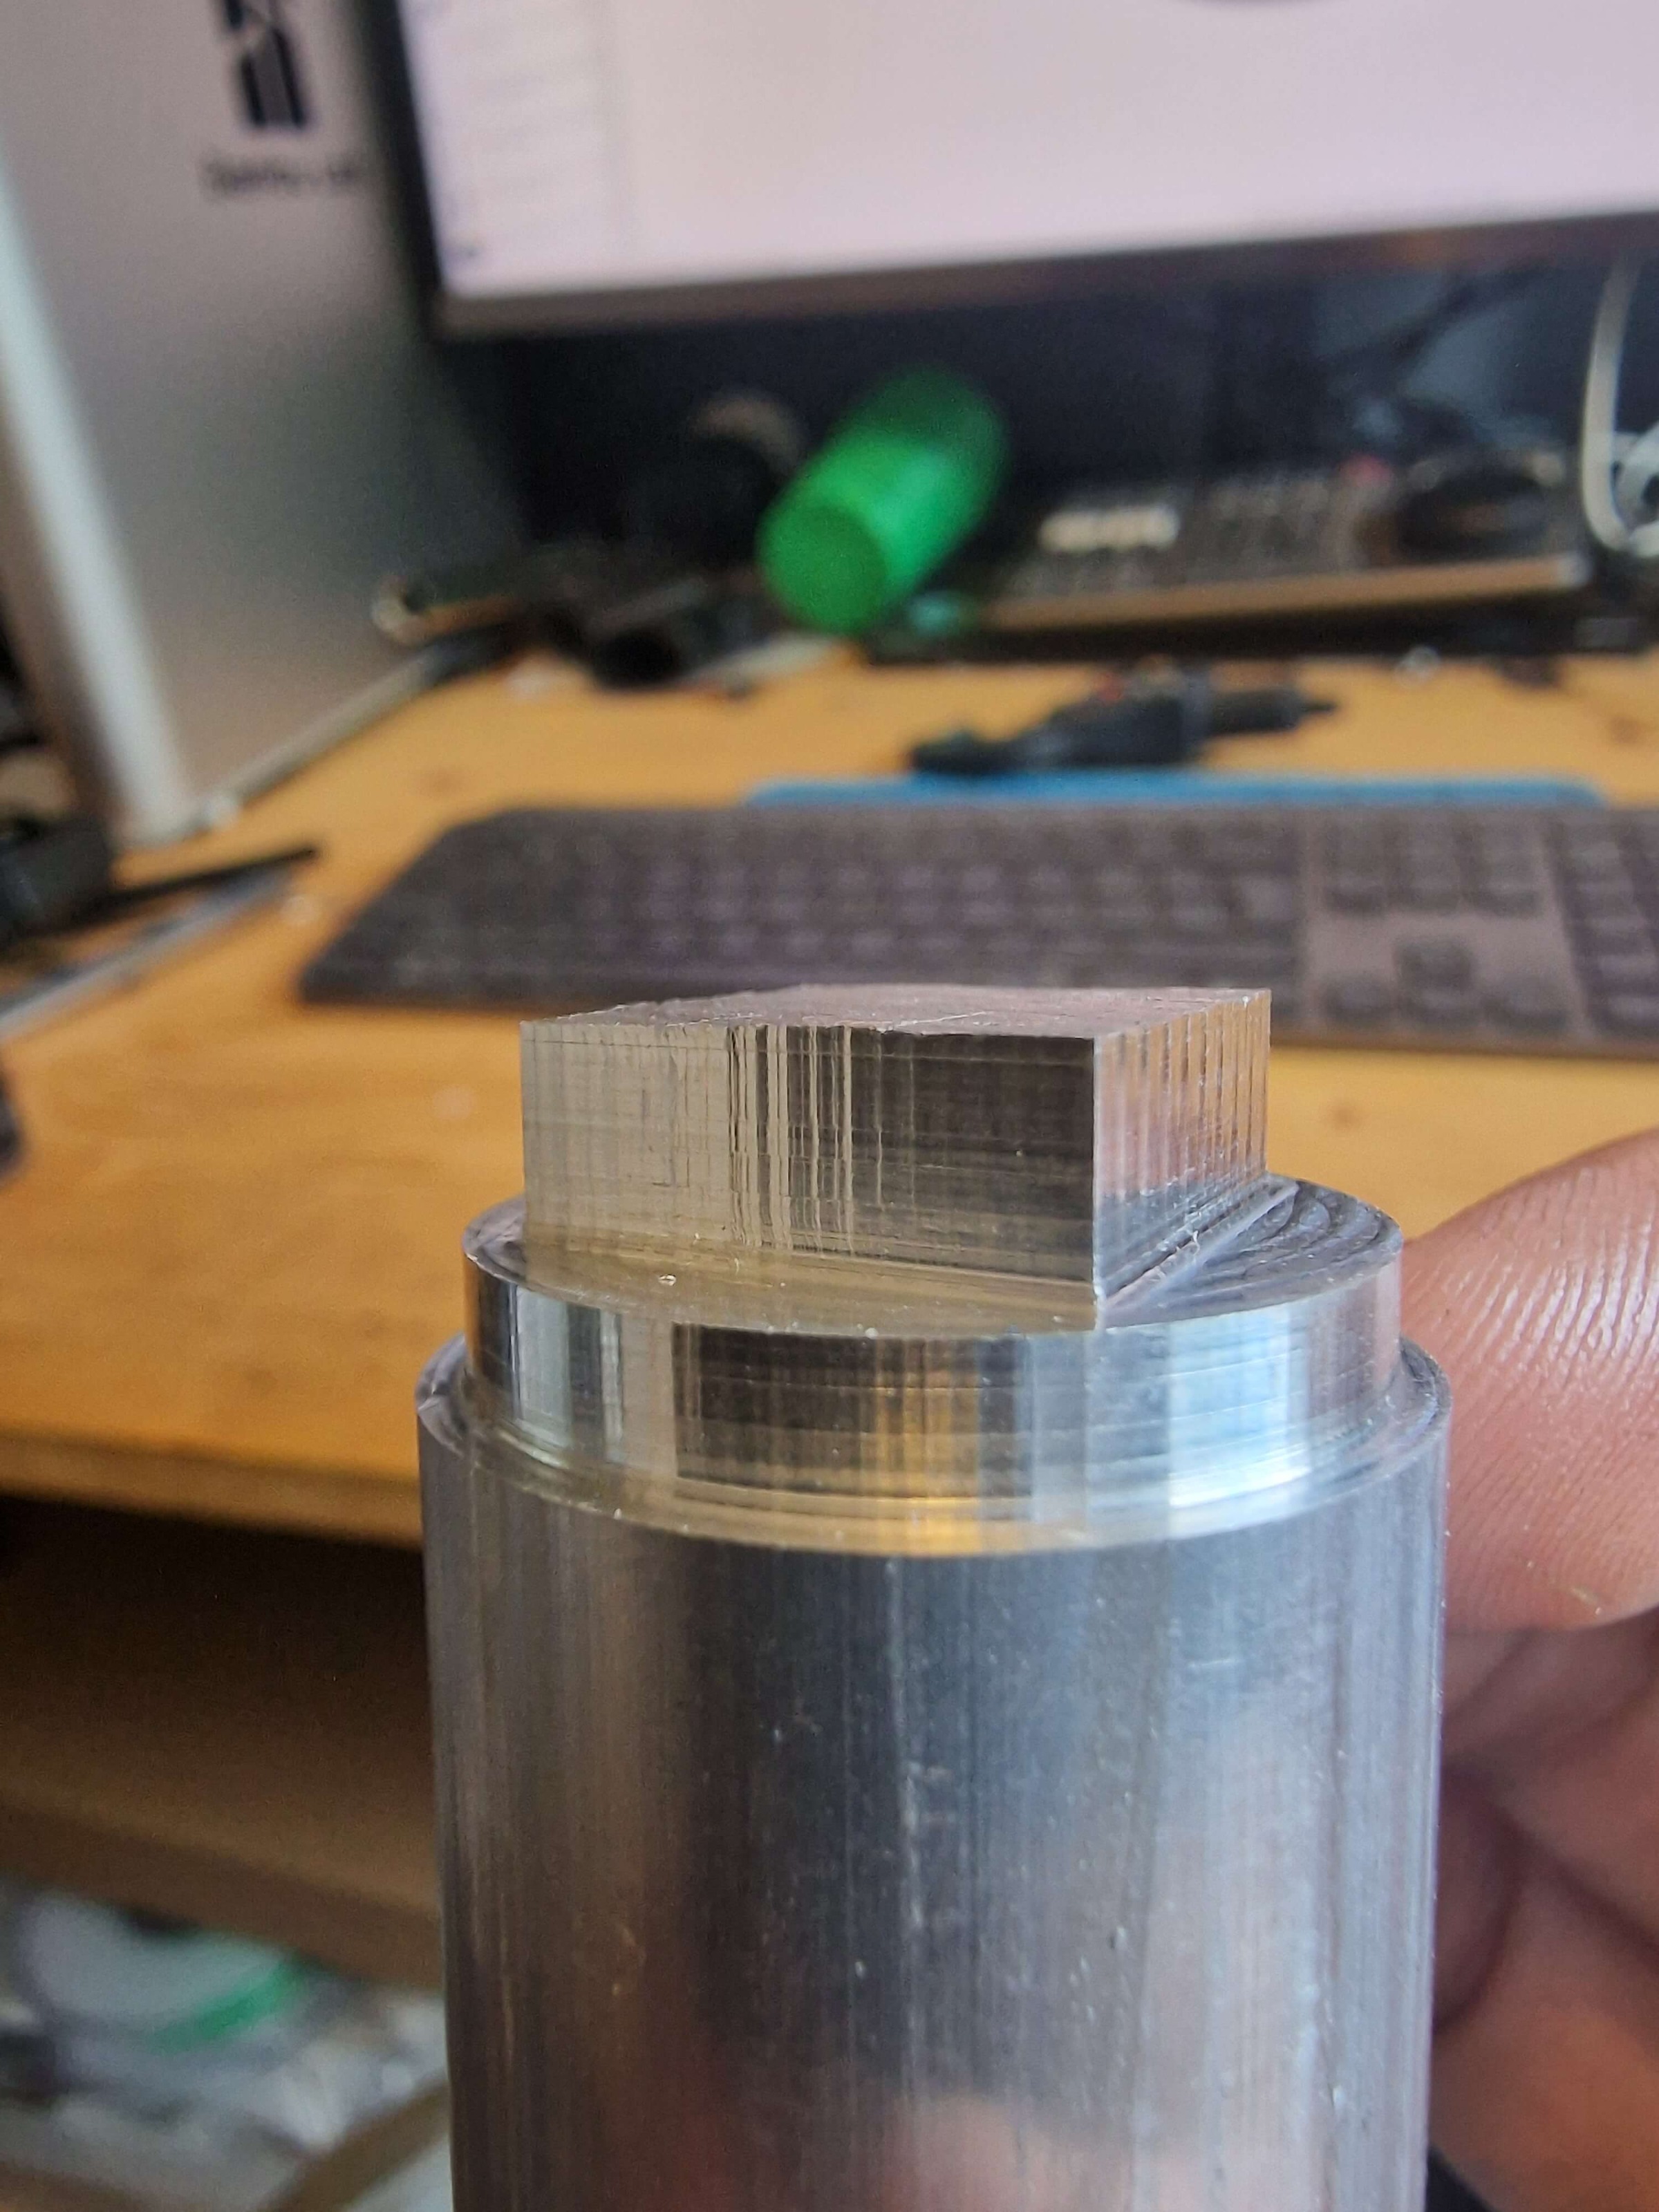
The problem is the even faceting im getting, this is only on round or any move that needs the x and y axis working together. Straight lines in x and y are a nice and smooth surface finish. I have attached a few pics for reference.
the cutting strategy was adapive clearing with 0.5mm stock to leave cleaned up with a profile toolpath
The square was oriented with the points facing north, south, east and west, forcing them to be cut using both servo motors.
I'm using AC servo motors with 10.000 steps per rev. So 1 micron per pulse.
I'm running a 2 ms servo thread, probe basic on linuxcnc 2.9
for this cut I used 0.001 tolerance and tried smoothing on and off with no difference. I also used G64 p0.01 makes no difference
if you look at the images you can see the faceting lines, they all measure around 1.5mm between each line.
any thoughts?