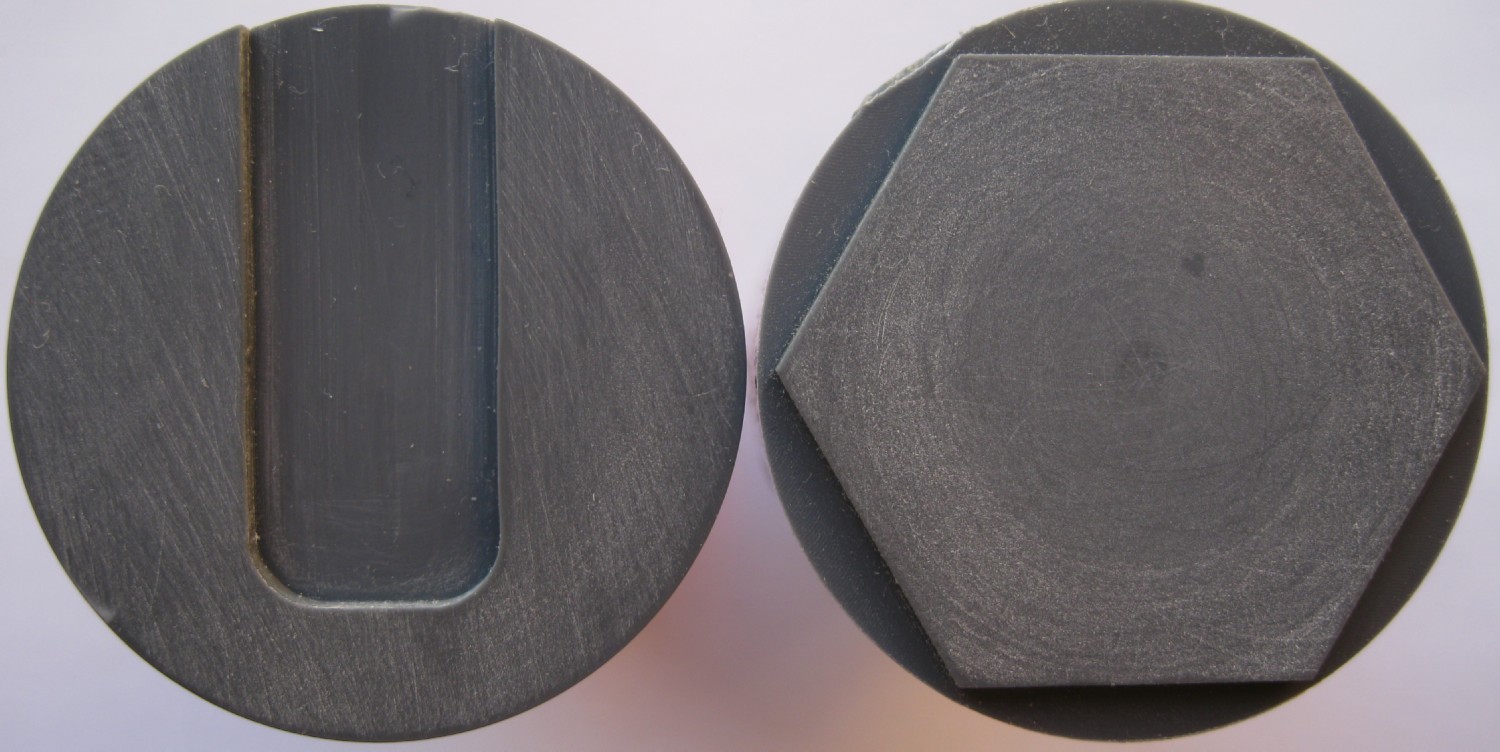
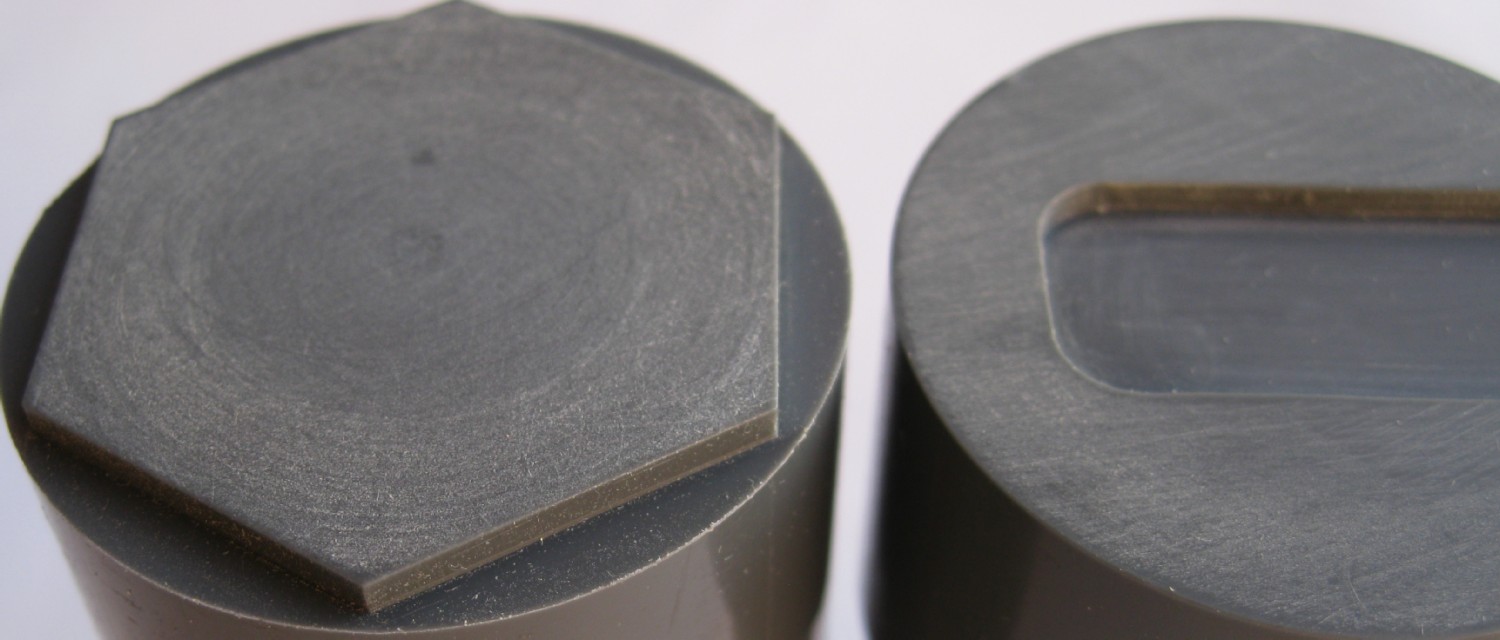
Good Progress on the Lathe. The software side is about done - some refinements here and there, but in all it works well.
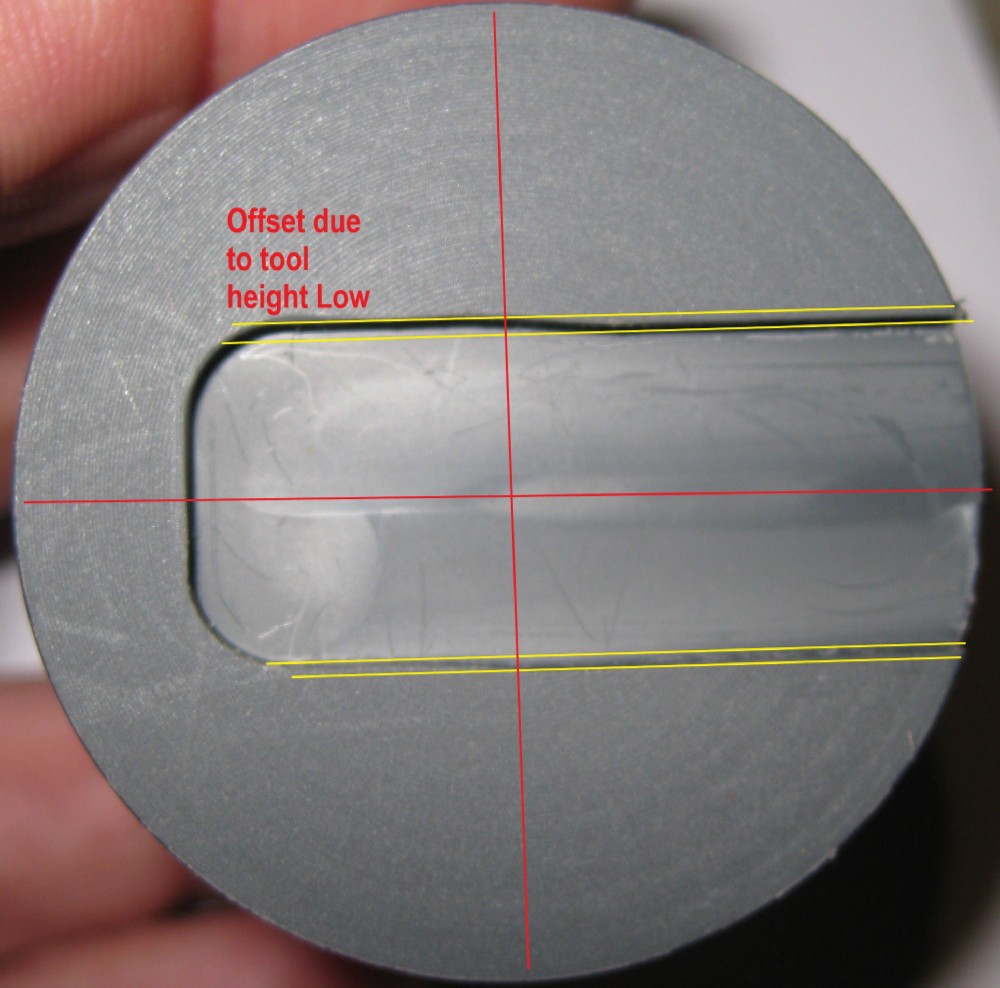
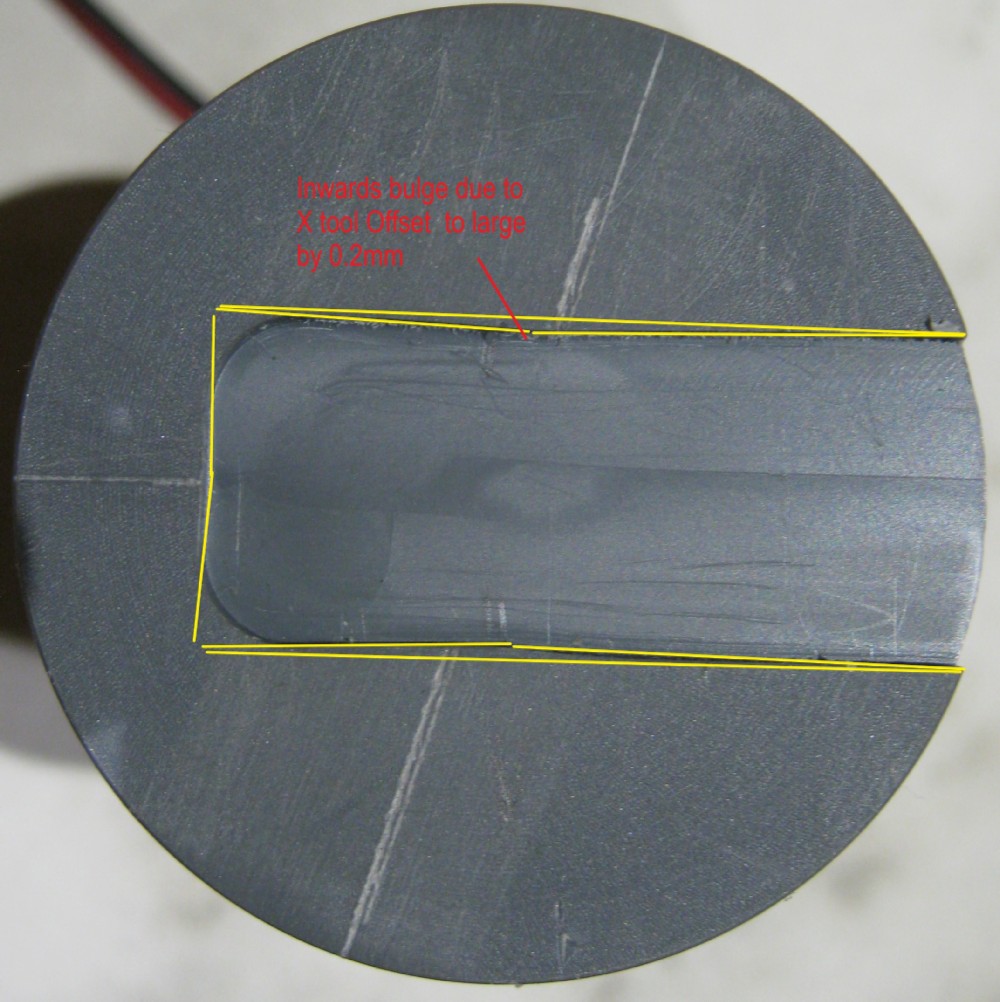
I have done some machining trials and the emphasis now shifts to the mechanics, setting all tool offsets correctly, getting the live tool centre height spot on with spindle height, else edges such as those of the U shapes in the photos end up offset - the X (G54) offset for the live tool is critical and has a huge effect when machining on the stock face where the live tool centre approaches the lathe spindle centre. At that point there are large C axis Theta changes for very small X axis changes. For the U, when C is near 90deg, incorrect X offsets result in bowed cut lines, etc. My X axis home sensor - a Hall effect sensor, is inadequate - repeated home to a fixed point shows up to 0.2mm variations, so a new home sensor is needed.
The C axis encoder - a magnetic encoder, is also poor - there seems to be a nonlinearity in the pulse output train, as though the excitation magnet is not rotating about its centre. Also, the encoder provide 1024 pulses ( 4096 edges) which is 0.08deg - that with a 3 edge deadband and a 1 edge repeatability gives around 0.3deg accuracy,, which is not great for a C axis. Looking for a 2000pulse Optical encoder now...
This shows the error due to incorrect tool height - to low by 0.2mm
This bulge is due to the X offset (G54) being 0.21mm to much
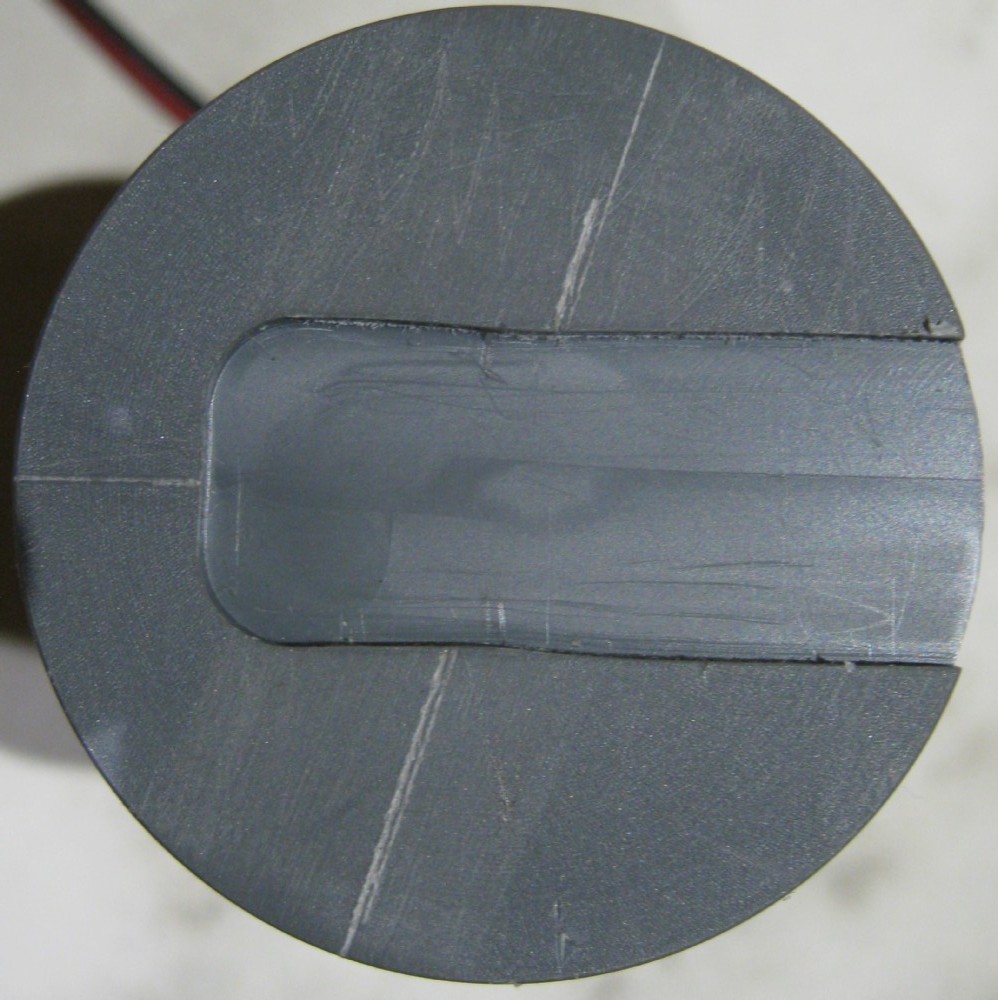
Same as above, but without the yellow lines
After setting tool height and X offset almost correct..