Bridgeport Torq-Cut TC4G Retrofit

More
5 years 9 months ago - 5 years 9 months ago #195845 by chopper79
I am excited to work on the tool change code.

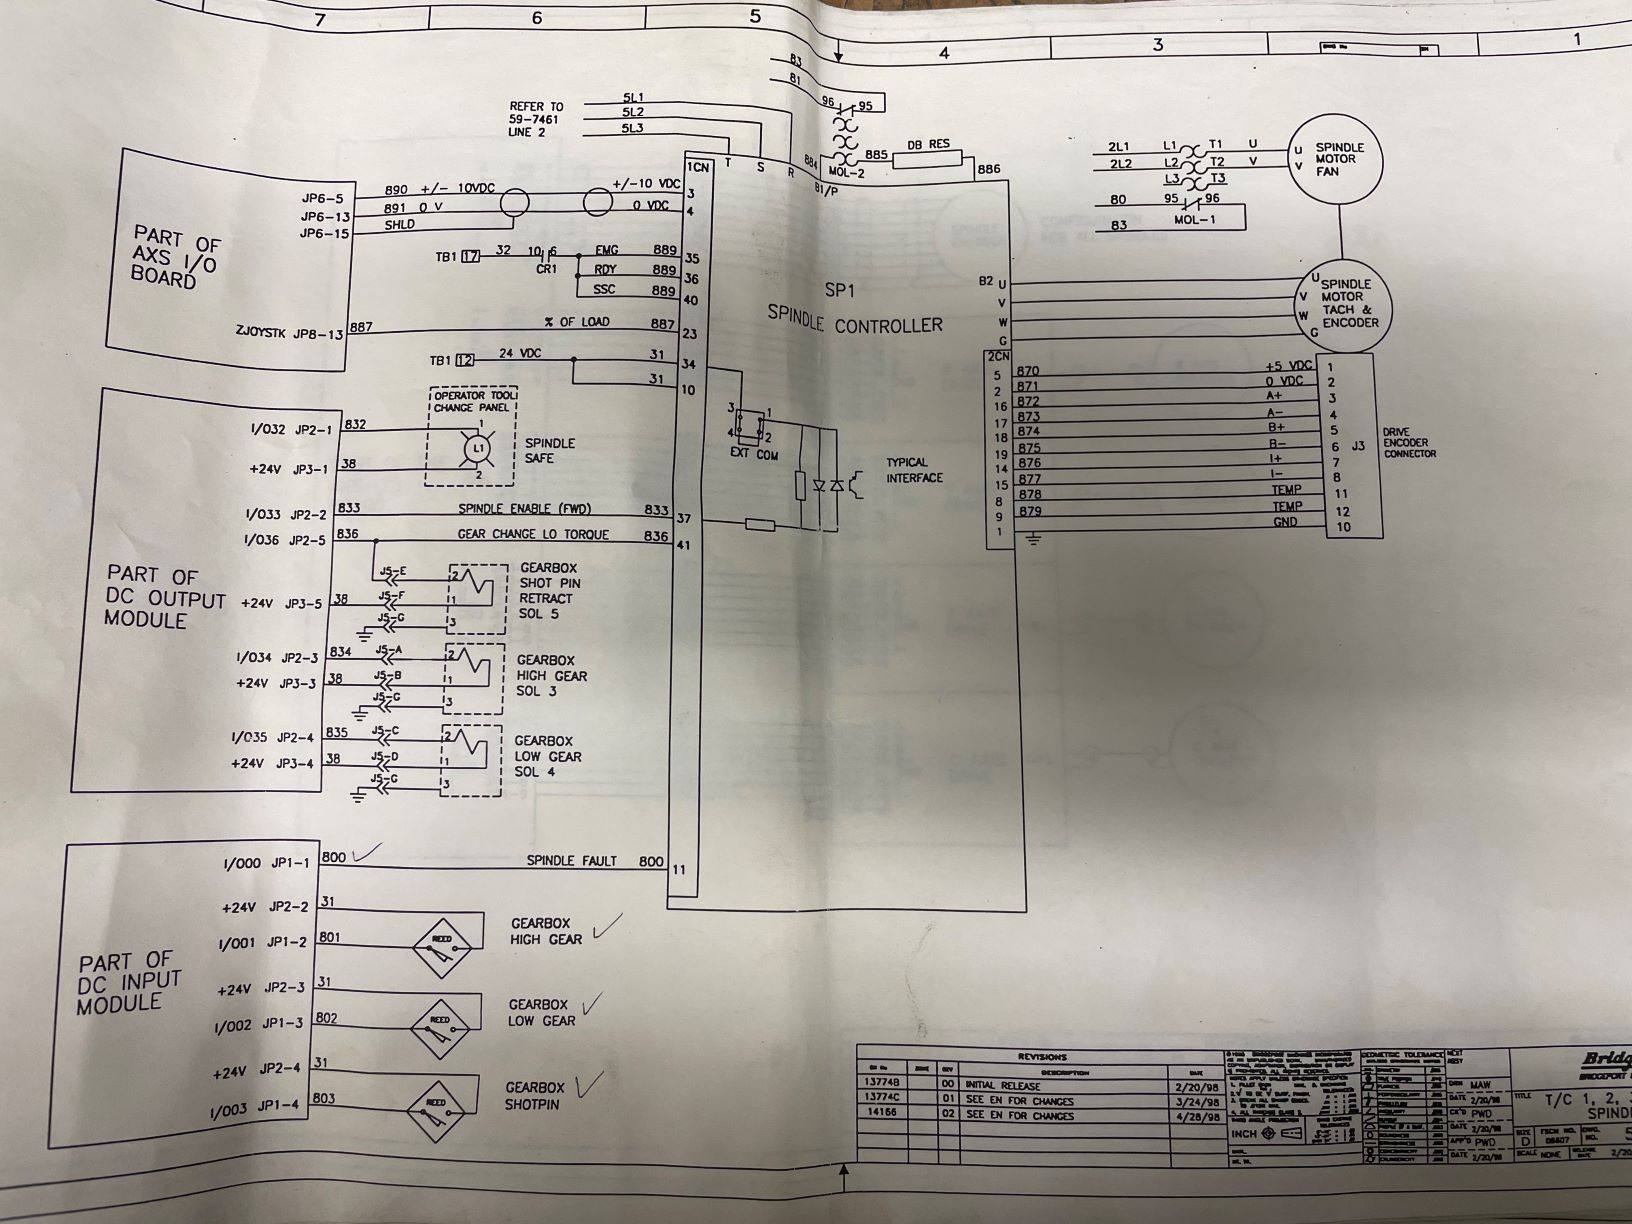
Need to first figure out how they are orienting the spindle as the machine did not utilize the orientation input on the vfd. I am thinking they utilized the torque limit mode (Pin 41) and fwd input (pin37). There is no sensor for it also, so it seem the vfd is put into incremental or absolute and then moved X amount of degrees from the index mark on the encoder. The orientation complete is also not utilized on the vfd so this makes me think that the controller had a programmed angle then when that was achieve, then the spindle locked and when no rotation was seen the tool change proceeded.

Just guessing here...


Last edit: 5 years 9 months ago by chopper79.

Please Log in or Create an account to join the conversation.

More
5 years 9 months ago #195846 by Michael
I have only gotten as far as to hook up the tool changer components to relays after deconstructing the boards they used to perform the changes. Have it all working individually but have not tackled the sequence yet.
Found a bad spindle bearing. Would love to know what the max speed I could get out of a spindle rebuild is. My 8k is cool but would be much happier in 12-16k range. Could end up going to a all in one motorized spindle if the price is similar.
Spindle wirong diagram looks similar. I don't believe I had an orient from the drive. Will need to be oriented off index.
The following user(s) said Thank You: chopper79

Please Log in or Create an account to join the conversation.

More
5 years 9 months ago - 5 years 9 months ago #195847 by chopper79
Yeah that is what I was figuring as well when it comes to orientation. Could always run a couple more wires and get orientation and orientation completed signals. Then reprogram the vfd a little bit so it looks for the input and then send the output.

I hope mine is 8k, so far it appears to be 6k, Will know more when I get the machine fired up again and look in the drive constants. Motor is capable of 8k based on data plate and manual but the bearings in the spindle motor are only rated for about 8k or a little less based on NTN website.

We shall see here someday soon....
Last edit: 5 years 9 months ago by chopper79.

Please Log in or Create an account to join the conversation.

More
5 years 9 months ago #195848 by Michael
Did you already have the bearing numbers or find them somewhere? I am very interested in what mine are but haven't dug into it or found information readily available.

Please Log in or Create an account to join the conversation.

More
5 years 9 months ago #195862 by chopper79
Spindle motor bearings are listed on the motor frame. I have not had to repair the spindle itself yet.

Spindle motor bearings are:

(1) 6308M2ZZAC3P6Q
(1) 6208M2ZZAC3P6Q

Please Log in or Create an account to join the conversation.

More
5 years 8 months ago - 5 years 8 months ago #197674 by chopper79
I am in need of some help here.

I am in the beginning stages of testing the LCNC config with the machine before I button up the last of the wiring and give y'all update pictures. The issue I am having is as followed:

1) Can not get any axis to move without a following error. I have tried many different encoder scale values based on the information I can find.

2) The jog velocity never changes when trying to move also. If control is set to 10 IPM the axis just rotates slow before the following error. If I change the jog to 600 IPM the axis rotates at the same slow speed before the following error. Almost like it is not getting a +/- 10v signal.

3) Have an issue with the spindle as well but I will save that one until the axis can move correctly.

The servo motor part number = SGMG-13A2AB which means it has a 8192 pul/rev from what I can tell. Also the ball screw on the machine is a 12mm pitch which should equate out to an encoder scale of ~ 69,358.0 unless my math has failed me which is possible.

I have attached the servo spec sheet and my config files.

If anybody has any ideas on this issue that would be great. Also if it matters the config was setup using PNCconf.
Last edit: 5 years 8 months ago by chopper79.

Please Log in or Create an account to join the conversation.

Time to create page: 0.422 seconds
Powered by Kunena Forum