

- Posts: 189
- Thank you received: 44
Bridgeport Torq-Cut TC4G Retrofit
5 years 8 months ago - 5 years 8 months ago #200471
by chopper79
Replied by chopper79 on topic Bridgeport Torq-Cut TC4G Retrofit
Update...
I removed epilog from my ini file and LCNC launches with no errors. Testing the gear change and it works well (couple small changes I want to do). Only issue now is the S value is not passed through to the spindle.
Command M3s1000 (program or mdi)
Gear changes
No commanded rpm value passed through
I am thinking this is due to the epilog being removed, but with it there LCNC does not launch. So now that most of it works I need to see what is not happy when the epilog is placed back into the ini file. Maybe it is something in my subroutine just not sure at the moment.
Any suggestions let me know please
I removed epilog from my ini file and LCNC launches with no errors. Testing the gear change and it works well (couple small changes I want to do). Only issue now is the S value is not passed through to the spindle.
Command M3s1000 (program or mdi)
Gear changes
No commanded rpm value passed through
I am thinking this is due to the epilog being removed, but with it there LCNC does not launch. So now that most of it works I need to see what is not happy when the epilog is placed back into the ini file. Maybe it is something in my subroutine just not sure at the moment.
Any suggestions let me know please
Last edit: 5 years 8 months ago by chopper79.
Please Log in or Create an account to join the conversation.

5 years 7 months ago - 5 years 7 months ago #200948
by Michael
Replied by Michael on topic Bridgeport Torq-Cut TC4G Retrofit
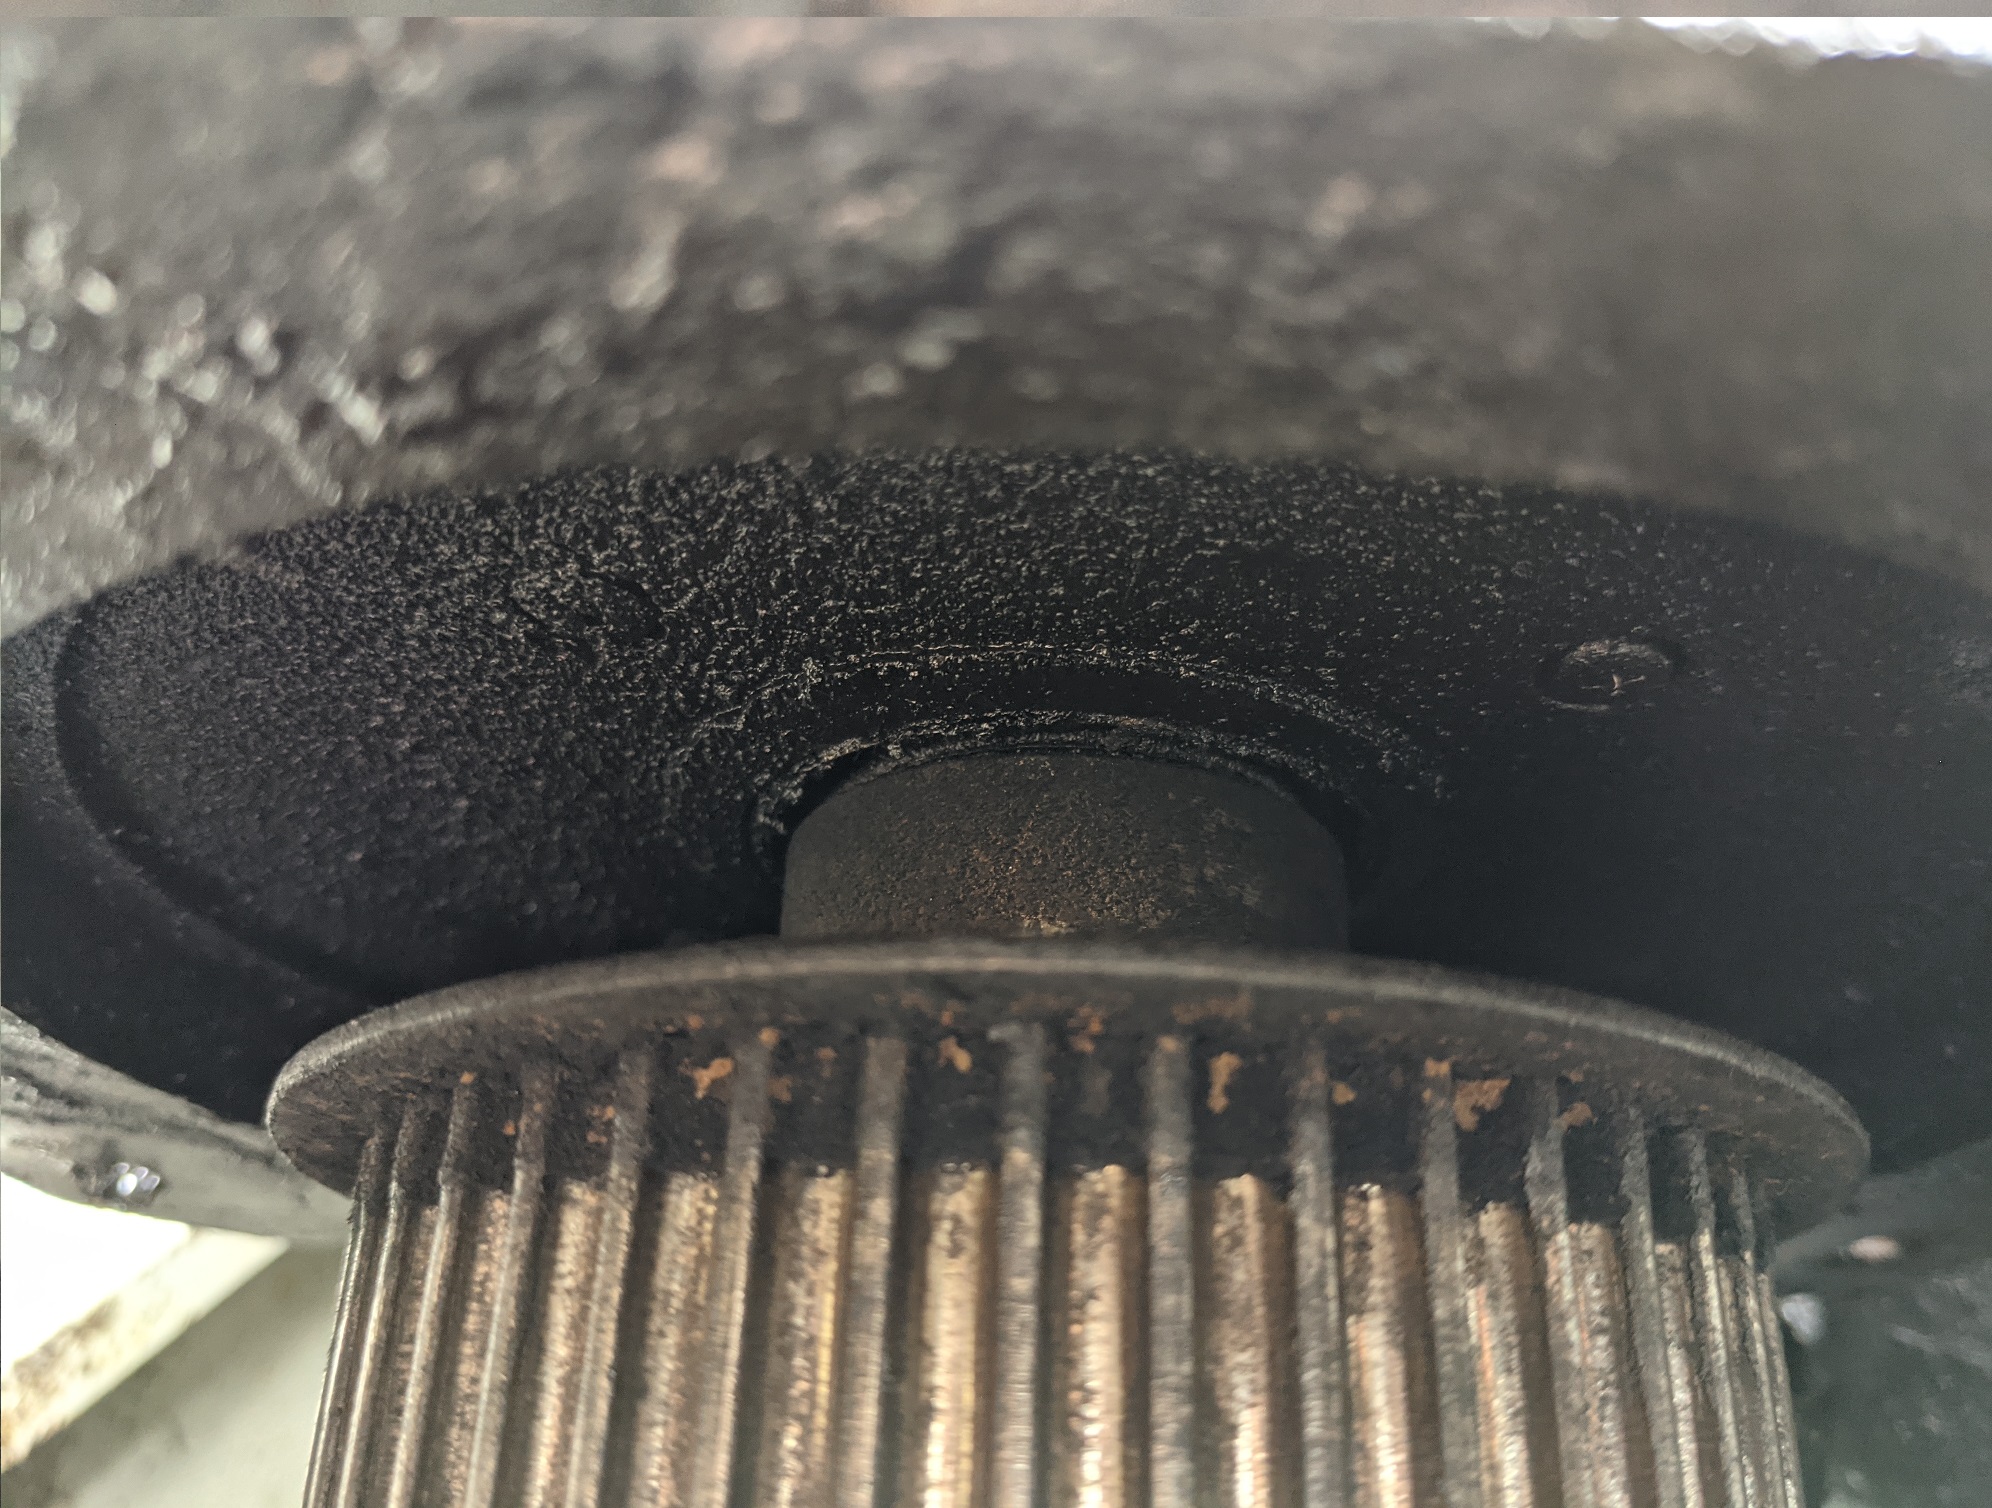
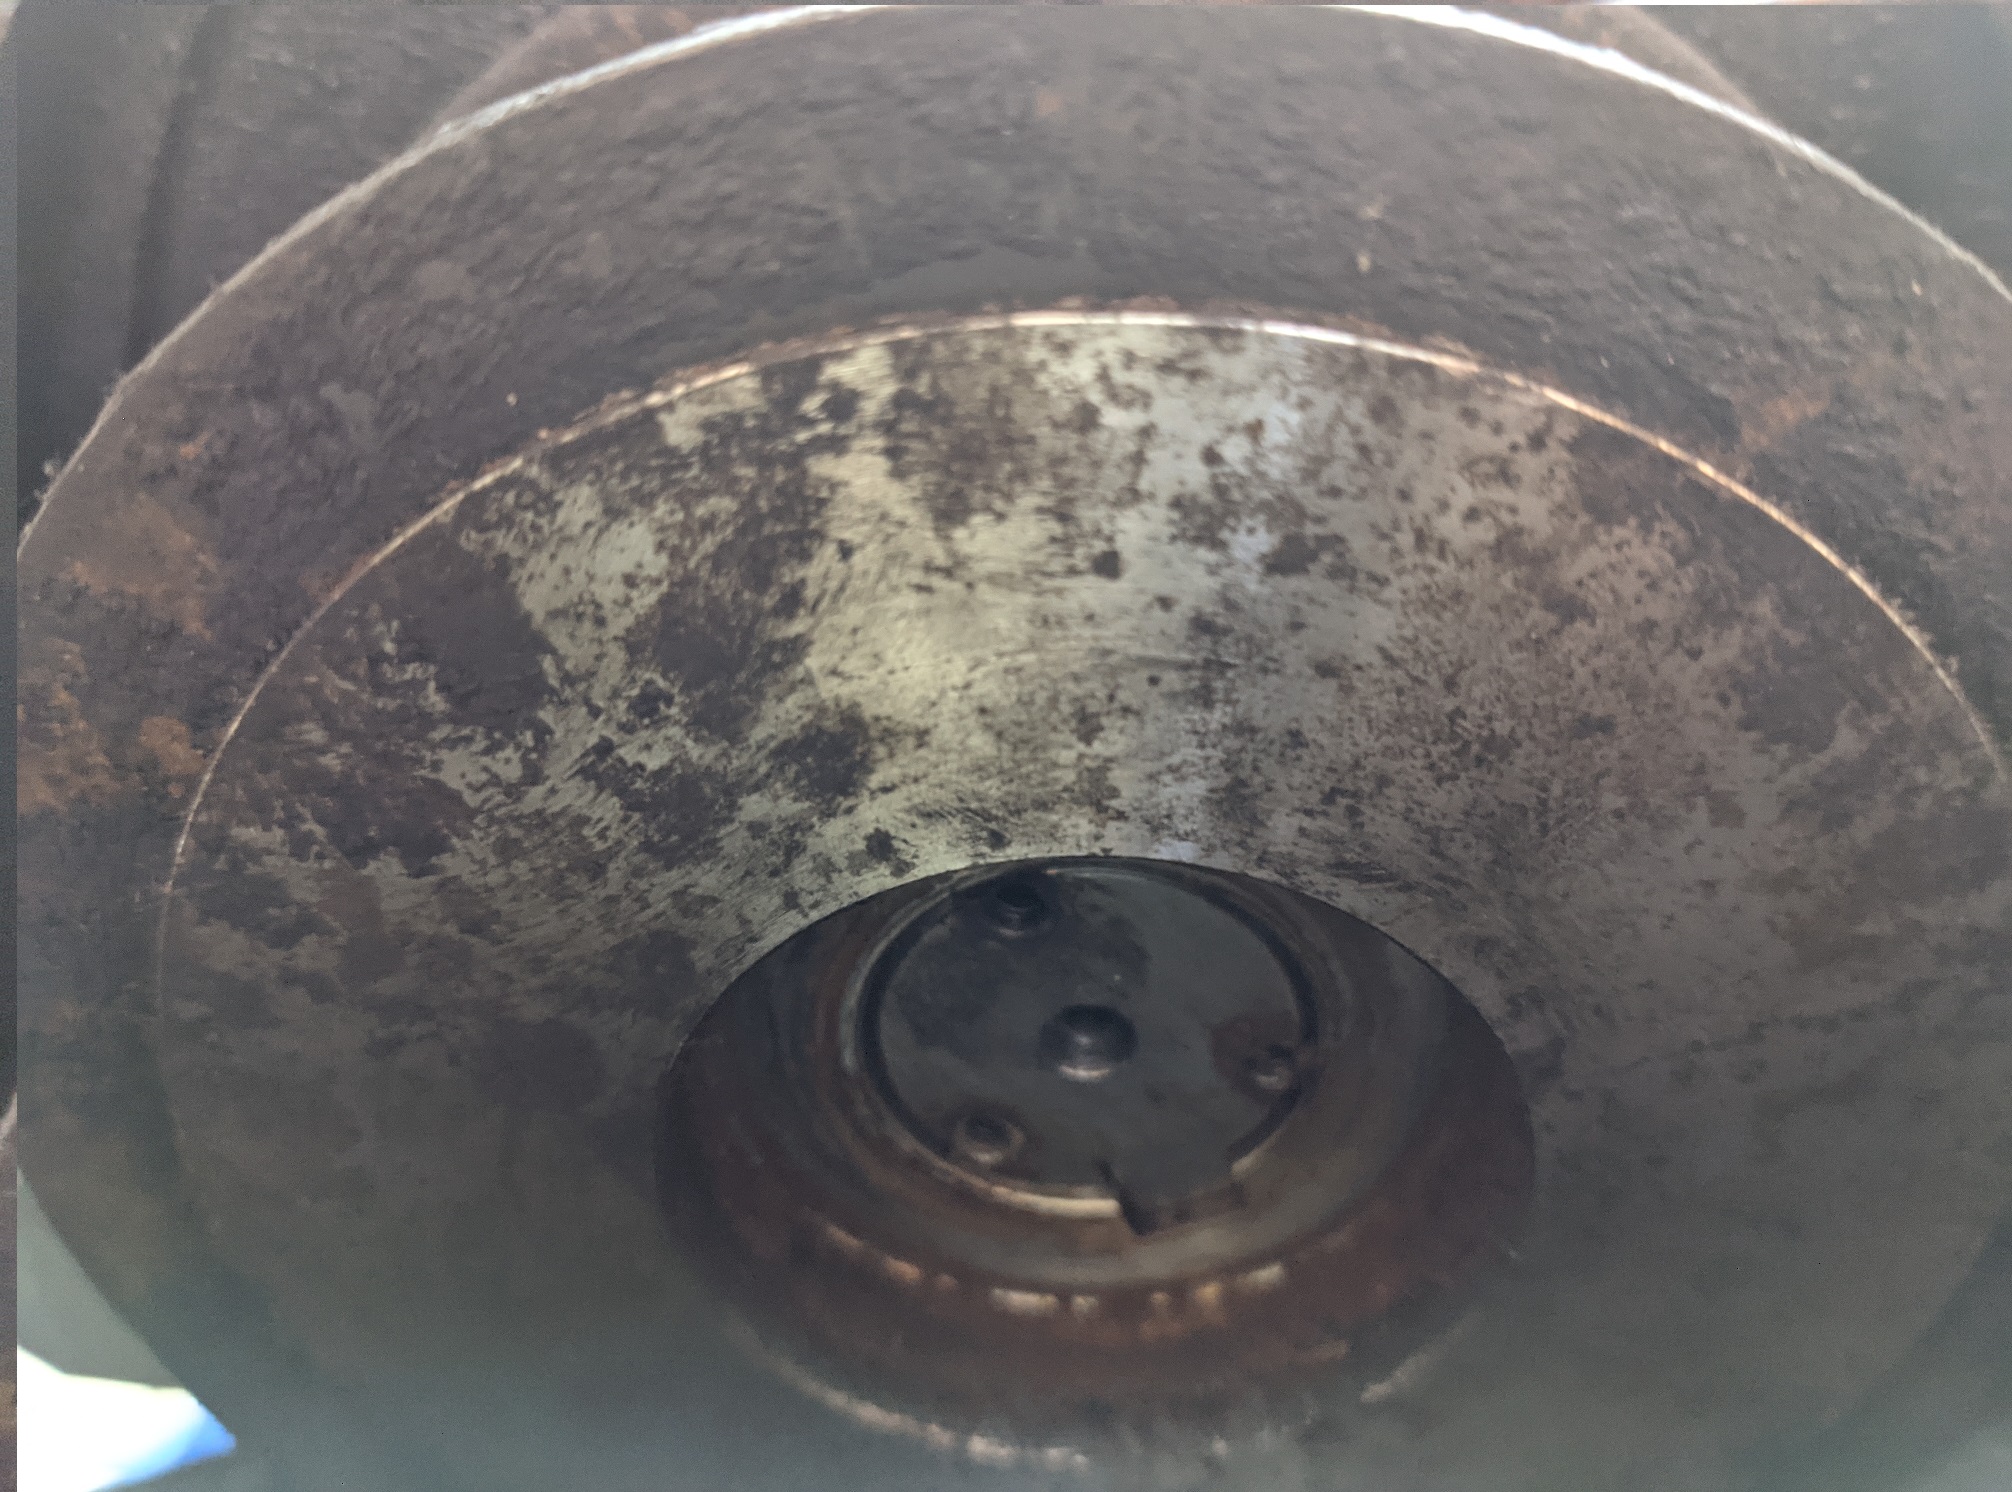
When you rebuilt your spindle motor, how was your pulley configured on the shaft and how did you get it off the shaft. I have attached pictures of mine. It had 3 small screws holding an end camp to the shaft. There is a collar between the pulley and motor casing that seems to keep the pulley in place. Before I start pulling on this or applying heat I wanted to make sure there is nothing I am missing. This appears to be a press fit and the axial offset is handled by the collar and end plate.
Last edit: 5 years 7 months ago by Michael.
Please Log in or Create an account to join the conversation.
5 years 7 months ago #200949
by chopper79
Replied by chopper79 on topic Bridgeport Torq-Cut TC4G Retrofit
Yeah that was a fun one...
1) Remove the (3) screws and end cap
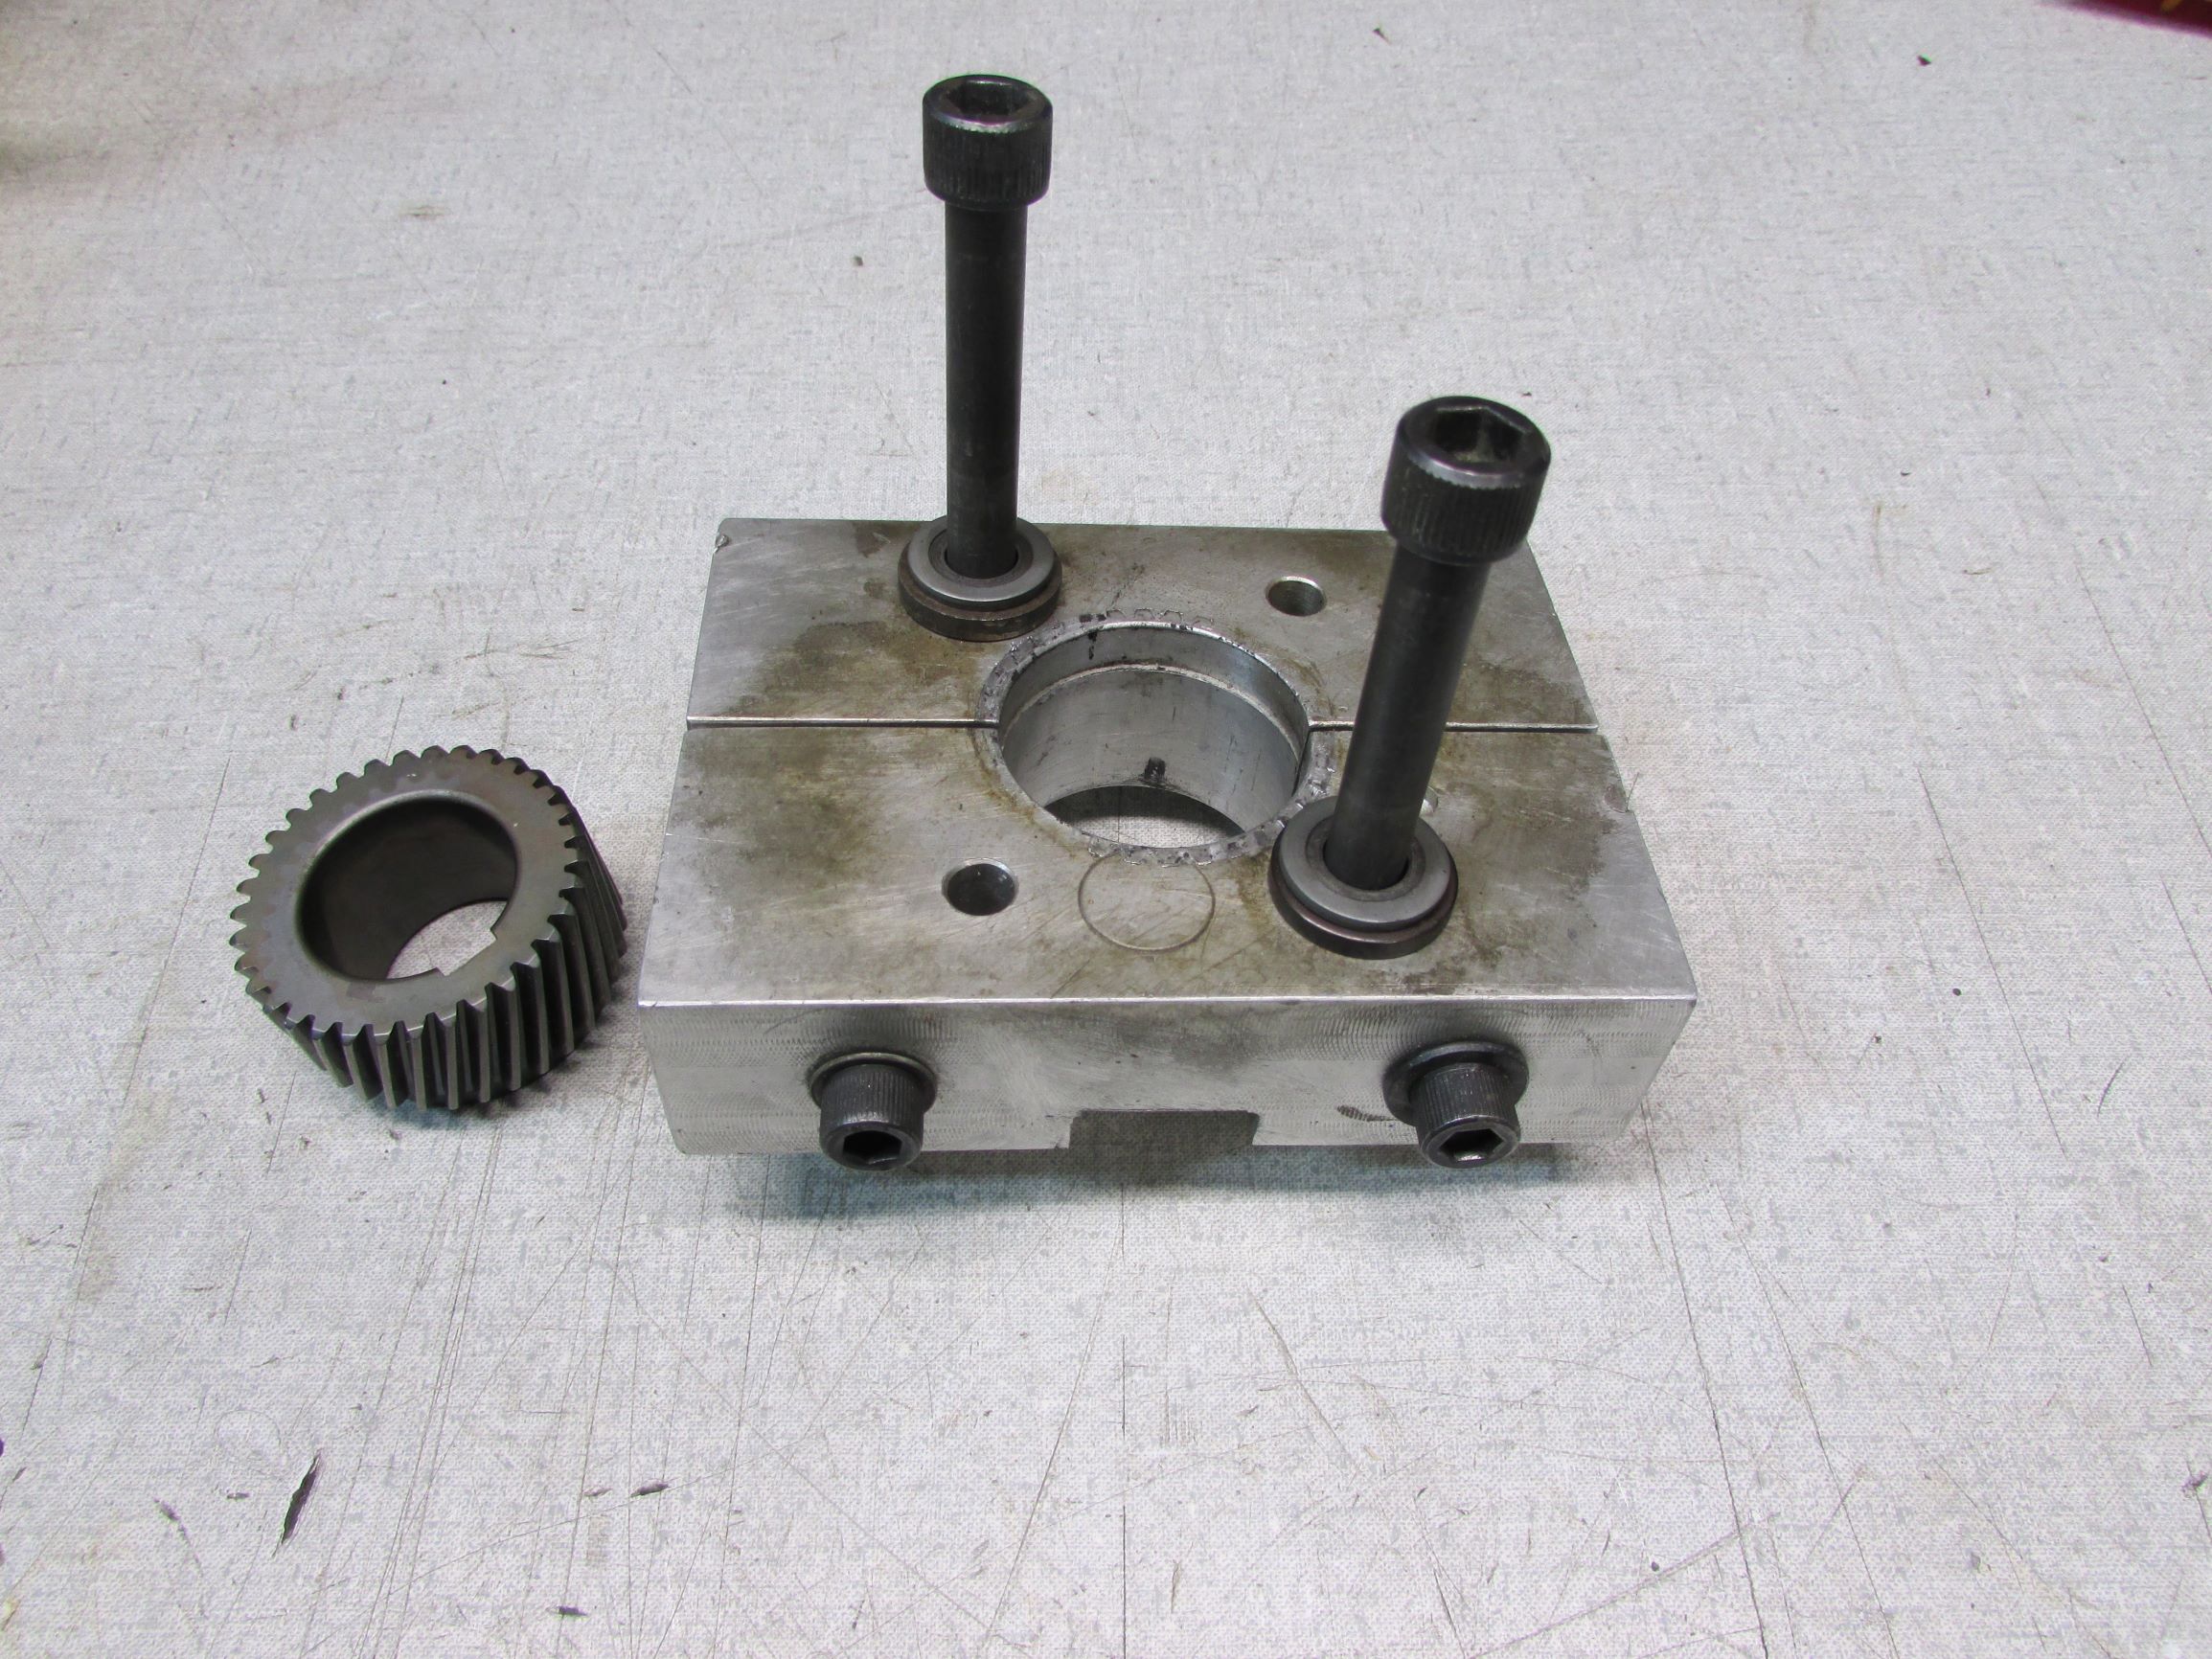
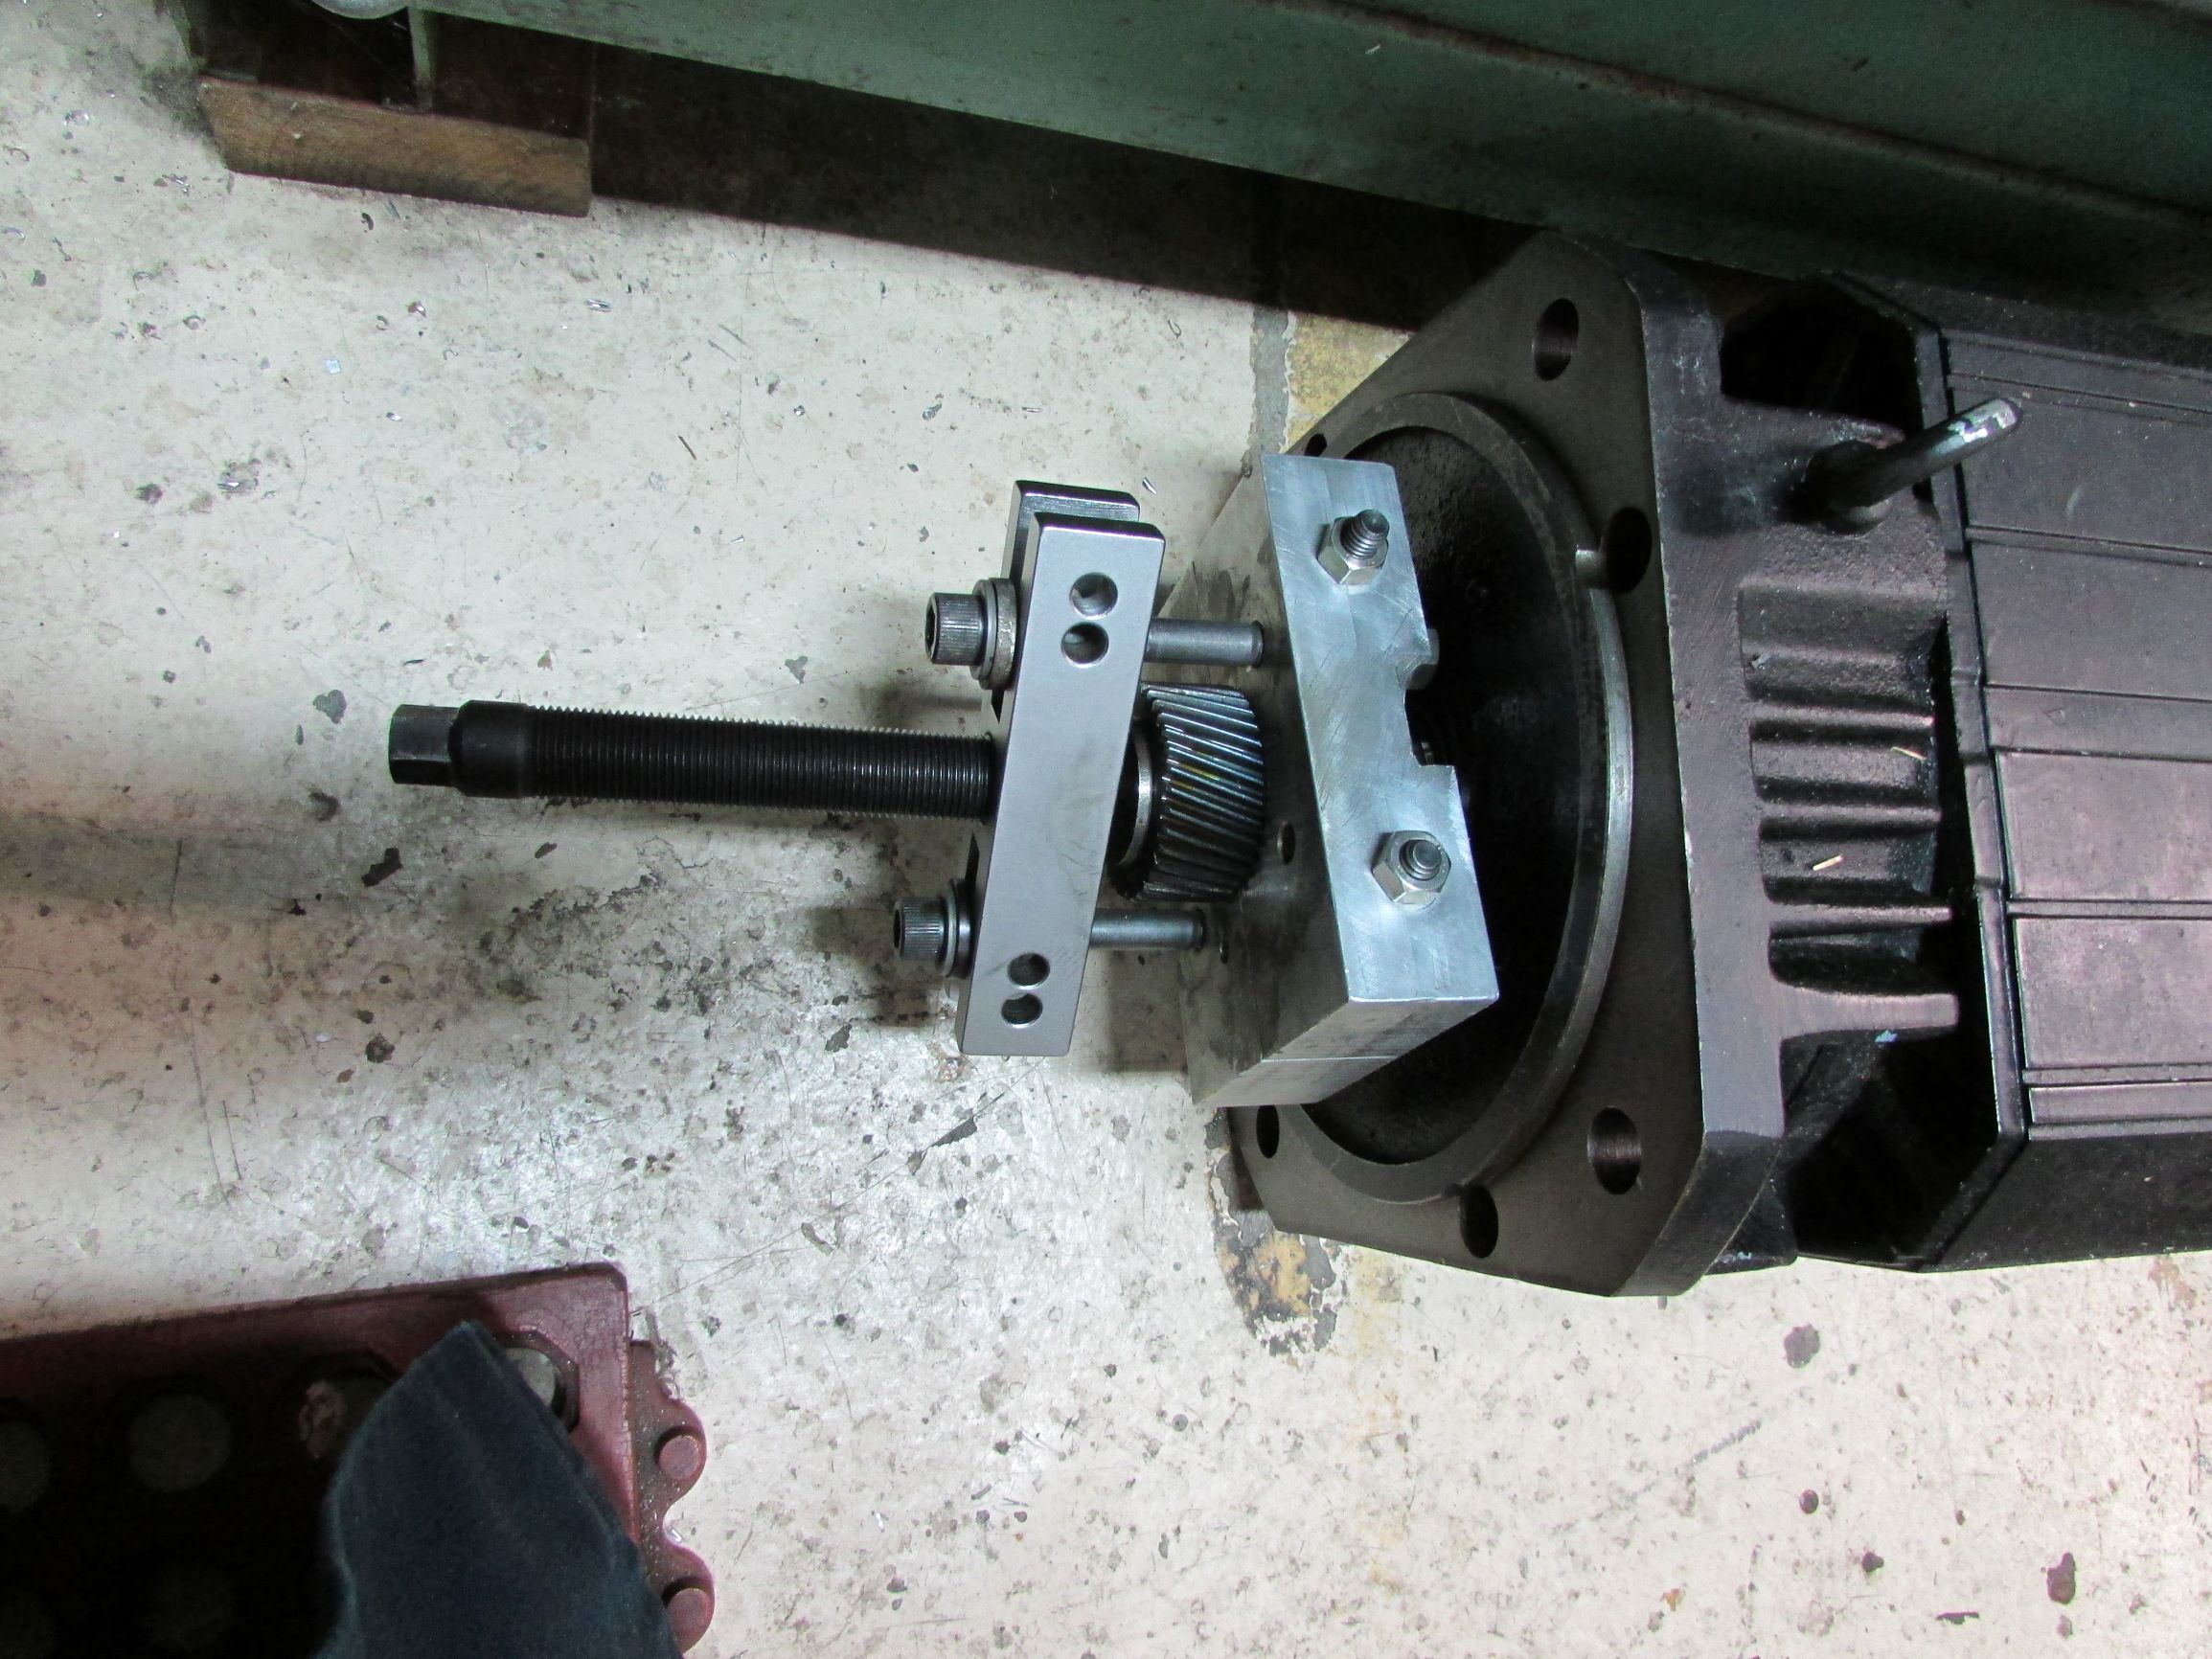
2) I had to make a puller setup for it
3) The gear is shrink fit not press fit
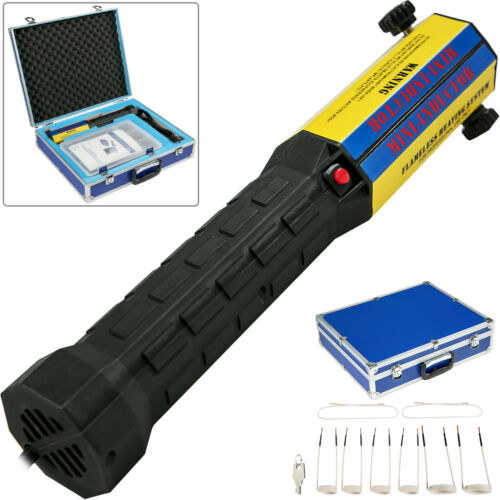
4) Used an induction heater to heat it then remove
5) Used an induction heater to heat for installation
Blow torch would work as well I would think, but would allow the heat to soak into the motor by the time it was to temperature. I purchased one of those hand held induction heaters from ebay and it works awesome! I had to get the gear up to ~ 500°F to remove and install which took about 45 sec with the induction heater.
The collar on there is just a spacer so the offset distance is correct for proper gear meshing.
1) Remove the (3) screws and end cap
2) I had to make a puller setup for it
3) The gear is shrink fit not press fit
4) Used an induction heater to heat it then remove
5) Used an induction heater to heat for installation
Blow torch would work as well I would think, but would allow the heat to soak into the motor by the time it was to temperature. I purchased one of those hand held induction heaters from ebay and it works awesome! I had to get the gear up to ~ 500°F to remove and install which took about 45 sec with the induction heater.
The collar on there is just a spacer so the offset distance is correct for proper gear meshing.
Please Log in or Create an account to join the conversation.
5 years 7 months ago - 5 years 7 months ago #200950
by chopper79
Replied by chopper79 on topic Bridgeport Torq-Cut TC4G Retrofit
Shoot... After I posted your pictures showed up. Do you have a transmission? Is that the spindle motor or the transmission output shaft?
I would use a standard pulley puller and an impact gun for that setup. Should need a little heat and some penetrating fluid maybe.
I am beginning to wish I did not have the transmission... I need to make it shift gears and I am no good at code..haha
I would use a standard pulley puller and an impact gun for that setup. Should need a little heat and some penetrating fluid maybe.
I am beginning to wish I did not have the transmission... I need to make it shift gears and I am no good at code..haha
Last edit: 5 years 7 months ago by chopper79.
Please Log in or Create an account to join the conversation.
5 years 7 months ago #200965
by Michael
Replied by Michael on topic Bridgeport Torq-Cut TC4G Retrofit
Yeah I realized you have the transmission also. But technically the motor shaft and whatever its attached to should be similar. I will give it some heat and see if we can get it to move. Also may make something like your puller. I don't have a puller that gets around the flanges on these pulleys. I could just put the torch next to the pulley and spin the spindle at 10 rpm until it falls off!?!
If you remove your transmission the spindle motor should need an adapter plate (maybe able to reuse the one on the transmission) to mount to the head and a drive pulley and be good to go, 8000rpm 32 ft lbs torque. Unless you are tapping or doing all your work in steel with large cutters I don't see the need for the transmission. My spindle is shot so I am exploring a rebuild or new spindle made overseas with a higher rpm limit. All my work is small cutters in aluminum so I can afford to loose some power.
I looked at your S remap stuff but am no good at code. I would love to see what you did for the tool change remap though. I am waiting on a sensor and will be trying to implement mine shortly.
If you remove your transmission the spindle motor should need an adapter plate (maybe able to reuse the one on the transmission) to mount to the head and a drive pulley and be good to go, 8000rpm 32 ft lbs torque. Unless you are tapping or doing all your work in steel with large cutters I don't see the need for the transmission. My spindle is shot so I am exploring a rebuild or new spindle made overseas with a higher rpm limit. All my work is small cutters in aluminum so I can afford to loose some power.
I looked at your S remap stuff but am no good at code. I would love to see what you did for the tool change remap though. I am waiting on a sensor and will be trying to implement mine shortly.
Please Log in or Create an account to join the conversation.
5 years 7 months ago - 5 years 7 months ago #200972
by chopper79
Replied by chopper79 on topic Bridgeport Torq-Cut TC4G Retrofit
I looked to remove the transmission, but the motor will not fit in the location (mounting flange is to wide). so I put the transmission back on...
I am going another direction then remapping S. It works minus not passing the speed command back out. I am in the process of implementing a comp file to do the transmission gear change right now.
1) I can get it to change to low gear, but not back to high gear when the speed is > xx.
2) The solenoid valves do not shut off after gear change to low
Need to do some more on the comp file to which is a major learning curve for me. Right now I need to get the comp file to provide a set rpm out during gear change. Currently it will keep the spindle rpm at the commanded value while changing the gear to low (s200 and it changes and grinds ). Need to do the following:
1) command speed (M3s200)
2) rpm drops to 11 rpm
3) gear changes
4) check for sensor status
5) ramp back up to commanded speed * the gear ratio
I may be in over my head right now but what the heck giving it a go anyway... :lol:
I am going another direction then remapping S. It works minus not passing the speed command back out. I am in the process of implementing a comp file to do the transmission gear change right now.
1) I can get it to change to low gear, but not back to high gear when the speed is > xx.
2) The solenoid valves do not shut off after gear change to low
Need to do some more on the comp file to which is a major learning curve for me. Right now I need to get the comp file to provide a set rpm out during gear change. Currently it will keep the spindle rpm at the commanded value while changing the gear to low (s200 and it changes and grinds
). Need to do the following:1) command speed (M3s200)
2) rpm drops to 11 rpm
3) gear changes
4) check for sensor status
5) ramp back up to commanded speed * the gear ratio
I may be in over my head right now but what the heck giving it a go anyway... :lol:
Last edit: 5 years 7 months ago by chopper79.
Please Log in or Create an account to join the conversation.
Time to create page: 0.297 seconds