My replacement probe arrived today along with a gift of a "VERS CM" from Verser. I did already have something wired up point to point on a proto board in a 3D printed box. This is way nicer so first of all thank you.
I've been using my fabricated Z touch probe and LED indicated edge detector along with my Shumatech DRO for determining edges and center position of the raw material. Once I got the feeds and speeds under control the second mount plate came out much better. No more high speed movement in the probe direction.
So far I've been using the modified tool change code and only the Z touch off button on the PSNG screen. The m6remap.ngc code uses the tool length in the tool table if it's non-zero or goes to the tool setter sensor to measure the tool if length is 0.
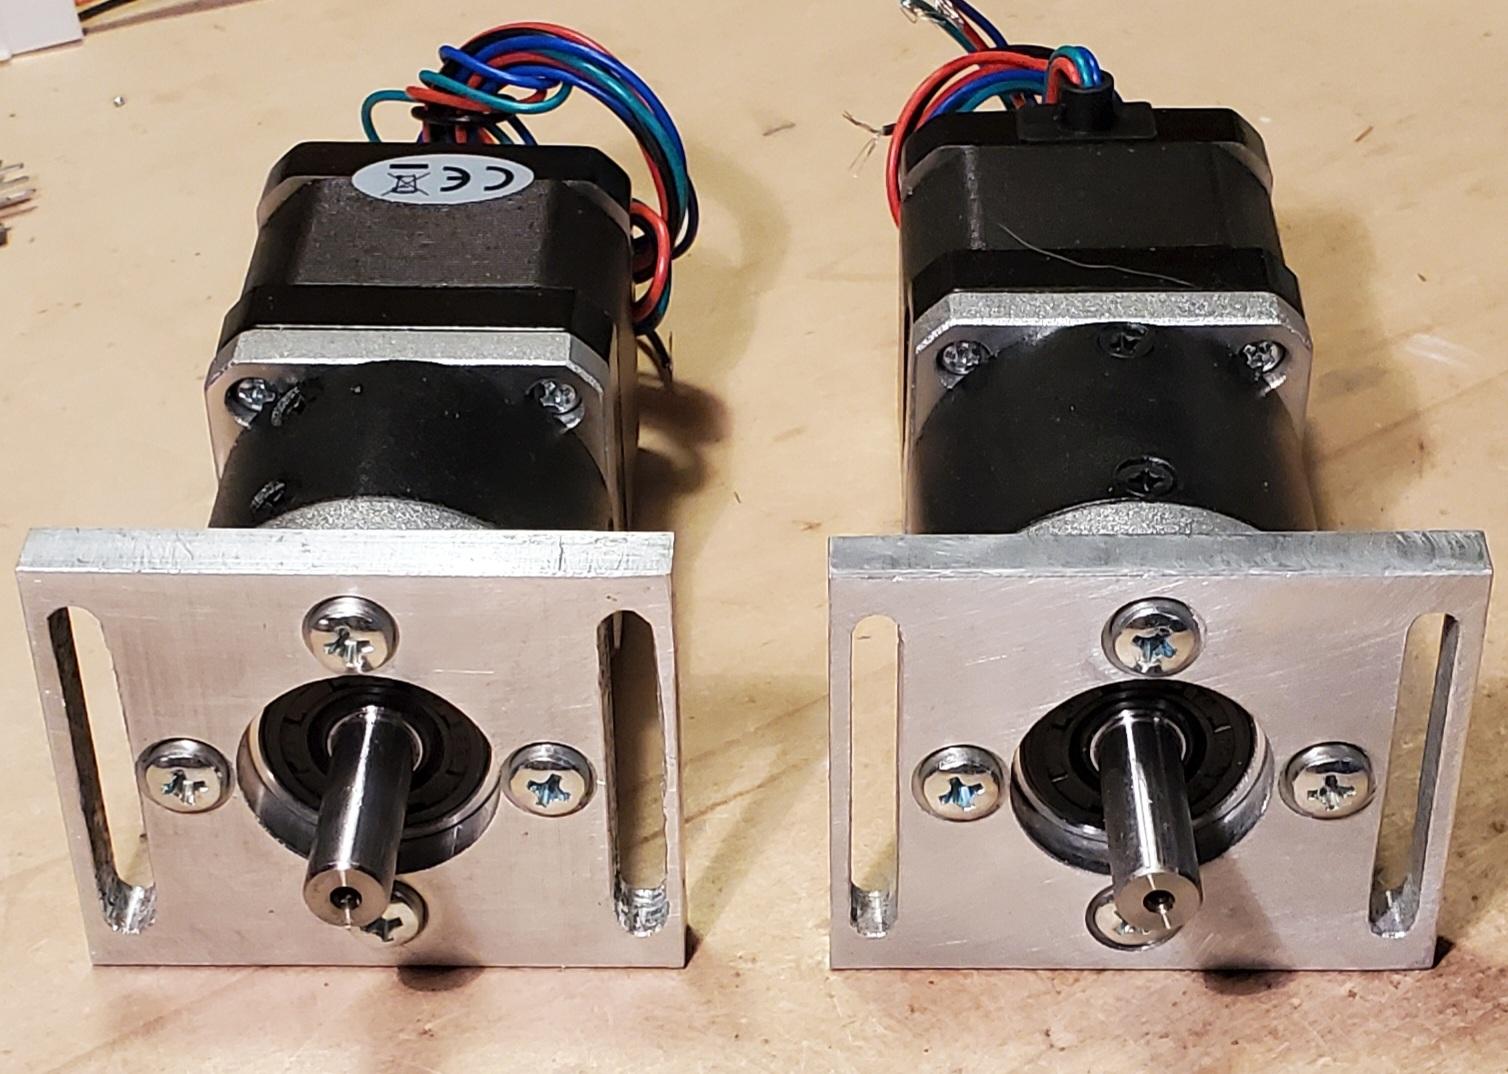
For example in the above photo I used a 0.125" 2 flute cutter for the slots, a center drill to create the hole positions, a 0.25" 2 flute cutter for the large holes and finally a 1/4" drill chuck with a 4.5mm drill for the holes. The center drill and 4.5mm holes were done first. Then the large hole. Finally the slots. Once I reduced the feed to 5 IPM instead of 14 IPM the slots turned out much better. The 4.5mm drill was probed with the tool setter each time. The others used the tool table so no probing. Nice!
An error in my drawing has the slots 1mm too close to one edge so I have to make new ones. Which is great because now I can use the replacement probe.
So why am I talking about all this? Well the checkbox for REMAP M6 doesn't really do anything anymore. So I've been looking into modifying the code so when checked a tool change will not only take the tool to the tool setter but will also install the length of the tool into the tool table. I'll rename it to be Measure Tool with M6.
I'm thinking the Button underneath the title should do "Measure Tool" with the tool number in the field that currently has the label TS Height. Or maybe leave that as Tool Setter Height value when tripped and add a box for tool #. The Work Piece height can just be the same as the other touch off button with the text filled with Machine Coordinate distance from 0.
I can't use the probe to determine the tool setter height since the probe trips before the tool setter does. Different spring strength.
Anyway. Enough of a ramble. More when I have something to show and the m6remap.ngc code is complete. Still all in the development state at the moment but at least it's usable.


 . Anyway I would like to slowly learn more and possibly upgrade probe_screen. This might be nice since there are some more panels that I would like to use (lathe macros for example) and it would be nice to be able to tune them for my needs.