OpenPnP with LinuxCNC via linuxcncrsh?

More
3 years 6 months ago #269998 by blazini36
Home switch is only valid during the actual homing procedure.

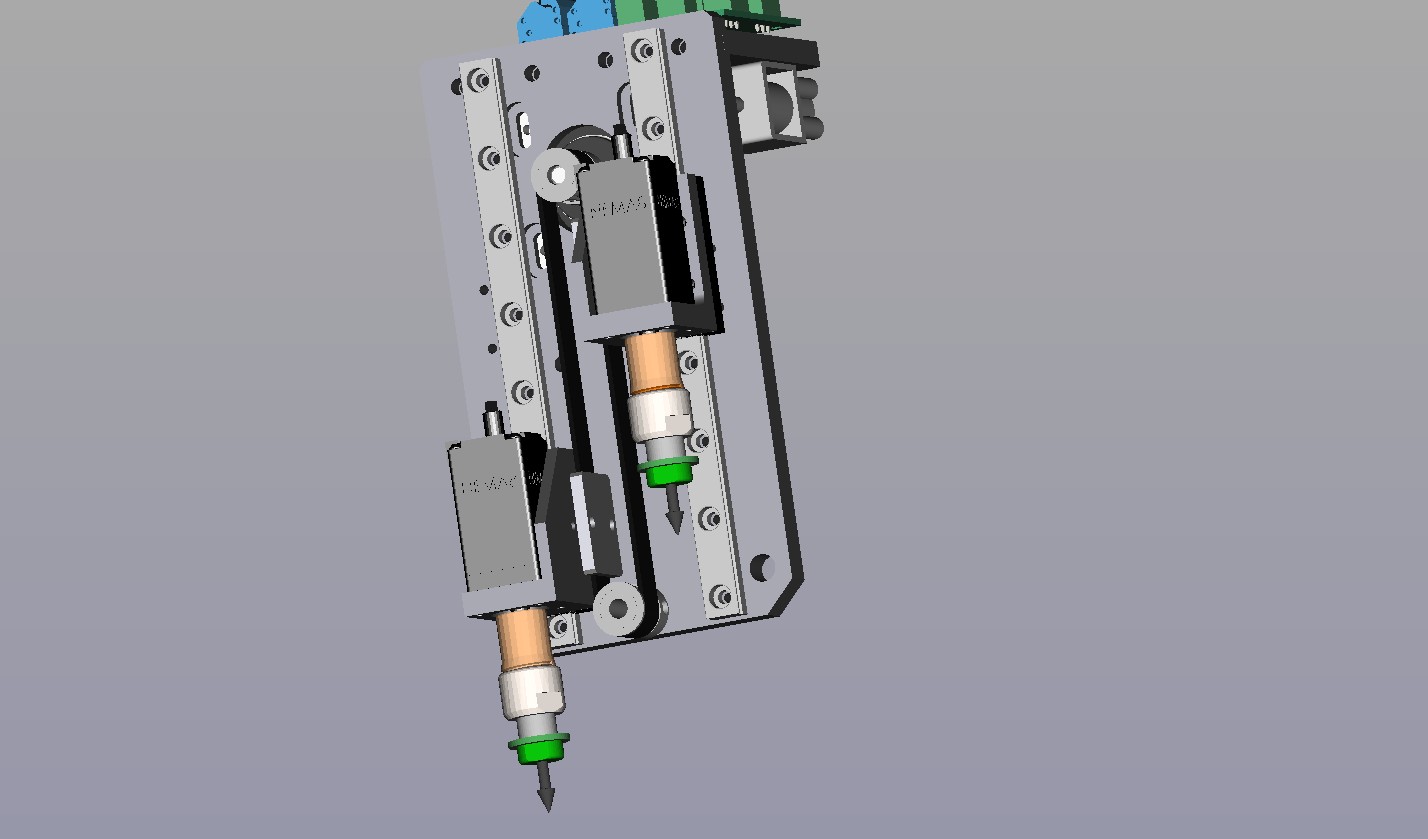
For a setup like the one I pictured several posts back, that's actually pretty easy to do. You just mount an inductive proximity switch on top of the base behind one of the gear racks. The switch will be active about 40% of the range which is probably fine.  That is a standard homing procedure, you set it up to travel towards the side that activates the switch, after it makes it backs off. If it's made when homing is started it only travels in the back-off direction.

That only works if you're setup mechanically allows it. Personally I'll be doing something like a 5-turn potentiometer and using the  HOME_ABSOLUTE_ENCODER = 2. The nice thing about this is it actually is an "absolute encoder" So it adds closed loop feedback for little coin.

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago #270010 by blazini36
Actually what I think I'll do is use one of these "high-torque" pots as the lower pulley shaft threaded in from the back.   www.digikey.com/en/products/detail/tt-el.../8146R5KL-25/4780742

Not much modification needed.

 
The following user(s) said Thank You: Clive S

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago #270043 by plhsystems
They're quite expensive, I think I'll stick with the switch :)

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago #270081 by blazini36
A $35 pot is not expensive considering the cost of everything else. I'm only using the "expensive" pot because it's serving as an axle for the lower pulley. The same type of pot in a lower duty version mounted freely to the stepper or lower pulley is alot less expensive.

But to each their own, this is what I'm doing.

Please Log in or Create an account to join the conversation.

More
3 years 5 months ago #271107 by Donb9261
One of the issues with homing using limit switches and steppers is there is no feedback from the motor to know the exact reference to the rotation of the motor. ie. an encoder Z marker. You can buy steppers with encoders but the cost is 3~4 times a standard stepper.

One way that could possibly help with you issue is to use a switch like this www.automationdirect.com/adc/shopping/ca..._actuator/csh121b-al

Metrol has been a round for a long time and I have worked with them hundreds of times. This switch is expensive @ $81 ea. But it has a 5um repeatability and a 2.8mm stroke. If you have a reasonable motor and driver you could allow a .02 or better home repeat position consistently.

There are just some things that hobby machines lack due to the expectation of solid accuracy for basically very small spend. You can cut corners in some things but cutting corners in accuracy is not a good idea.

The switch can act as both an end stop and a limit. You could avoid having a second opposing end stop by having this accurate switch and then setting soft limits once homed. As long as the reference is good and your code is set so that if the reference is lost the axis can ONLY move in the home direction you can save some money. Typically I do not use end stop switches in any builds. The clutter the machine and I would never use a $2 switch to use as my datum for the machine.

Although I recommend using the switch above, they offer small and slightly less accurate versions for much less.

Hope that helps.

PS - Control the speed at reference and acc/dec to ensure that when the reversal happens no steps are lost. As long as your overall backlash is less than .025mm or .001" you should be able to have solid control over your net accuracy.


Please Log in or Create an account to join the conversation.

More
3 years 5 months ago #271440 by iforce2d
I have been working on this recently.
github.com/iforce2d/linuxcnc-gcode-server

Please Log in or Create an account to join the conversation.

Time to create page: 0.452 seconds
Powered by Kunena Forum