Mach3 -> Camtronics -> Parallel P Replacement

More
5 years 7 months ago - 5 years 7 months ago #203628 by rdeeming
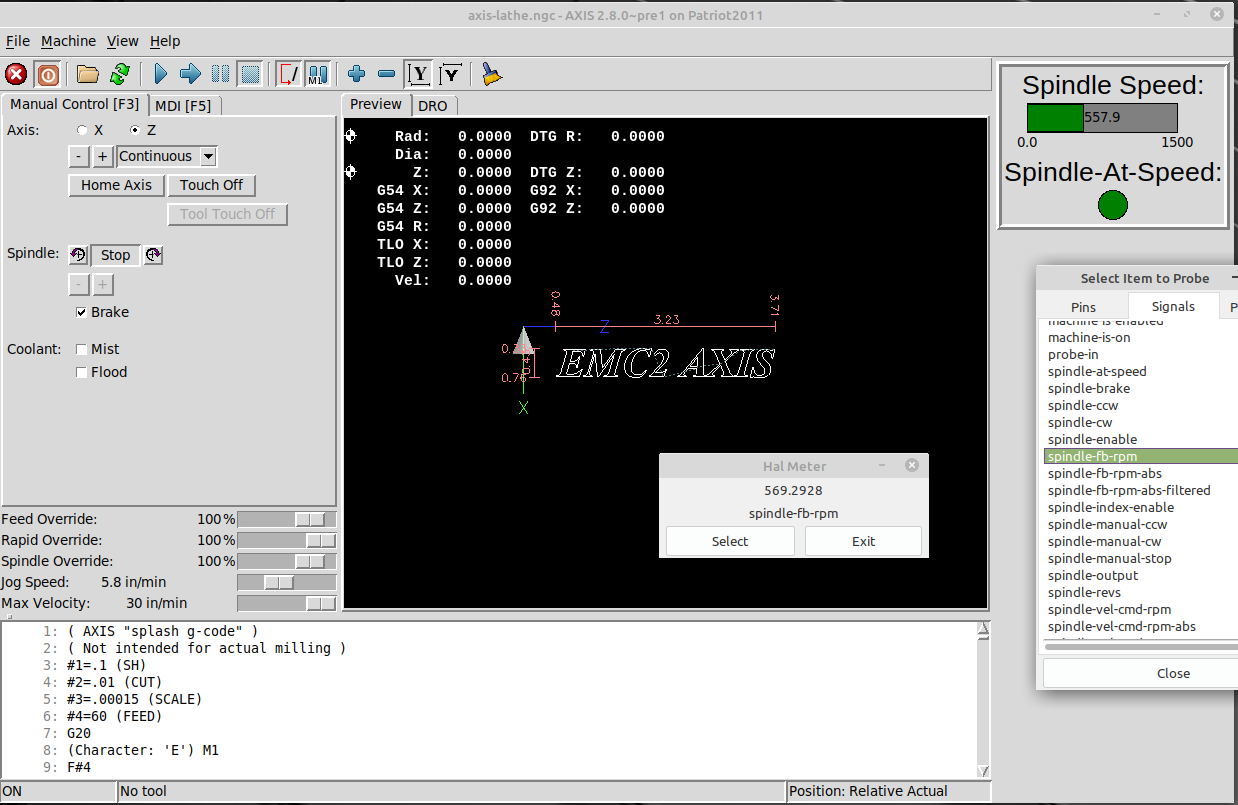
Got things a bit closer to the quest to do threading with the lathe.

Attached is the latest screen shot with RPMs showing.

Off to figure out how to get BobCad post processor to create gcode that linuxCNC appreciates using for thread operations.
Last edit: 5 years 7 months ago by rdeeming. Reason: sloppy typing

Please Log in or Create an account to join the conversation.
More
5 years 7 months ago #203841 by andypugh
Note that LinuxCNC does not use the spindle.0.speed-in pin for threading, it slaves the Z axis to spindle.0.revs

You will not be able to thread until you link the spindle.0.index-enable pin to the encoder index-enable.

Rather than persuade Bob CAD to thread for you, consider using G76 in the MDI window. It's a single line of G-code.
The only wrinkle is that you need to position the tool in the right place relative to the work first, as many of the parameters are relative to the starting position.
The following user(s) said Thank You: rdeeming, arvidb

Please Log in or Create an account to join the conversation.

More
5 years 7 months ago #204242 by rdeeming
Ran a test cutting 3/4" bar 6061-T6511 to have 3/4 16NF thread on 1" long.
I can't call it a success.... Ok the result is actually horrific.

With the tool offset .125" away from the outer edge and end of the bar.
G76 Z-1.125 P.063 I-.125 J.005 K.065 Q29 H1

It looks like I am not quite there getting the revolutions.
Looking at spindle-revs, marking a point I turned the spindle 20 revs and yes in fact it is considerably short.

When using Mach3 I had a single tigger (a magnet) attached to the lathe shaft recording one rotation.

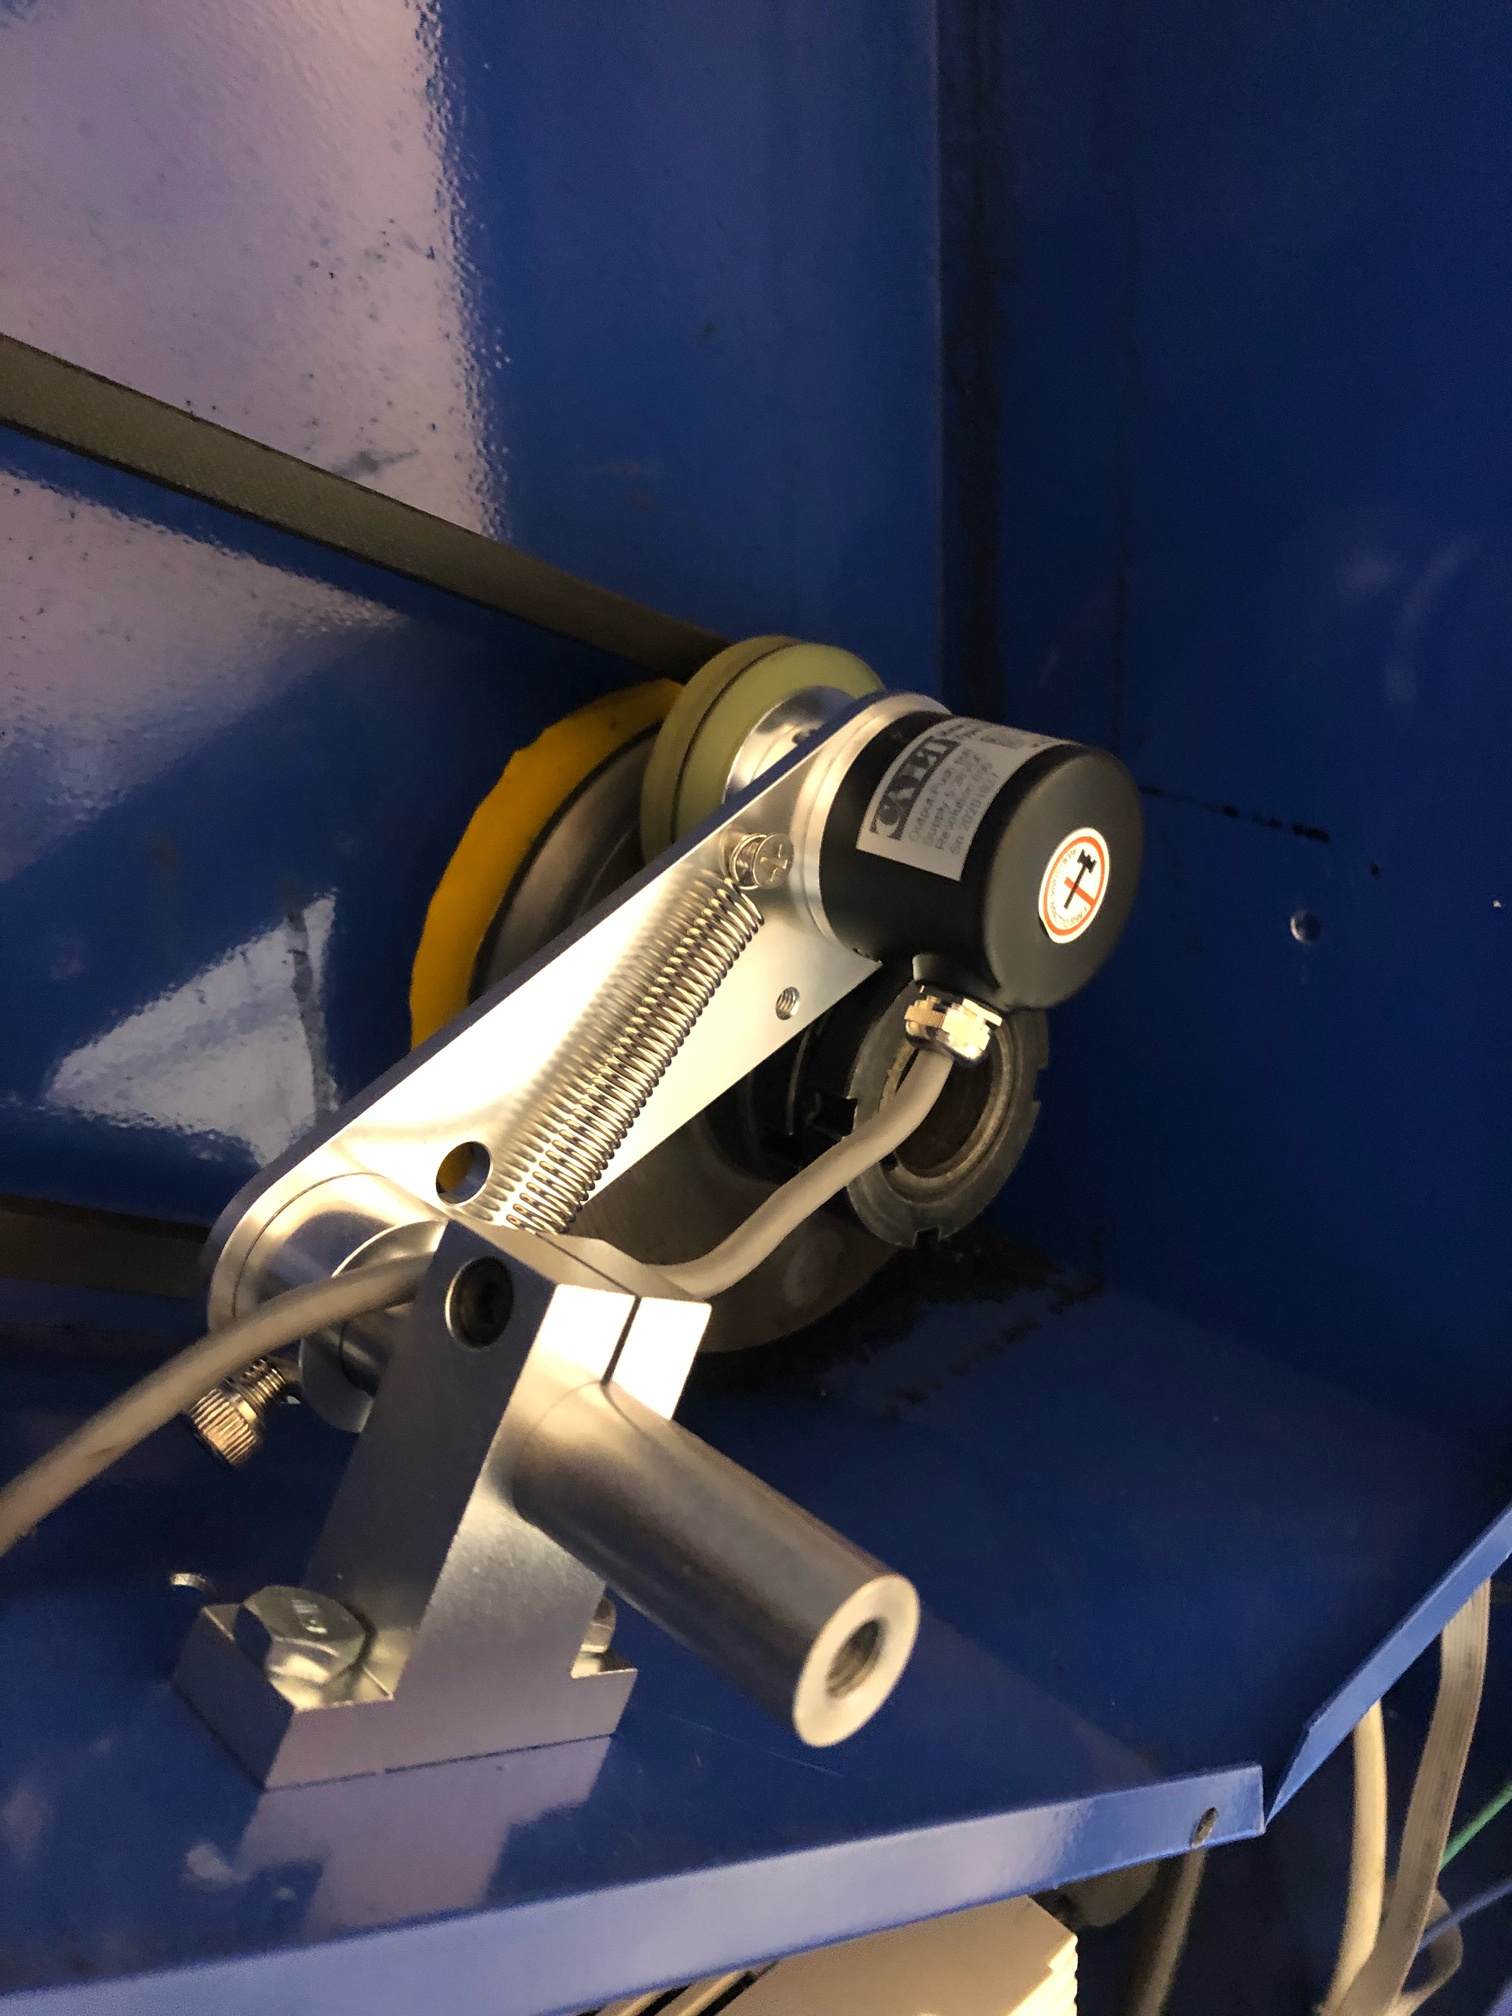
Now using LinuxCNC with an encoder what kind of trouble have I created using an encoder that is spinning off the lathe shaft relying on no slipping and perfect timing.

Please Log in or Create an account to join the conversation.
More
5 years 7 months ago #204249 by andypugh

rdeeming wrote: Now using LinuxCNC with an encoder what kind of trouble have I created using an encoder that is spinning off the lathe shaft relying on no slipping and perfect timing.


You might have been better off keeping the single pulse, LinuxCNC can work with that (about as well as Mach, ie not very)

Your current arrangement would probably work if you used an index pulse from the spindle rather than from the encoder.

But best would be to swap the friction-wheel for a toothed-belt.
(This might be a good application for a 3-d printed toothed belt)

Is there a spacer on the end of the spindle that could be replaced by a timing pulley?

Here is one I made earlier

Please Log in or Create an account to join the conversation.

More
5 years 7 months ago - 5 years 7 months ago #204257 by rdeeming
I'd like to keep the back part of the lathe shaft open to turn long stock and not have to cut it all the time.

To do that I need to find a pulley for the shaft that is ~2.25" in diameter. Then I can cut it like you did there and sleeve the lock rings that are on the end of the shaft.

So far google is not digging up pulleys that large with something like an 8mm belt.

I'll keep looking around.
Last edit: 5 years 7 months ago by rdeeming.

Please Log in or Create an account to join the conversation.

More
5 years 7 months ago #204335 by andypugh
www.bearingboys.co.uk/3M-Section-Timing-...iming-Pulley-21189-p

Might be a bit tight on material under the teeth.

But this 5mm one is pretty comfortable.
www.bearingboys.co.uk/5M-Section-Timing-...iming-Pulley-21224-p

I made my own , as I have the right gear hob for T5 belt.
The following user(s) said Thank You: rdeeming

Please Log in or Create an account to join the conversation.

Time to create page: 0.145 seconds
Powered by Kunena Forum
