

- Posts: 648
- Thank you received: 267
Gildemeister NEF 480 Retrofit
5 years 3 months ago - 5 years 3 months ago #214315
by anfänger
Replied by anfänger on topic Gildemeister NEF 480 Retrofit
Thanks spindle and gears are working now
Now it’s time to tune everything and take the first cut.
Now it’s time to tune everything and take the first cut.
Last edit: 5 years 3 months ago by anfänger.
Please Log in or Create an account to join the conversation.
5 years 3 months ago - 5 years 3 months ago #214688
by anfänger
Replied by anfänger on topic Gildemeister NEF 480 Retrofit
Added some new features for the gearchange yesterday, but the rain kept me from testing it.
Now I have buttons for each gear / spindle speed range.
When presse a custom MCode is executed, which stops the spindle and brings up a dialogue with the leaver positions.
Then sets the right clutch und spindle speed.
I think this will come in useful.
But what should be a quick session took me a lot longer than planned as always with me when I try to code I don‘t do it regularly and forget quite quick.
What is still missing is too write spindle speed and gear to a persistent parameter and reload it when powered on again.
Is there a best practice which parameters to use?
Next is to find a way to implement this in the post processor
OK and testing I hope I find the time for testing this evening
Thanks for reading
Patrick
Now I have buttons for each gear / spindle speed range.
When presse a custom MCode is executed, which stops the spindle and brings up a dialogue with the leaver positions.
Then sets the right clutch und spindle speed.
I think this will come in useful.
But what should be a quick session took me a lot longer than planned as always with me when I try to code I don‘t do it regularly and forget quite quick.
What is still missing is too write spindle speed and gear to a persistent parameter and reload it when powered on again.
Is there a best practice which parameters to use?
Next is to find a way to implement this in the post processor
OK and testing I hope I find the time for testing this evening
Thanks for reading
Patrick
Last edit: 5 years 3 months ago by anfänger.
Please Log in or Create an account to join the conversation.
5 years 3 months ago #214774
by anfänger
made sone progress on the gearbox change today.
Three problem I've got.
First the the spindle sounds like it needs new bearings,
second the parameter #<_spindle_on> os 0 even when the spindle is running, so the spindle doesn't restart after gear change
third the MCode to load the stored gear (M245) doesn't work when I put it in the startup codes. then linuxcnc errors our with M144 unknown.
M144 is a bash script and nit mapped in the INI.
When I run it in MDI later it works fine M144 is the script which brings the popup window wit the gear settings.
Thaks Patrick
Replied by anfänger on topic Gildemeister NEF 480 Retrofit
made sone progress on the gearbox change today.
Three problem I've got.
First the the spindle sounds like it needs new bearings,
second the parameter #<_spindle_on> os 0 even when the spindle is running, so the spindle doesn't restart after gear change
third the MCode to load the stored gear (M245) doesn't work when I put it in the startup codes. then linuxcnc errors our with M144 unknown.
M144 is a bash script and nit mapped in the INI.
When I run it in MDI later it works fine M144 is the script which brings the popup window wit the gear settings.
Thaks Patrick
Please Log in or Create an account to join the conversation.
5 years 3 months ago #214992
by anfänger
Replied by anfänger on topic Gildemeister NEF 480 Retrofit
Fixed the spindle start by reading the hal pins. Now it works, But I didn’t make a video.
What I did film was the successful homing:
Then I removed Chuck and the mechanical clamping device.
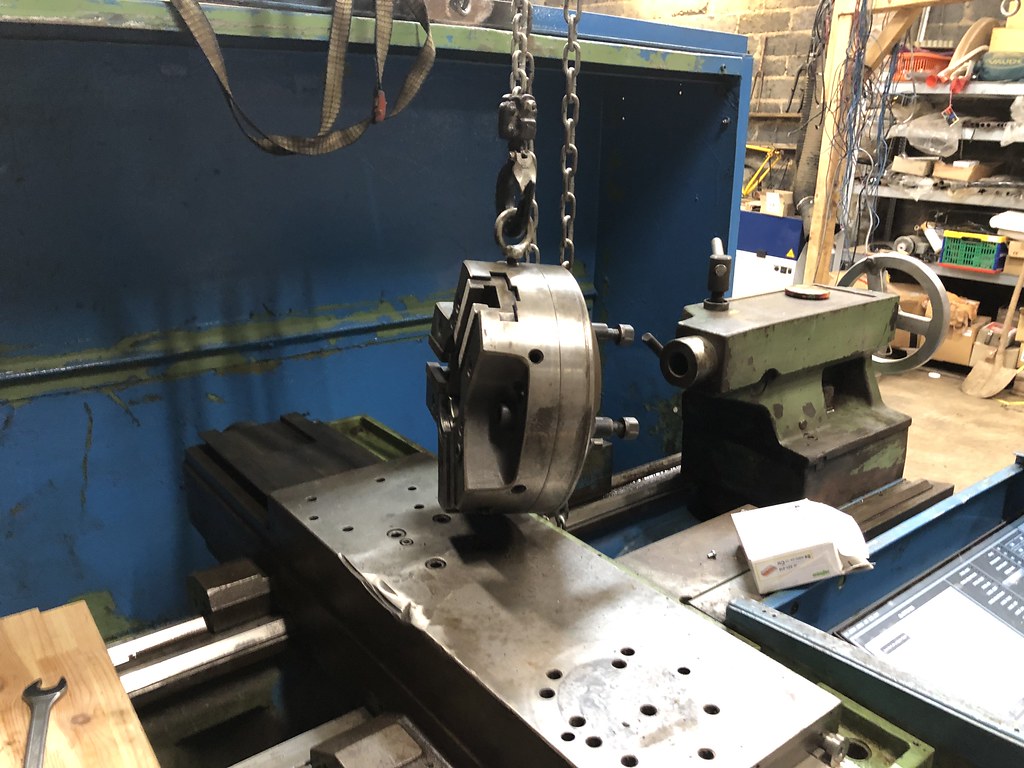
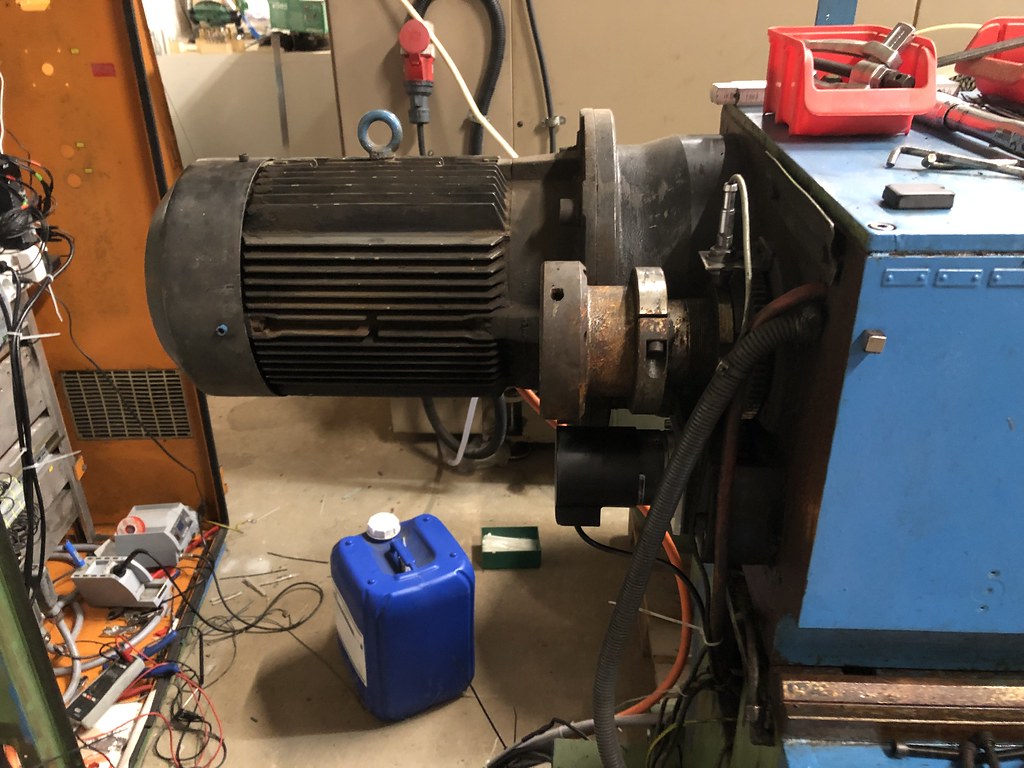

I will clean the spindle and then start to prepare for mounting a normal chuck.
The Schunk Cuck and the clamping thing will get a a cleaning and the n will be stored till I have a need for it.
What I did film was the successful homing:
Then I removed Chuck and the mechanical clamping device.
I will clean the spindle and then start to prepare for mounting a normal chuck.
The Schunk Cuck and the clamping thing will get a a cleaning and the n will be stored till I have a need for it.
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- tommylight
-

- Away
- Moderator
-

5 years 3 months ago #215026
by tommylight
Replied by tommylight on topic Gildemeister NEF 480 Retrofit
I wonder if that chuck would fit my Mazak Micro Slant 15 ???

Please Log in or Create an account to join the conversation.
5 years 3 months ago - 5 years 3 months ago #215028
by anfänger
Replied by anfänger on topic Gildemeister NEF 480 Retrofit
What kind of Spindle Node do you have? And where her you from?
But I am not sure If I will sell it.
Now that I know how to mount it and if I make some tools mounting and dismounting won’t take that long.
It is a nice three jaw chuck and I have a lot of jaws for it.
But I font think I will ever need the automatic clamping it was fun to get it running and it nice for a Job shop but for me it is more or less useless, cause I don’t think I will make more thank three same parts in a row.
But I would would be really tempted trade it for a 250mm there jaw chuck with two piece jaws cable of 2250 rpm
But I am not sure If I will sell it.
Now that I know how to mount it and if I make some tools mounting and dismounting won’t take that long.
It is a nice three jaw chuck and I have a lot of jaws for it.
But I font think I will ever need the automatic clamping it was fun to get it running and it nice for a Job shop but for me it is more or less useless, cause I don’t think I will make more thank three same parts in a row.
But I would would be really tempted trade it for a 250mm there jaw chuck with two piece jaws cable of 2250 rpm
Last edit: 5 years 3 months ago by anfänger.
Please Log in or Create an account to join the conversation.
Time to create page: 0.691 seconds